Explore our primary spectrum of certified chemical auxiliaries, high-performance cosmetic base matrices, and natural extracts engineered for safety, bioavailability, and regulatory compliance.
In the contemporary global chemical, cosmetic, and food manufacturing sectors, coloring agents act as pivotal functional raw materials. With the regulatory frameworks across the European Economic Area (EEA) and global markets tightening, the acquisition of a CE Certification (Conformité Européenne) serves as a definitive yardstick for product safety, non-toxicity, and compliance. CE-certified coloring agents demonstrate adherence to strict directives regarding heavy metal thresholds, chemical stability, and biocompatibility, allowing multi-industry manufacturers to integrate these colorants without legal or health concerns.
Furthermore, shifting consumer preferences from synthetic azo-dyes to clean-label, bio-based alternatives have forced manufacturers to rethink extraction protocols. As regulatory authorities phase out traditional synthesized pigments due to systemic health implications, plant-derived colorants—such as Gardenia Yellow Extract—experience unprecedented global demand. Adapting to this trend requires high technical precision to stabilize natural color molecules under varying thermal, light, and pH environments.
Shaanxi Mirae Biology Co., Ltd. is a professional manufacturer and global supplier specializing in the research, development, production, and distribution of high-quality plant extracts, nutritional ingredients, cosmetic raw materials, peptides, and specialty chemicals.
Located in Shaanxi Province, China, a region renowned for its rich botanical resources and advanced biotechnology industry, we combine premium natural ingredients with modern extraction technology to provide innovative and reliable solutions for customers worldwide.
With a strong commitment to quality, innovation, and customer satisfaction, we serve clients across the pharmaceutical, nutraceutical, cosmetic, food, and research industries. Our experienced technical team and strict quality control system ensure that every product meets international standards for purity, safety, and consistency. Today, our products are exported to customers in North America, Europe, Southeast Asia, the Middle East, and many other international markets, earning a reputation for dependable quality and professional service.
Our GMP-compliant facility utilizes cutting-edge mechanical, physical, and chemical extraction methodologies. Each stage is meticulously monitored to prevent cross-contamination and thermal degradation of active pigments.
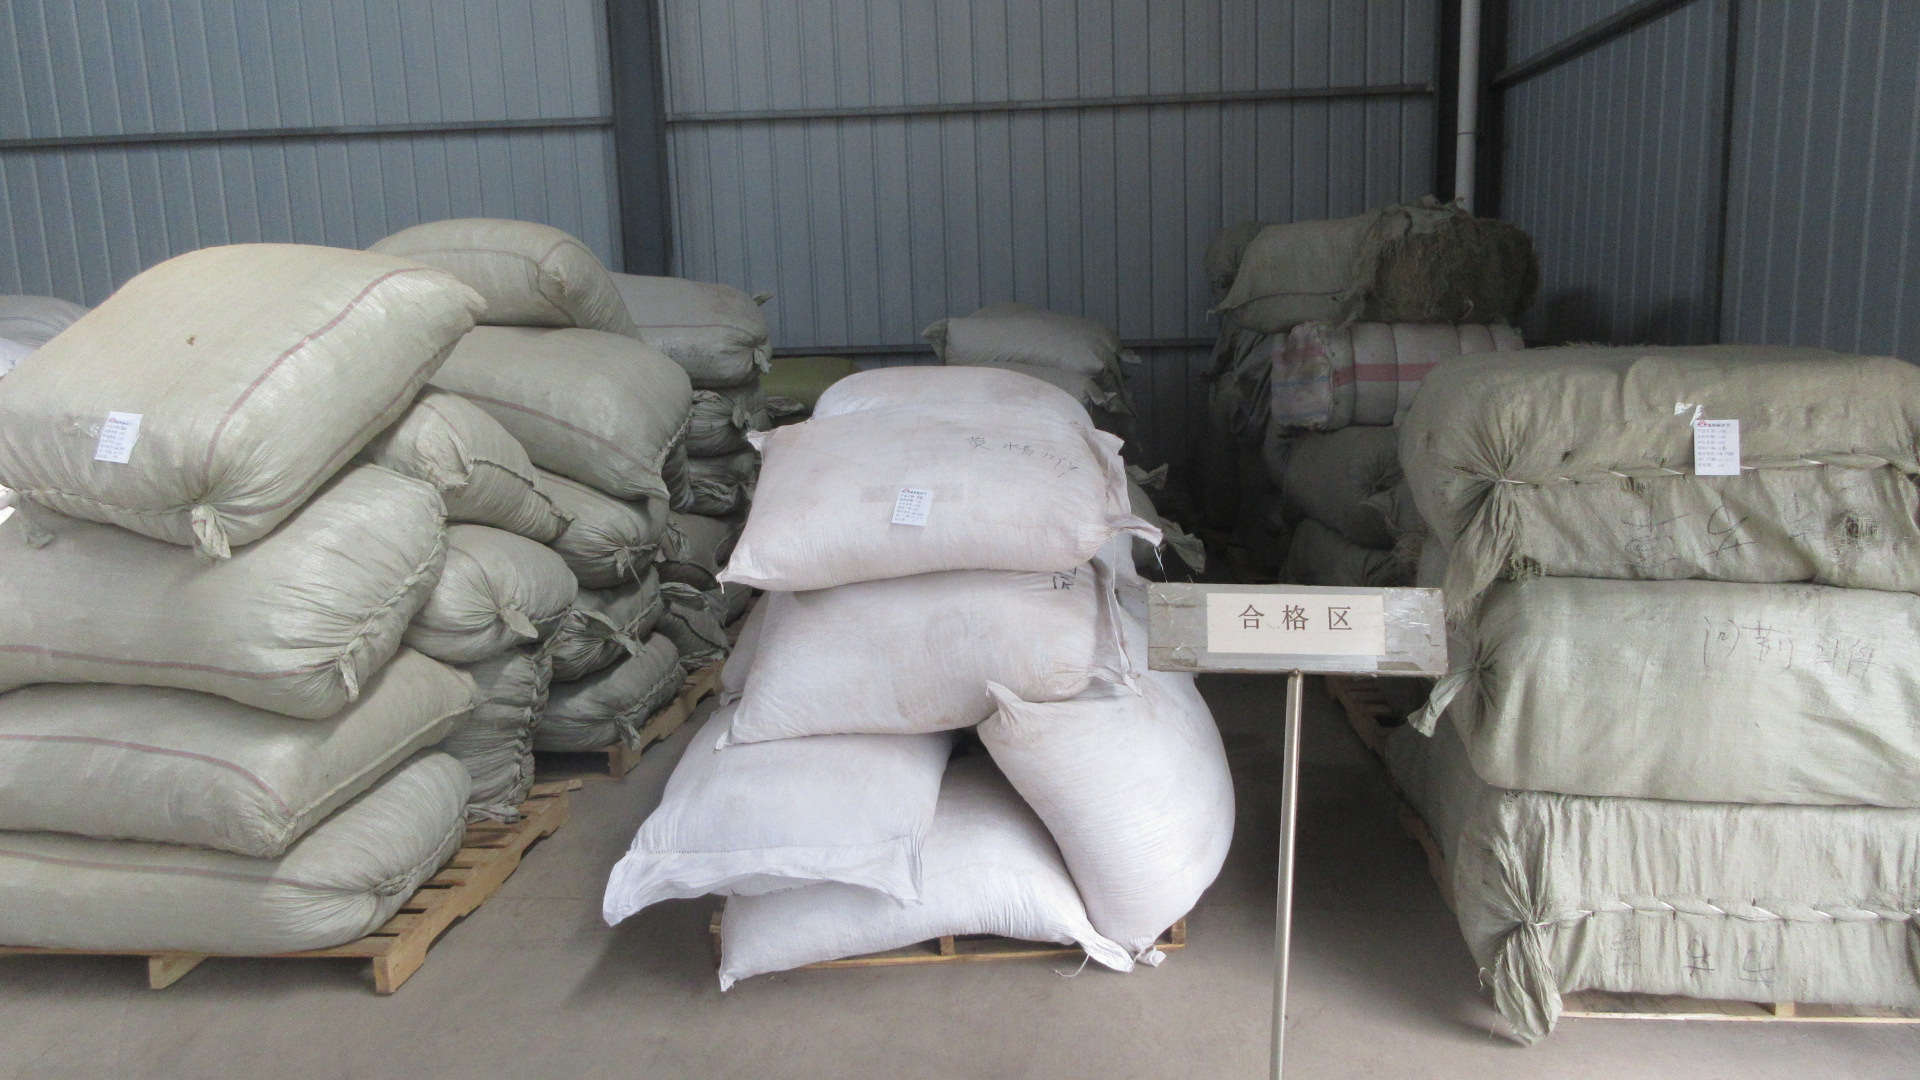
Sourcing and rigorous chromatographic validation of organic inputs.
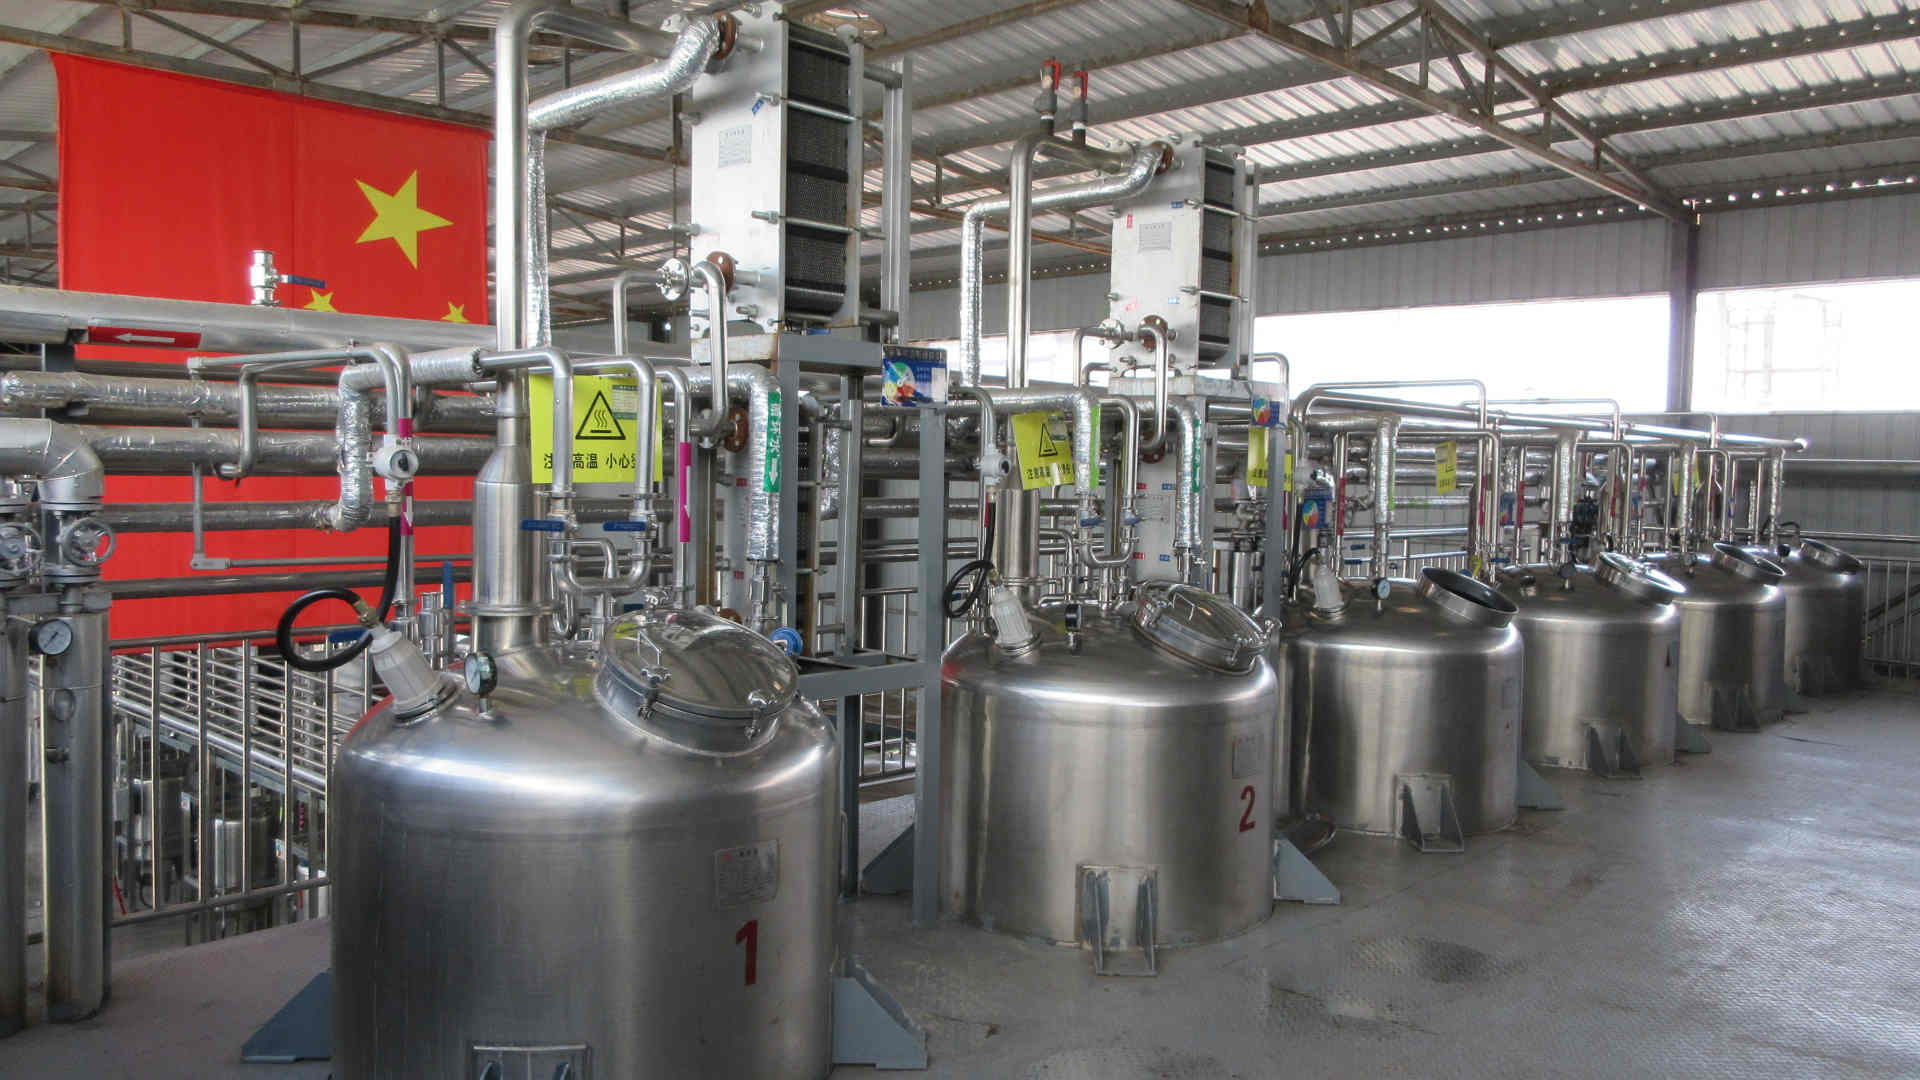
Supercritical fluid and low-heat solvent processing.
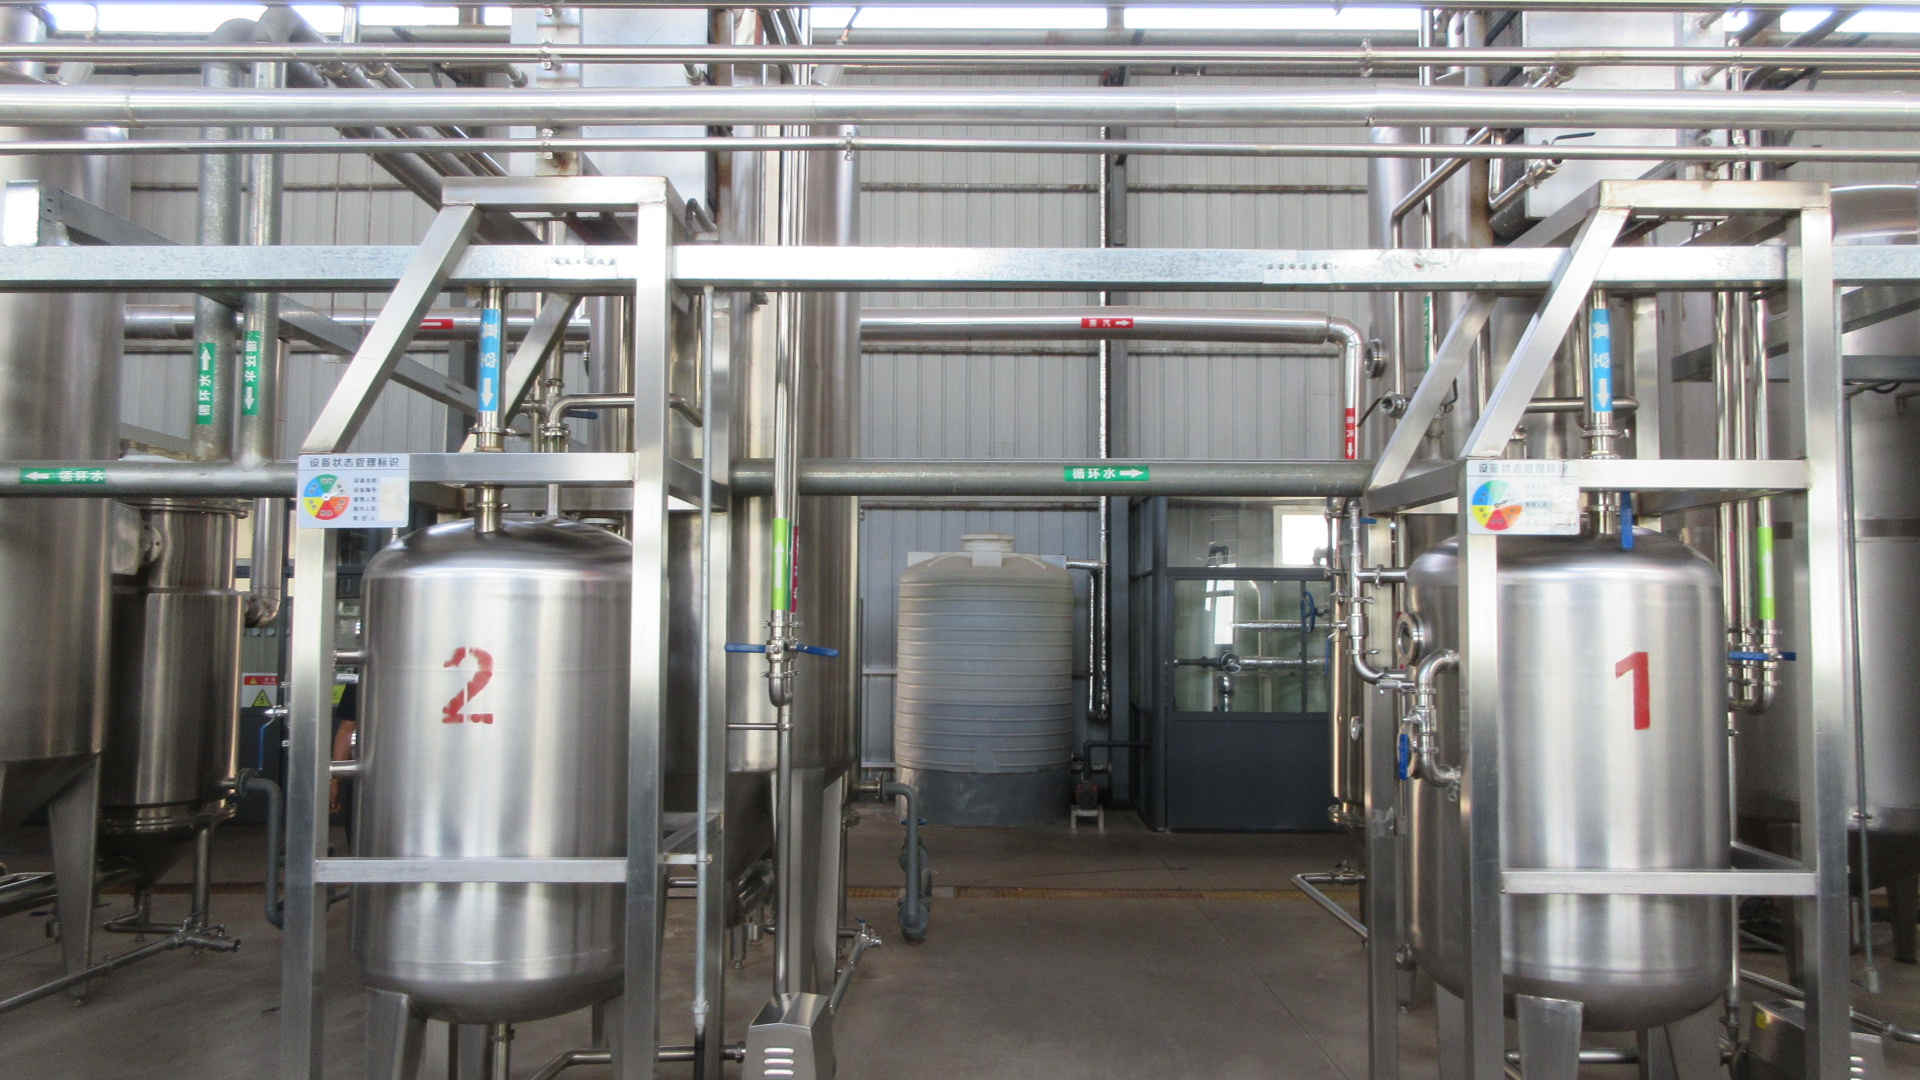
Vacuum-evaporation loops designed to conserve molecular structures.
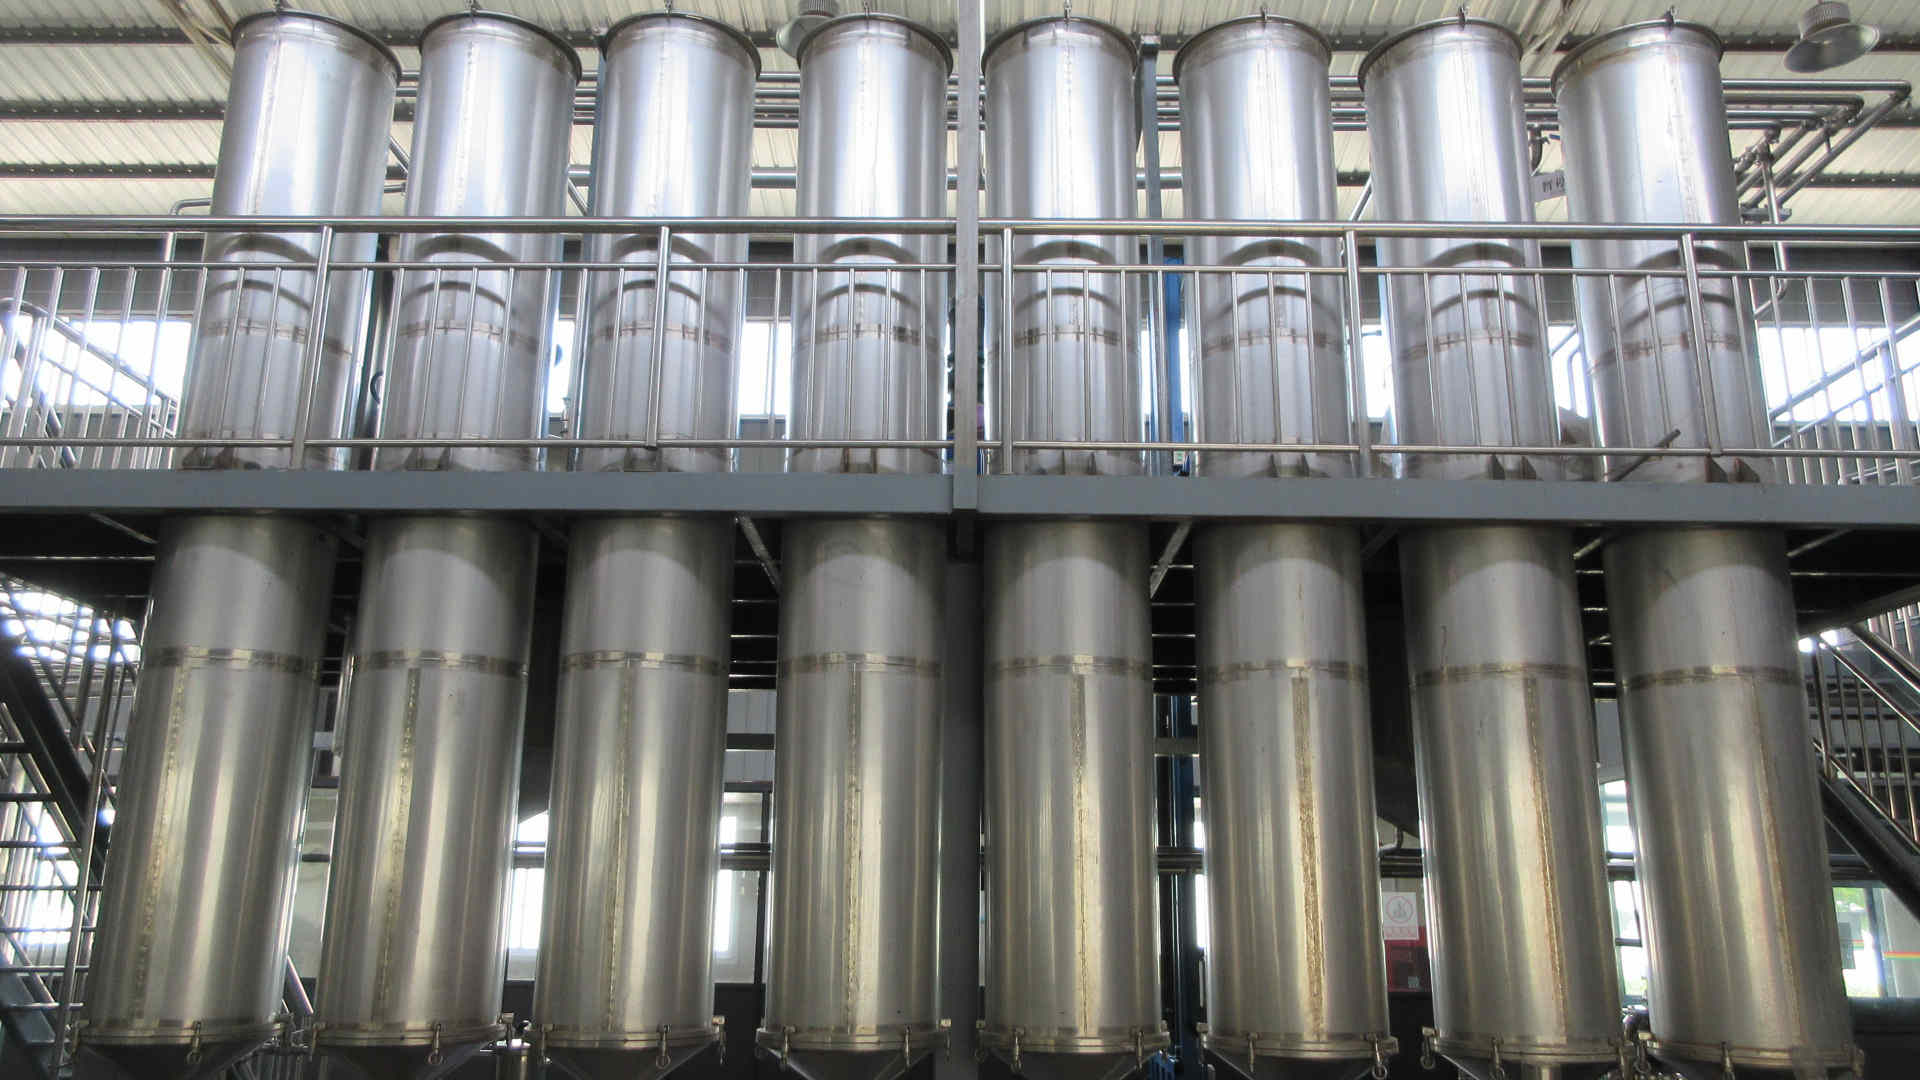
Macroporous resin chromatography targeting trace toxins.
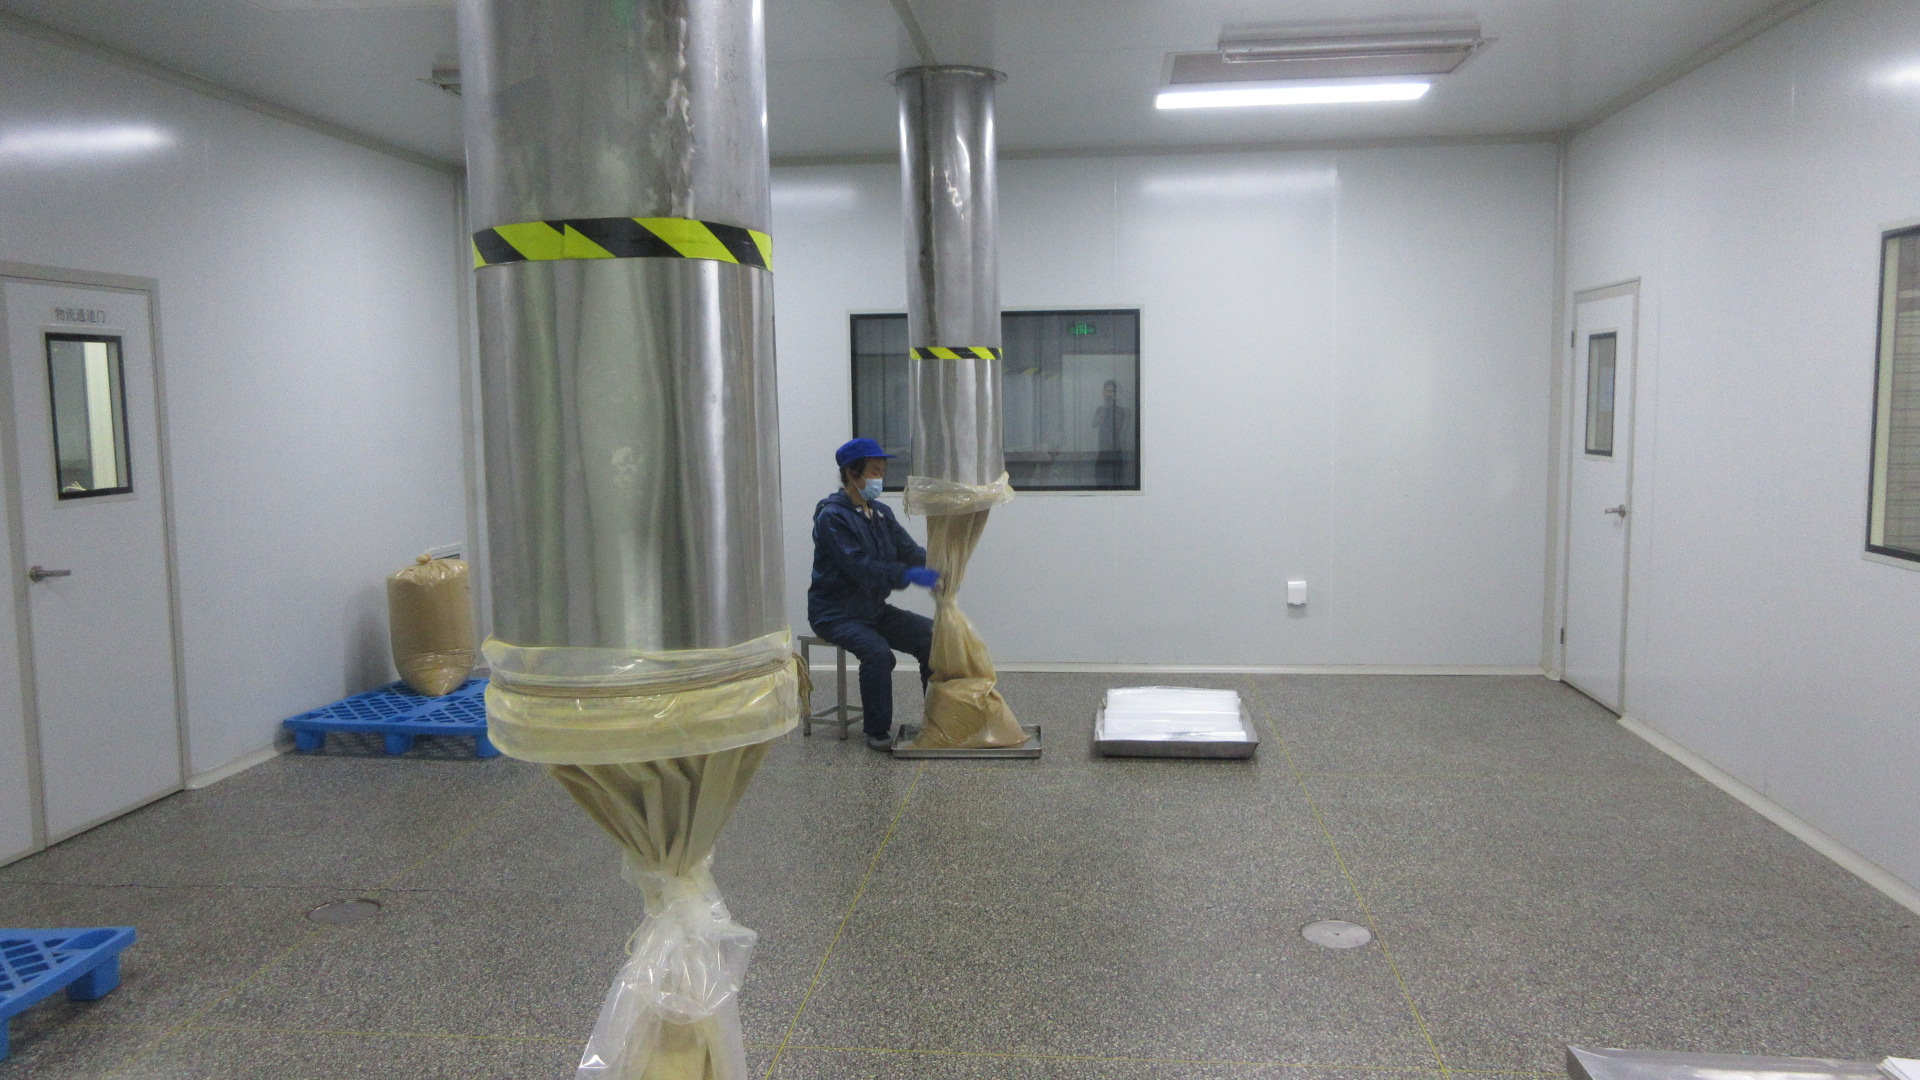
Converting liquid phase to stable powder format via atomization.
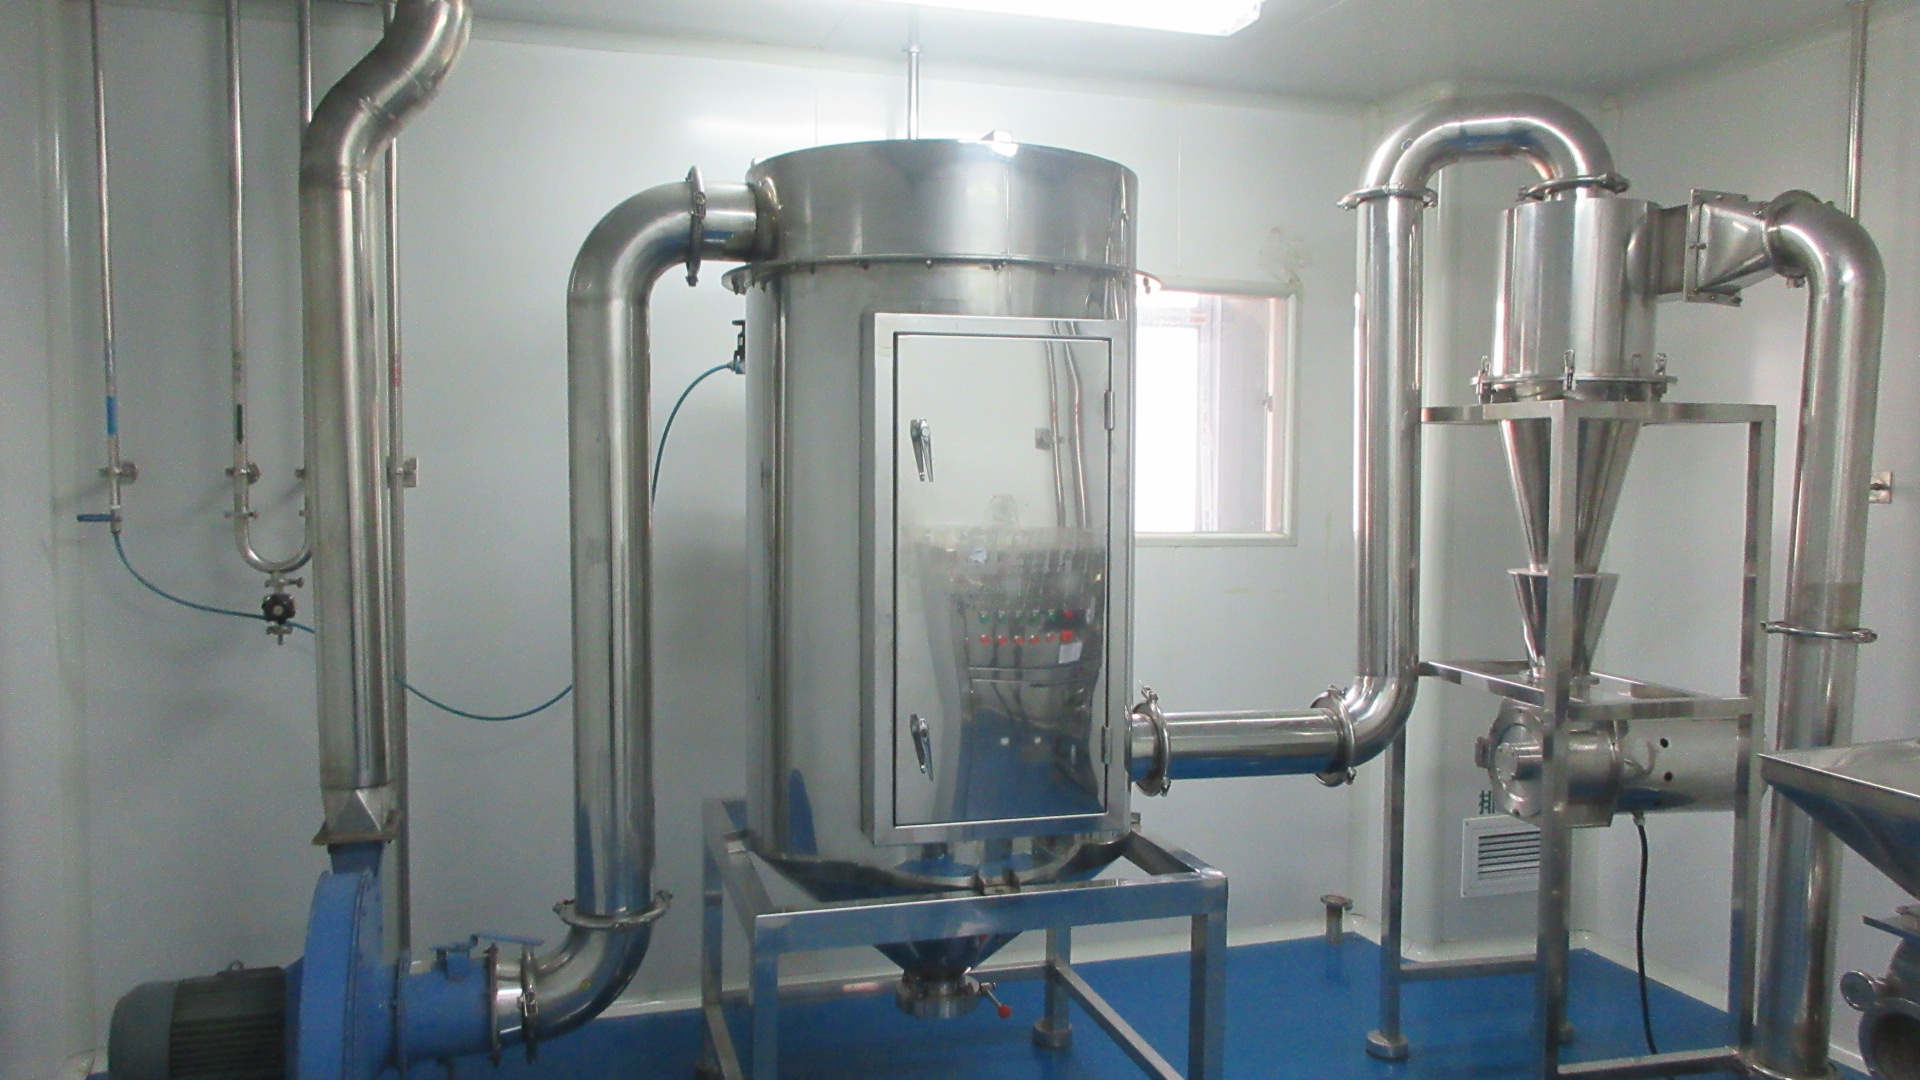
Refining particle distribution down to standardized micron scales.
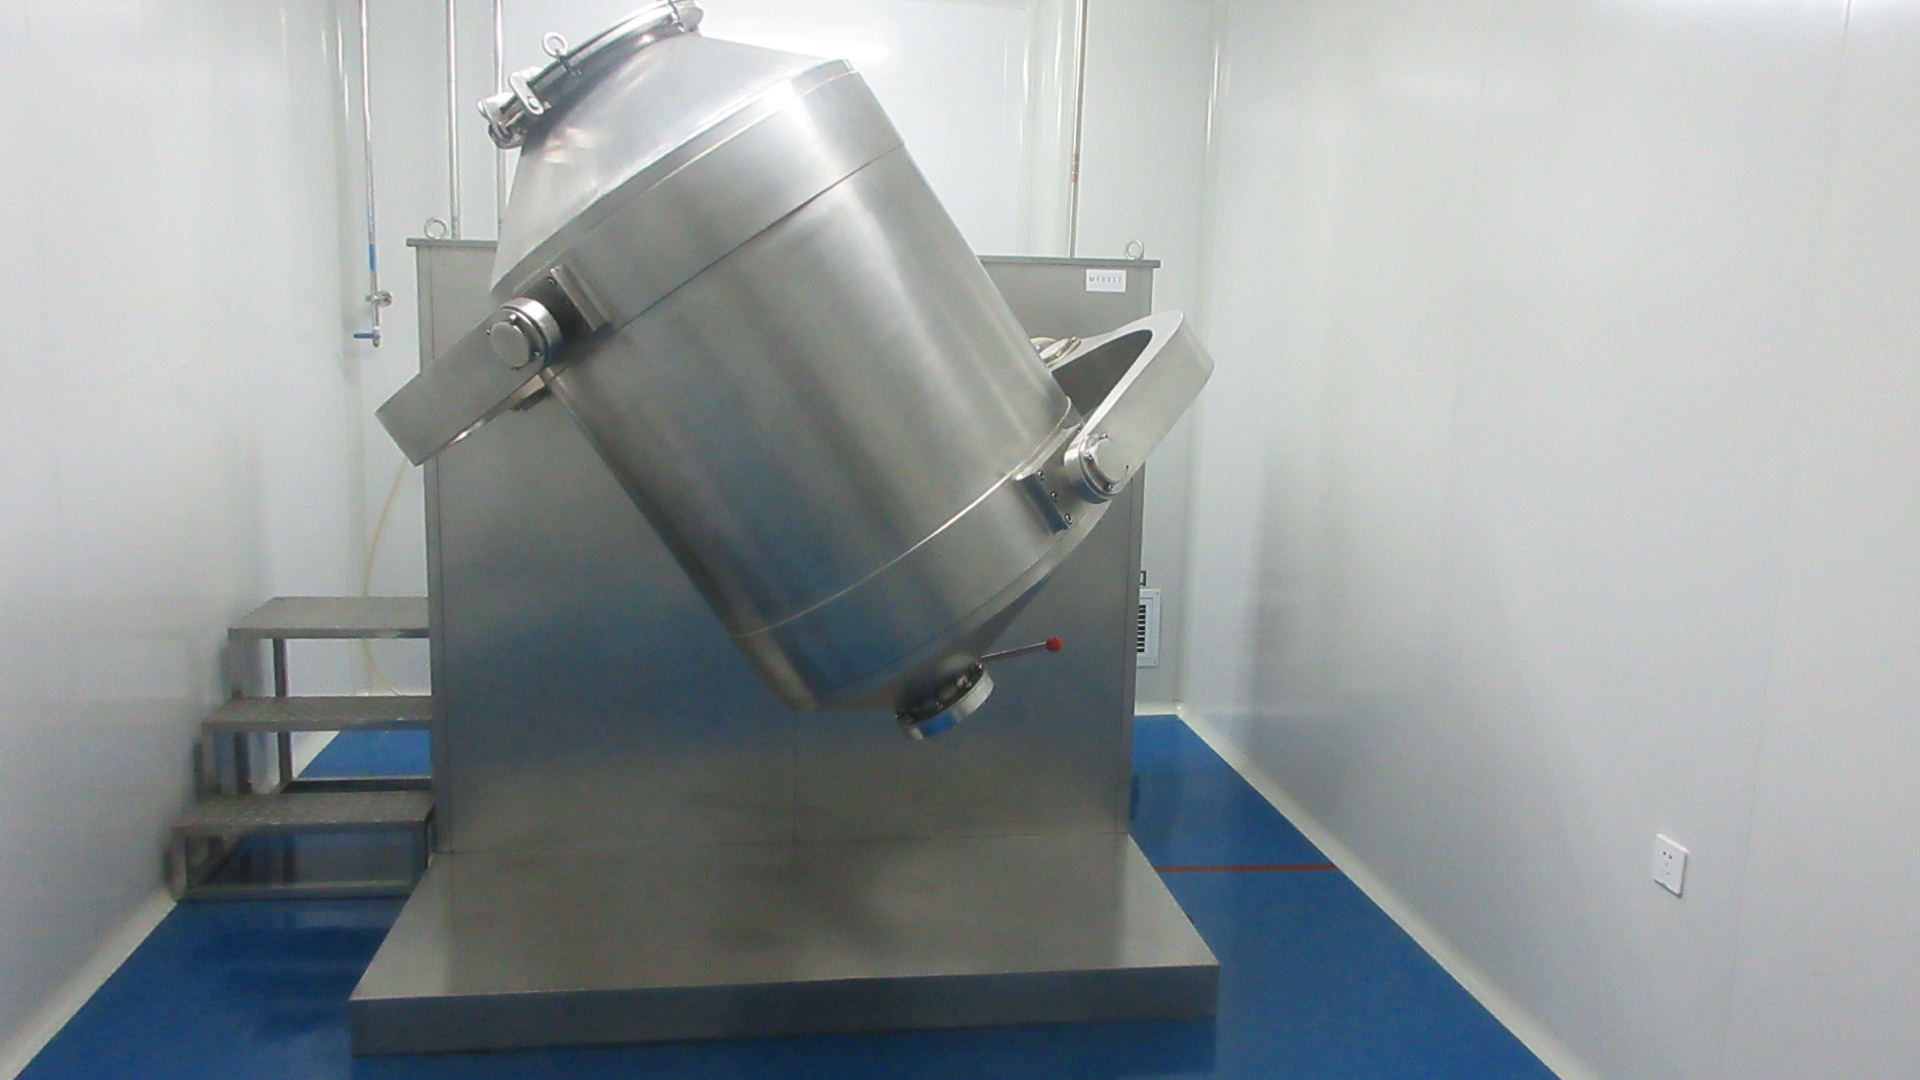
Homogenization of batches to guarantee consistent color intensity.
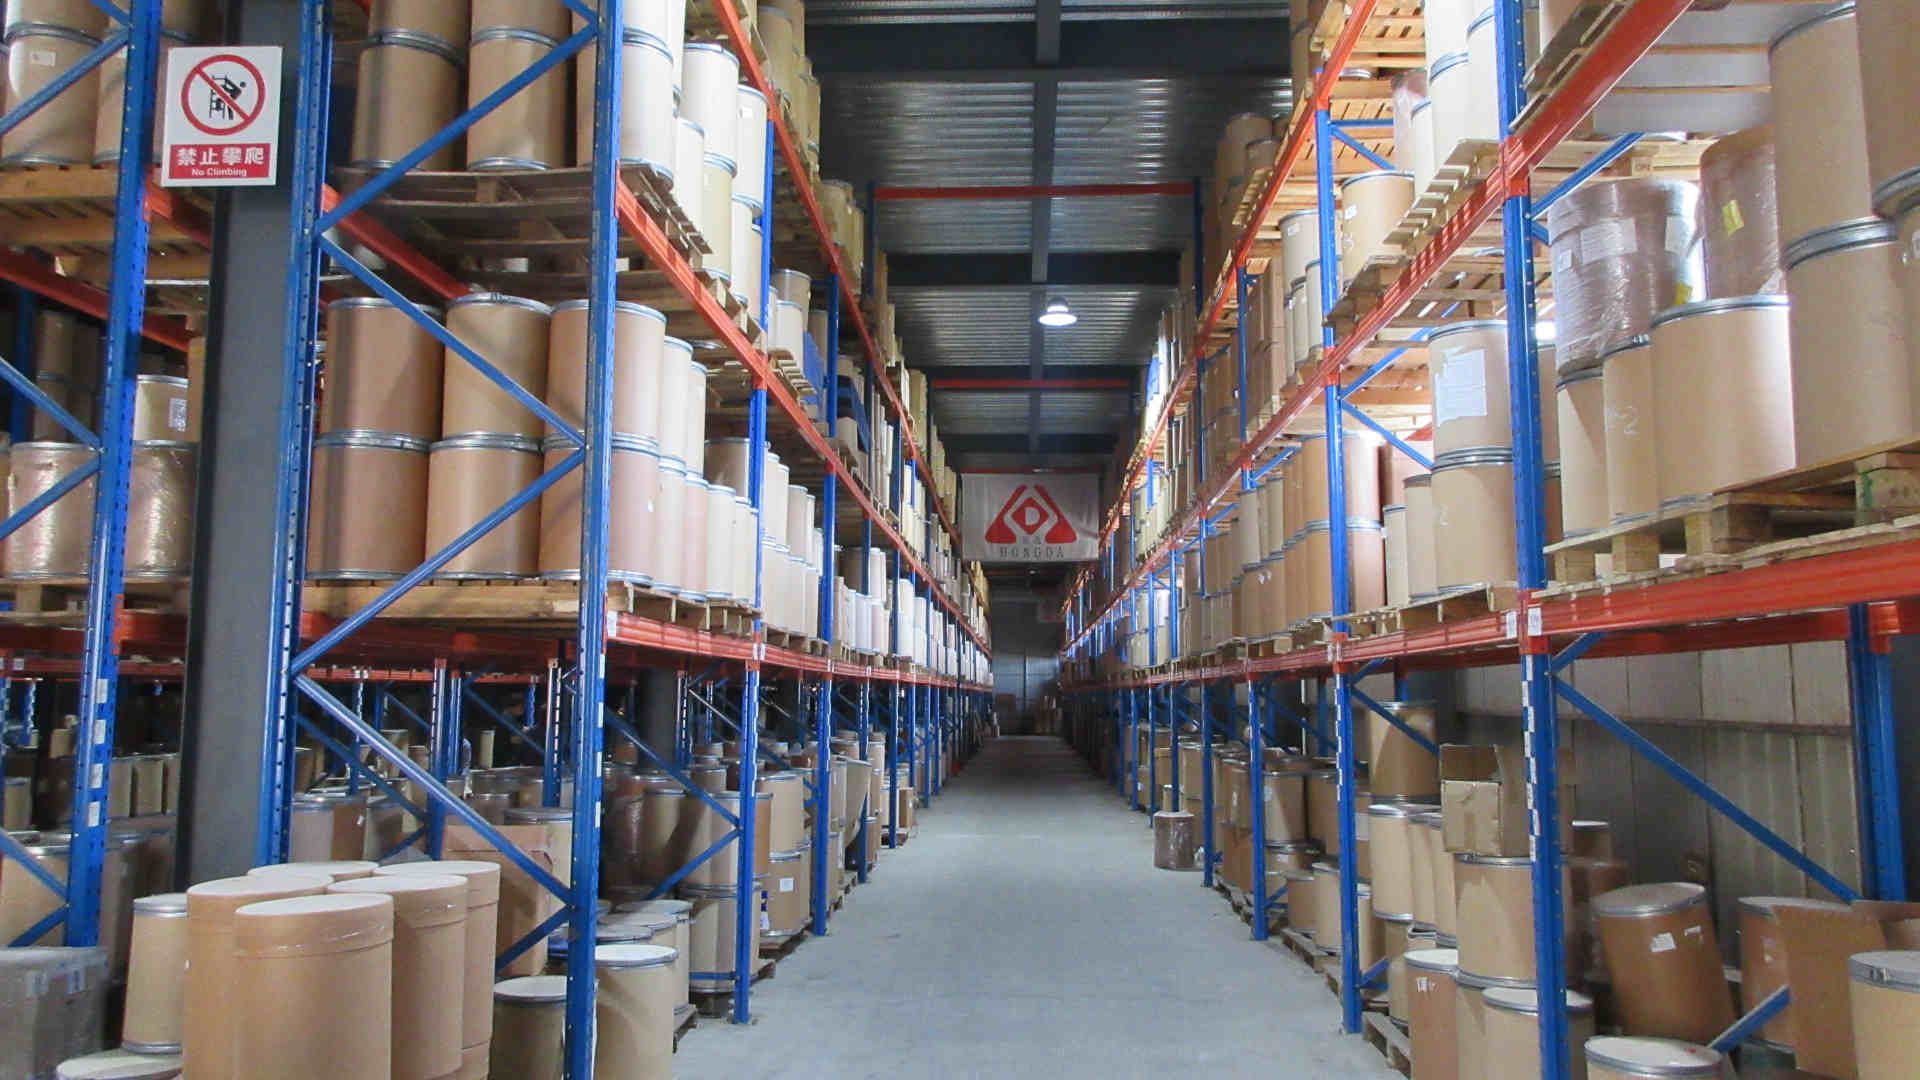
Secure, nitrogen-sealed packaging to protect against light and oxidation.
Our factories house large-scale bioreactors and processing machinery to meet massive supply chain needs. Automation ensures high precision, reduced contamination risk, and consistent batch quality.
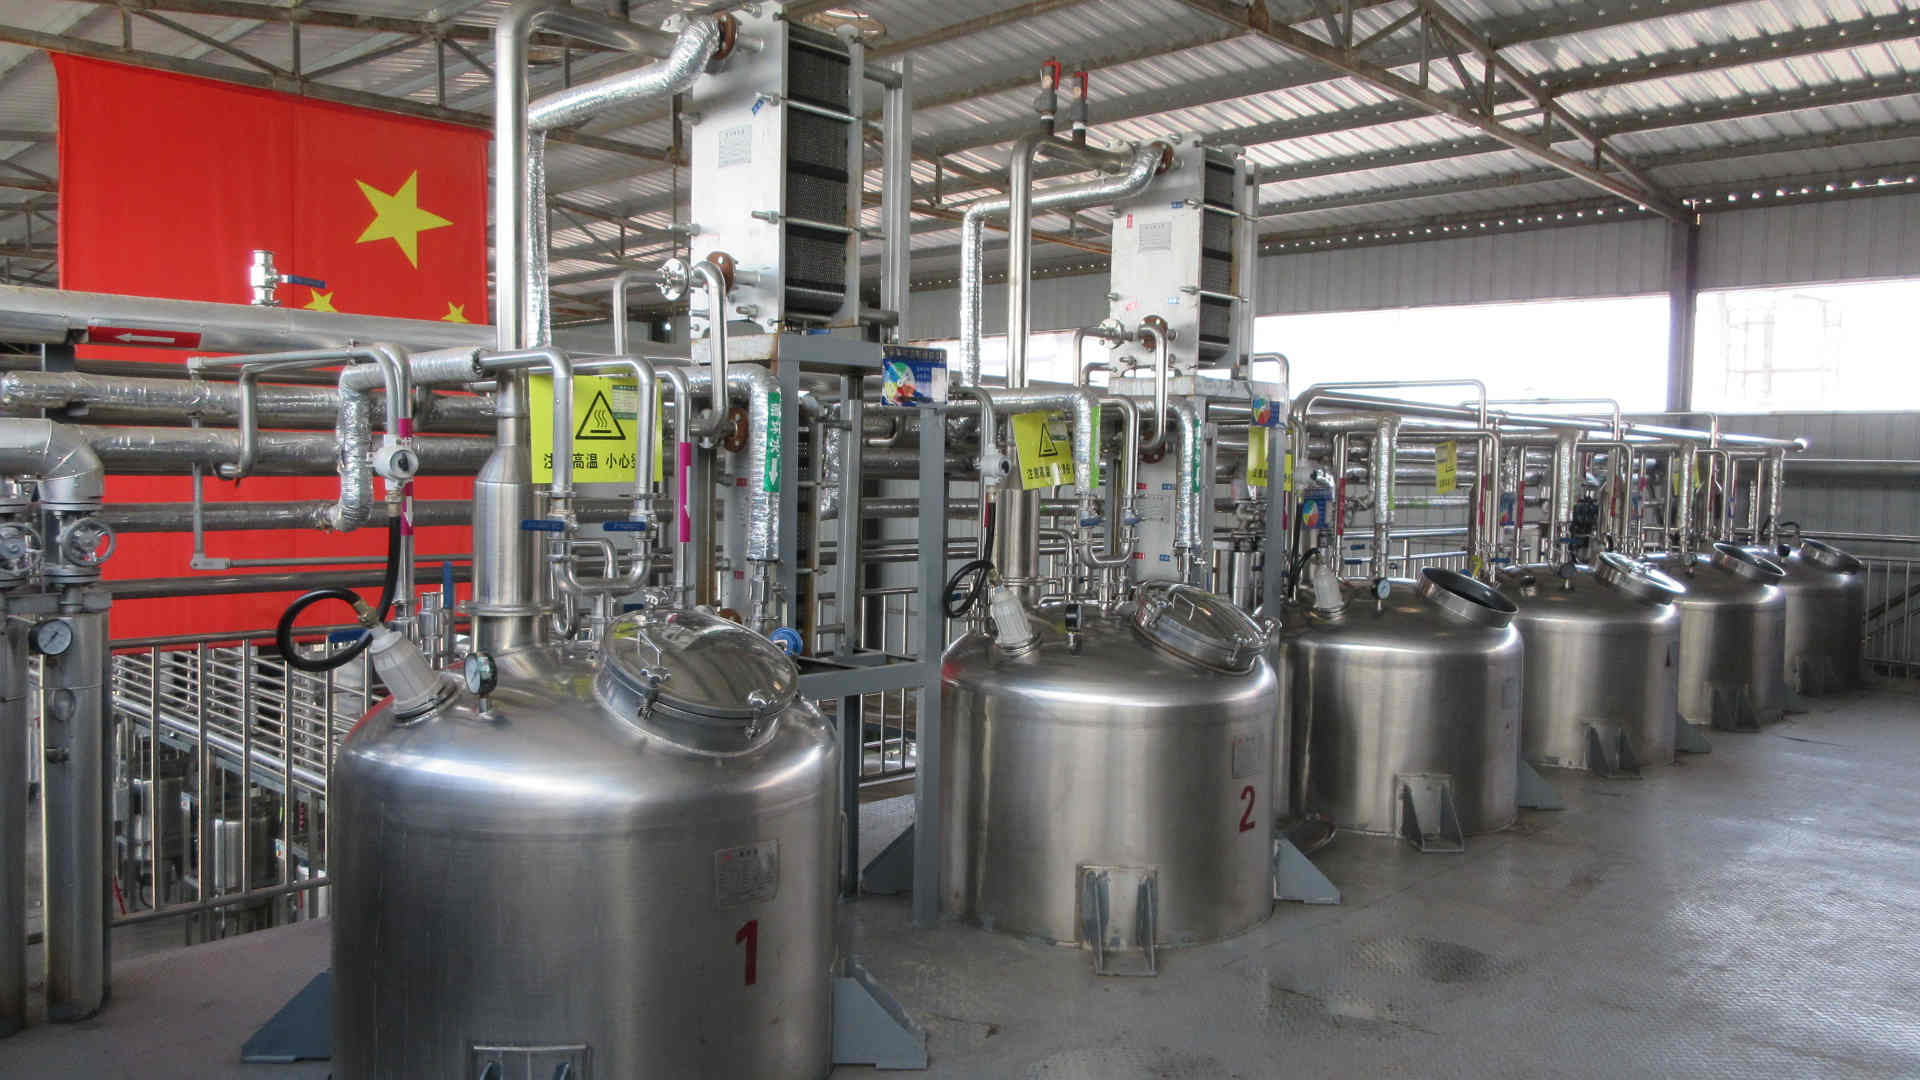
High-volume, temperature-controlled vessel optimized for primary extraction cycles.
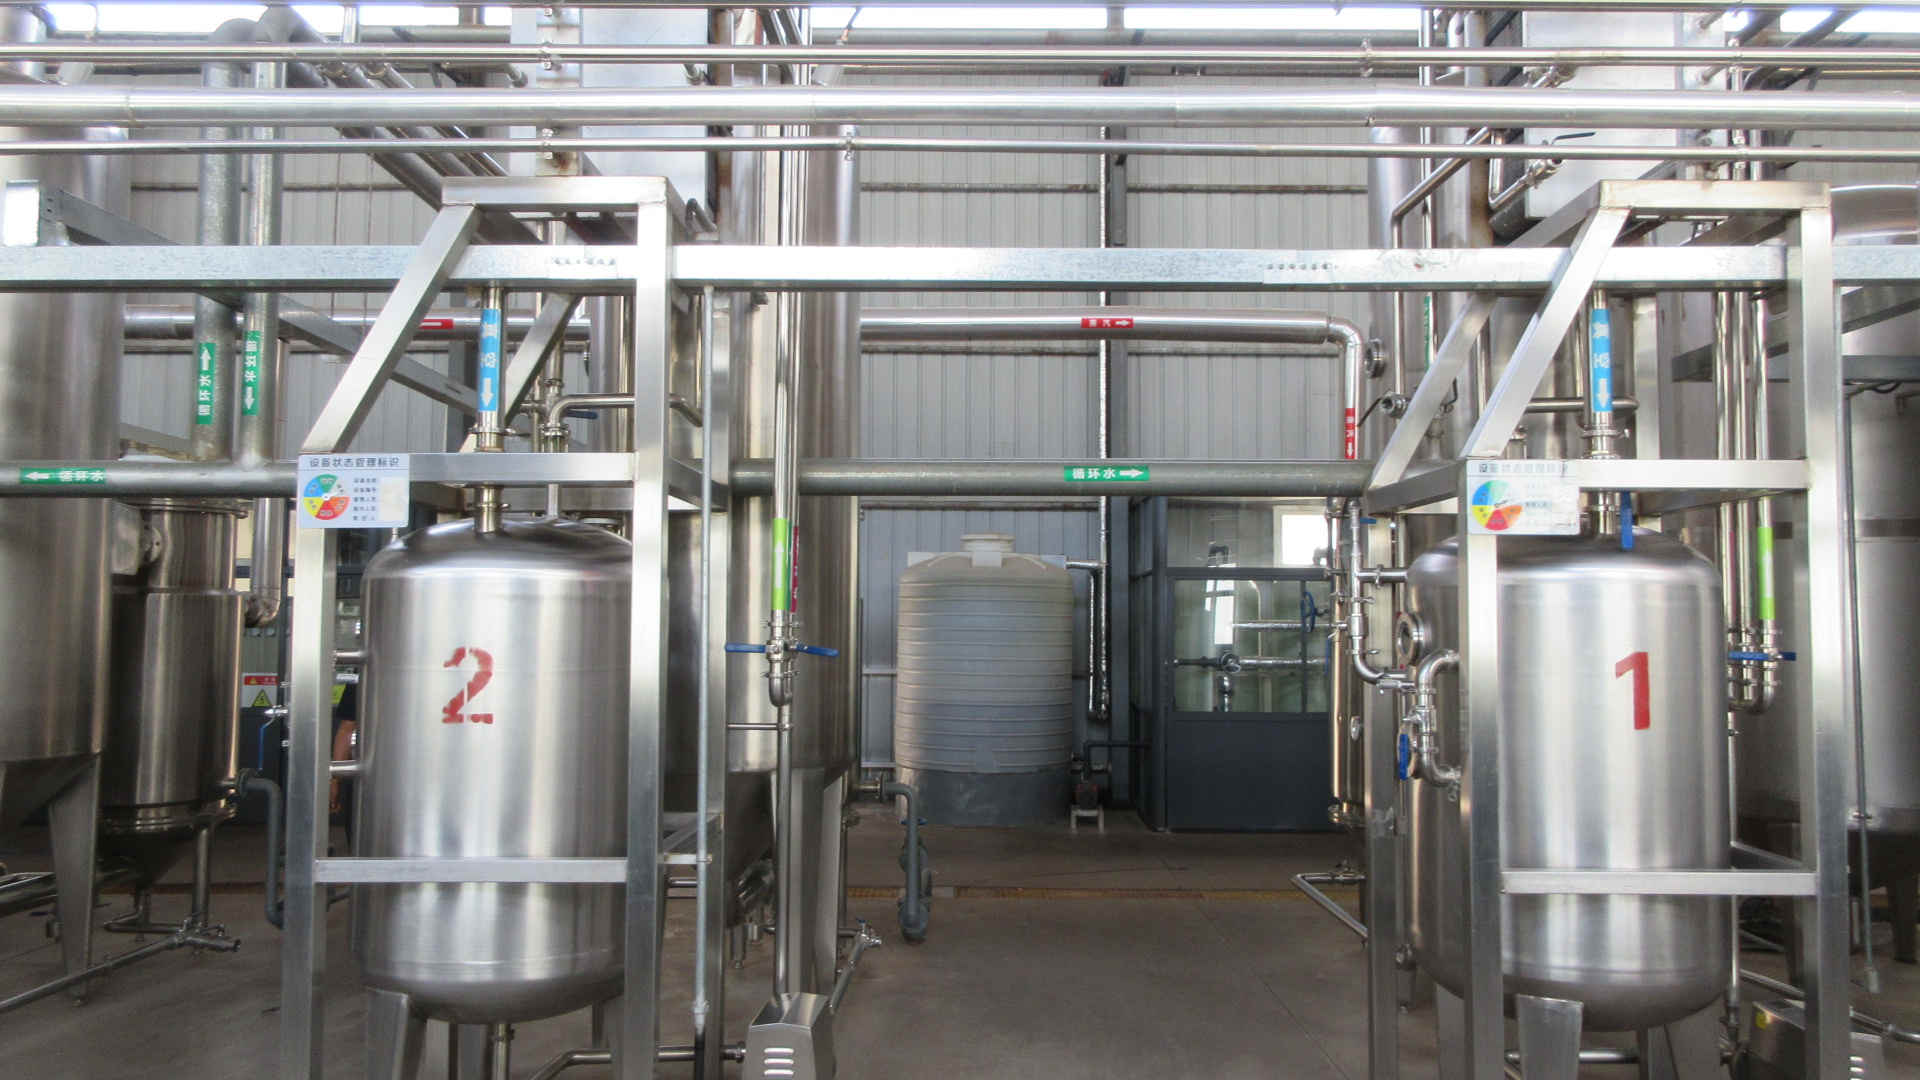
Falling-film evaporator for rapid, low-temperature liquid concentration.
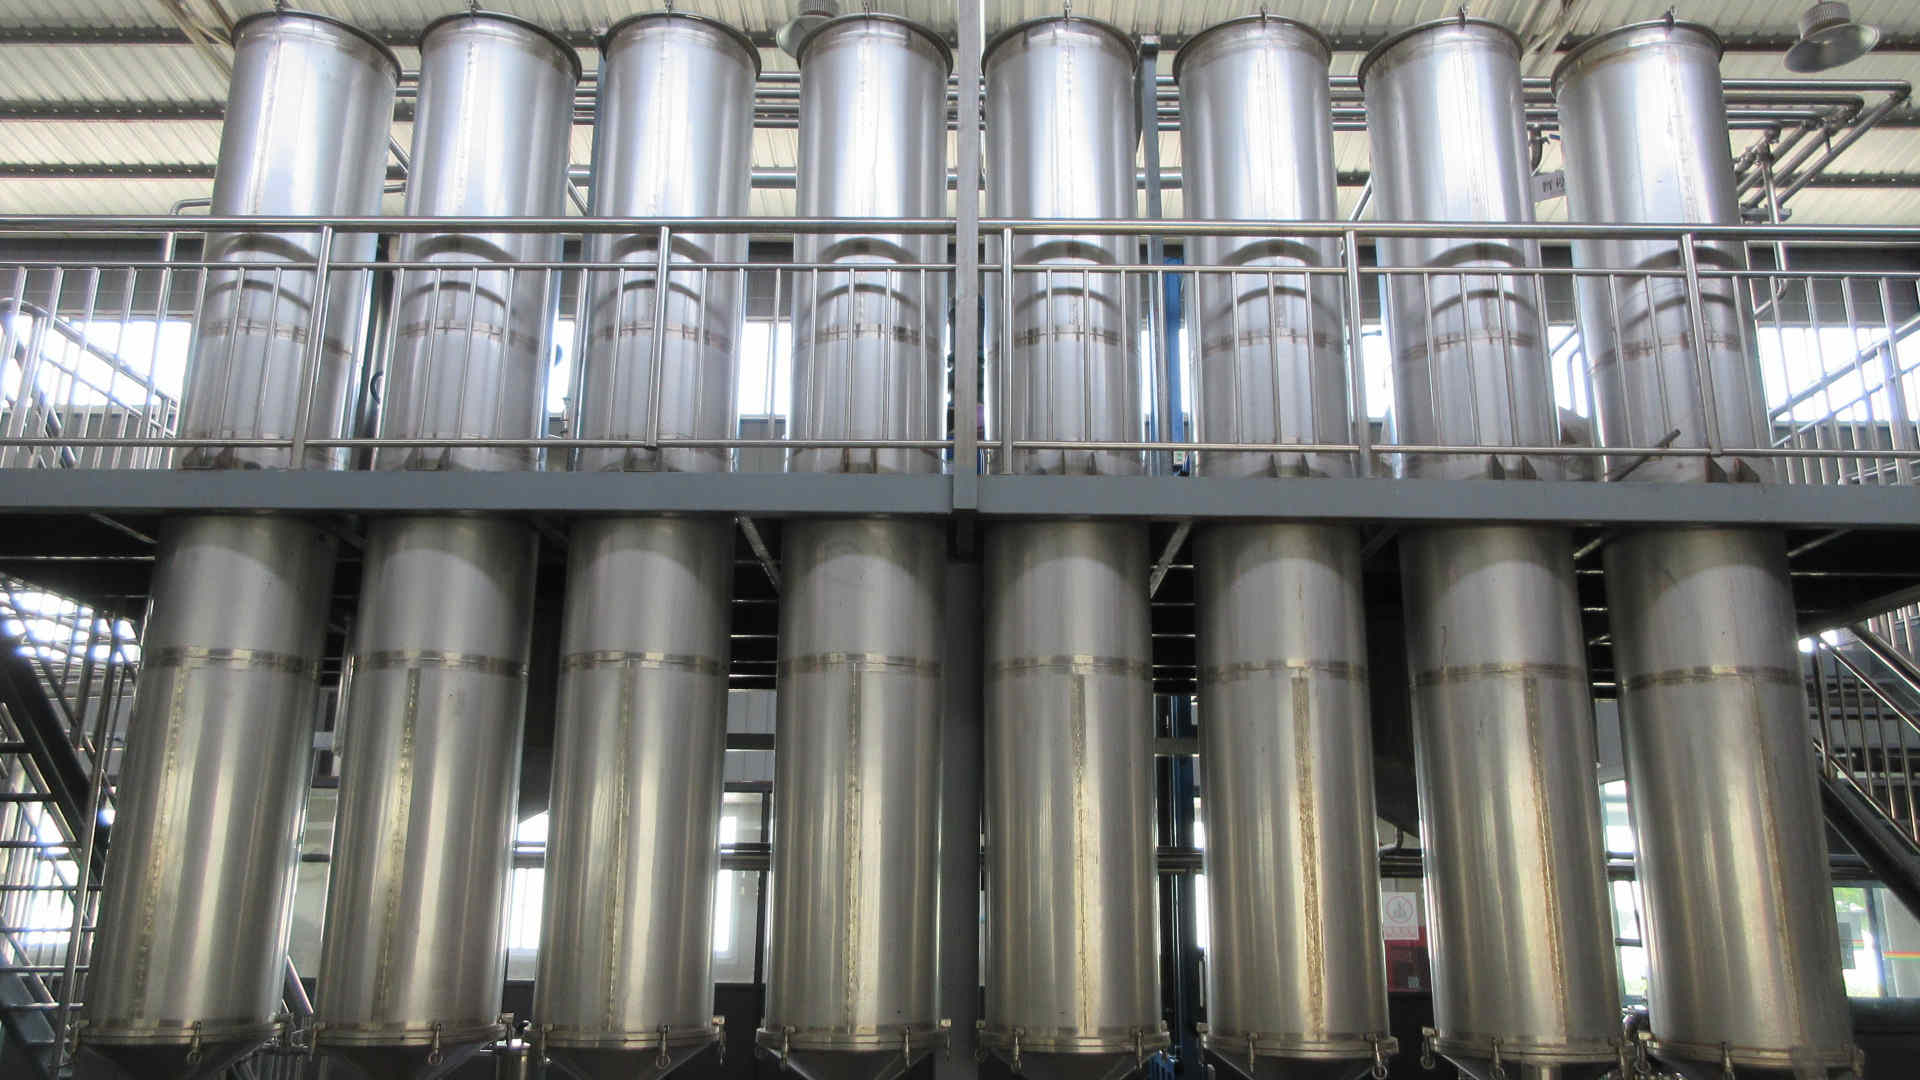
Columns packed with specialized resin matrices for pigment purification.
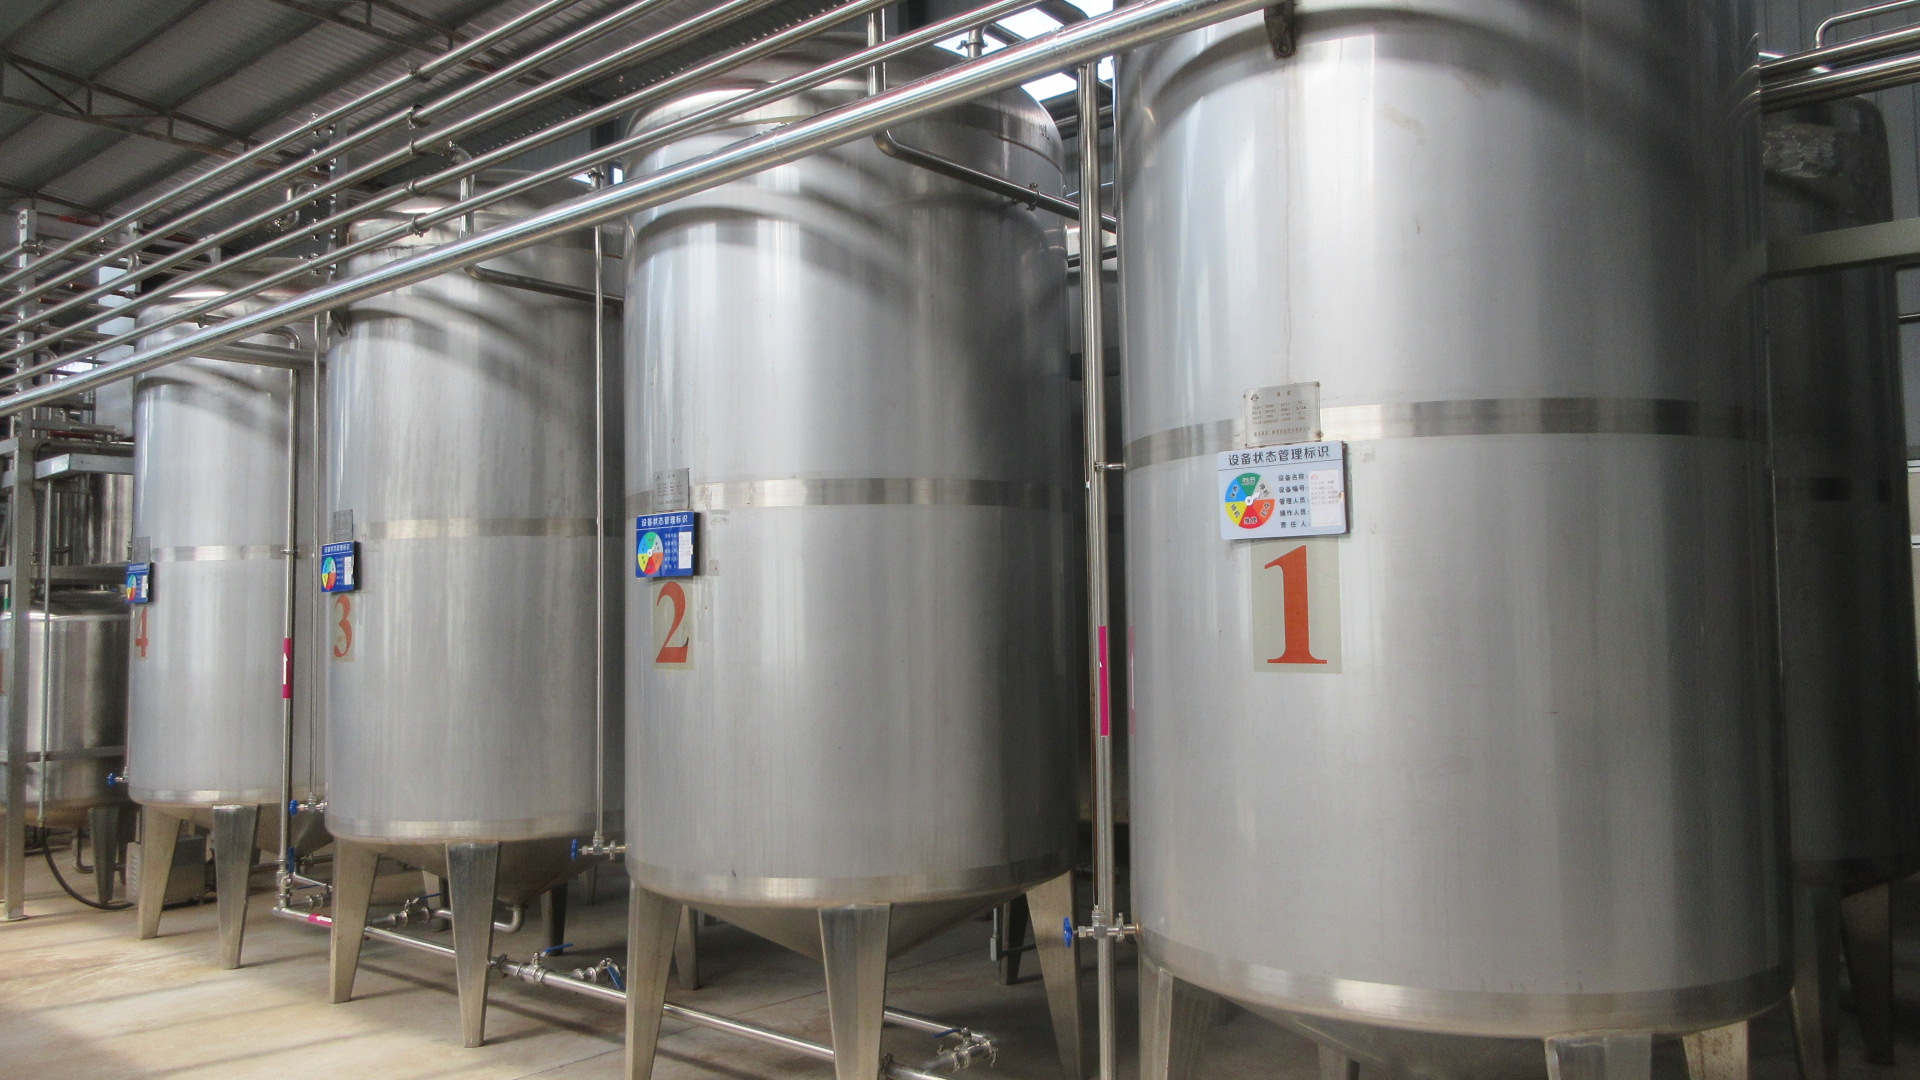
Hermetically sealed stainless steel tanks protecting refined raw liquids.
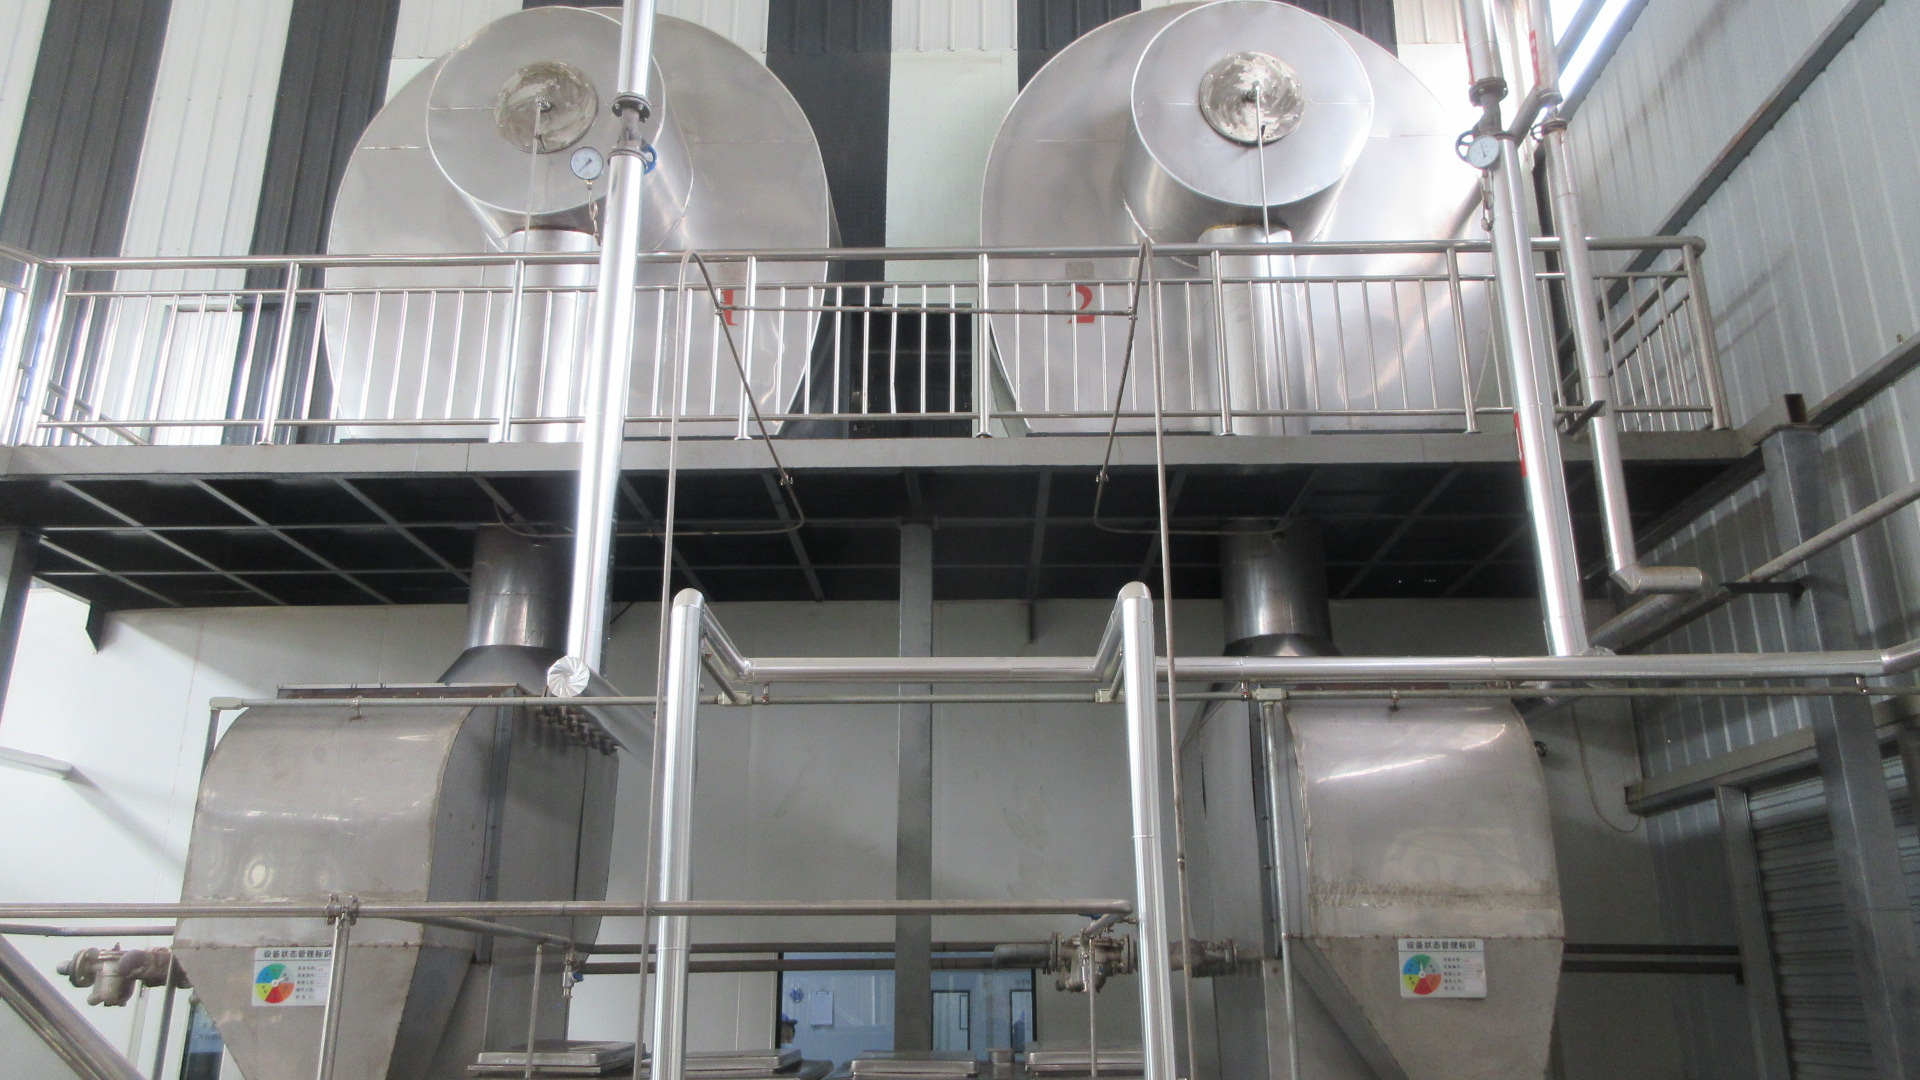
Industrial-scale drying tower creating uniform powder geometry.
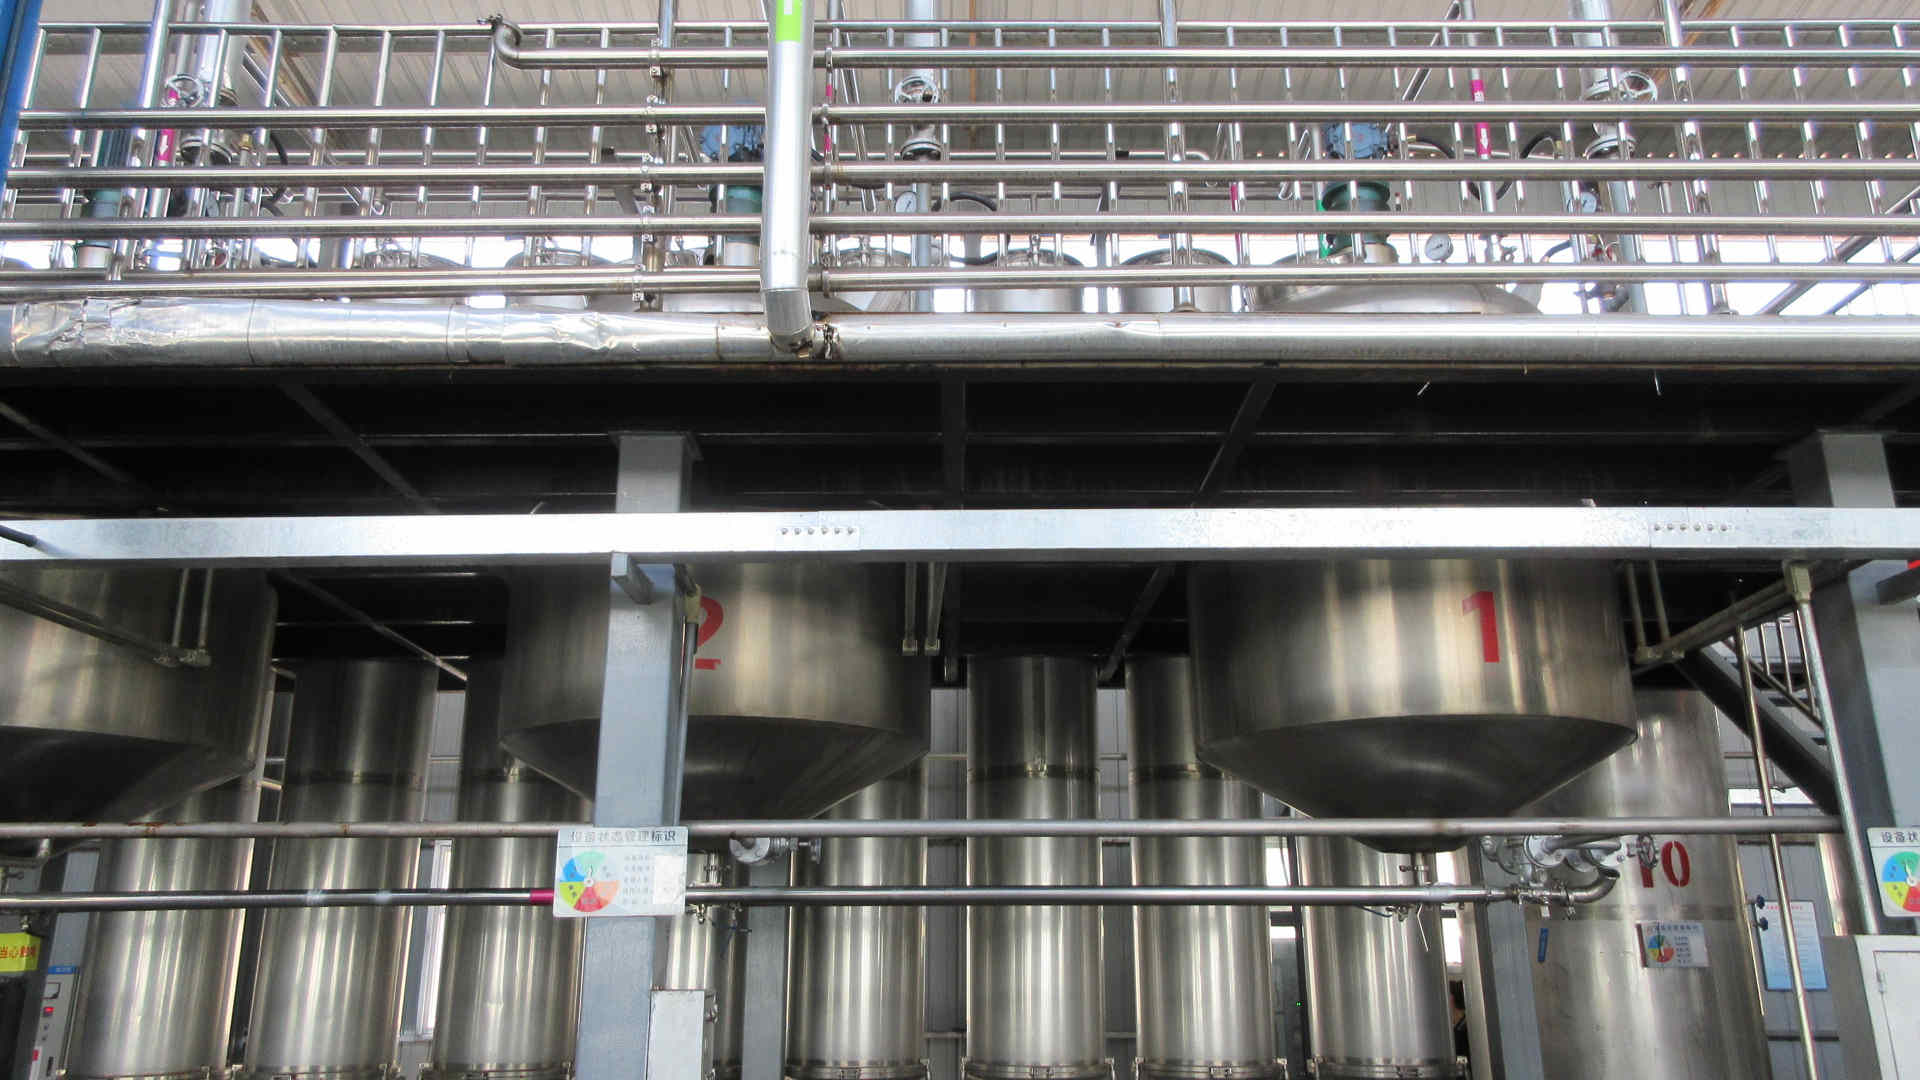
Advanced reactor for synthesis, surface modification, and emulsification.
Developing stable natural pigments requires addressing complex molecular challenges. Organic structures are naturally sensitive to UV exposure, oxidation, and heat. Shaanxi Mirae Biology's R&D efforts focus on microencapsulation technologies and molecular modifications to protect active pigments.
By utilizing high-shear homogenization, we wrap lipophilic colorants in stable, water-dispersible carriers, significantly expanding their application in liquid formulations.
Using natural carbohydrate shells like maltodextrin, gum arabic, or modified celluloses, we protect core pigments from thermal degradation during extrusion or baking processes.
Integrating trace plant antioxidants within color formulations inhibits auto-oxidation pathways, extending the color shelf-life of retail cosmetics and foods.
Colorants behave differently depending on the medium they are suspended in. The table below details how our range of natural and chemical raw materials function in global consumer goods and industrial systems.
| Application Field | Target Raw Material | Functional Value Added | Regulatory/Safety Standards |
|---|---|---|---|
| Clean-Label Beverages | Gardenia Yellow Extract | Brilliant, water-soluble hue with high heat stability. | ISO 22000, Non-GMO, CE Food Contact Standard. |
| Functional Makeup & Lip Balms | Bis-Diglyceryl Polyacyladipate-2 | Excellent pigment wetting agent and lanolin alternative. | 98% High Purity, Cruelty-Free, FDA Compliant. |
| Functional Confectionery | Thaumatin Powder | Sweetener and flavor enhancer that masks botanical off-notes. | CAS 53850-34-3, GRAS, CE Certified. |
| Personal Care & Shampoos | HPMC Powder | Rheology modifier that stabilizes pigment suspension. | Industrial/Detergent Grade, High Viscosity. |
| Skin Whitening Formulations | Thiamidol / Salmon DNA | Active ingredients that improve skin tone and cell renewal. | Cosmetic Grade, Certified Biocompatible. |
Answers to technical and regulatory questions commonly asked by procurement departments and compliance directors in the European Union and worldwide.
Browse our range of cosmetics preservatives, synthesis intermediates, dietary fiber additives, and functional oils designed to support diverse industrial and cosmetic formulations.
 Mirae Biology