High-purity organic pigments and natural coloring ingredients optimized for stability, compatibility, and clean-label compliance.
Phycocyanin Powder E18 Natural Blue Color Food Grade Bulk for Beverage Food Supplement
Learn More →
Sephcare Natural Food Coloring Plant Extract Red Pigment Beetroot Powder
Learn More →
Natural Food Pigment Water Soluble 99% Sodium Copper Chlorophyll Sodium Copper Chlorophyllin Chlorophyll Powder
Learn More →
B.C.I Supply 100% Natural Plant Pigment Colour Gardenia Jasminoides Ellis Extract E30-E100 Gardenia Blue
Learn More →Takamaka, a vital economic and environmental enclave in the Seychelles, represents a unique convergence of pristine biodiversity conservation and advanced ecological industrialization. As the global regulatory environment tightens around synthetic coal-tar dyes and heavy-metal based pigments, local sectors within Takamaka—spanning premium eco-resort packaging, marine-safe textile staining, artisanal bio-cosmetics, and pharmaceutical formulation—have turned to natural plant pigments to align with sustainable development directives.
The transition toward biological colorants in the region is heavily propelled by the local government's strict blue economy initiatives, ensuring that trace discharge from manufacturing and packaging processes contains zero toxic load. Shaanxi Mirae Biology Co., Ltd. has established a highly specialized service mechanism to cater to the specific requirements of Takamaka-based manufacturers, offering plant-derived alternatives that are biodegradable, non-hazardous to marine life, and highly resistant to tropical ambient humidity and heat degradation.
This localized supply channel bridges the gap between raw agrarian biological raw materials and pure, standardized commercial ingredients, meeting both local environmental compliance laws and global safety paradigms.
A professional manufacturer and global supplier specializing in the research, development, production, and distribution of high-quality plant extracts, nutritional ingredients, and specialty chemicals.
Located in Shaanxi Province, China, a region globally renowned for its rich botanical resources and advanced biotechnology industry, we combine premium natural ingredients with modern extraction technology to provide innovative and reliable solutions for customers worldwide.
With a strong commitment to quality, innovation, and customer satisfaction, we serve clients across the pharmaceutical, nutraceutical, cosmetic, food, and research industries. Our experienced technical team and strict quality control system ensure that every product meets international standards for purity, safety, and consistency.
Today, our products are exported to customers in North America, Europe, Southeast Asia, the Middle East, and many other international markets, earning a reputation for dependable quality and professional service.
At Shaanxi Mirae Biology Co., Ltd., we are committed to providing high-quality ingredients, reliable manufacturing, and professional services to help our global partners succeed. We look forward to building long-term and mutually beneficial partnerships with customers around the world.
Need Technical Assistance?
Contact our lab technicians to discuss customize carrier bases, color optimization under distinct pH levels, and temperature stability profiles.
Our advanced GMP-compliant processing facility utilizes state-of-the-art closed loop systems to extract, concentrate, and refine botanical pigments under clean room standards.
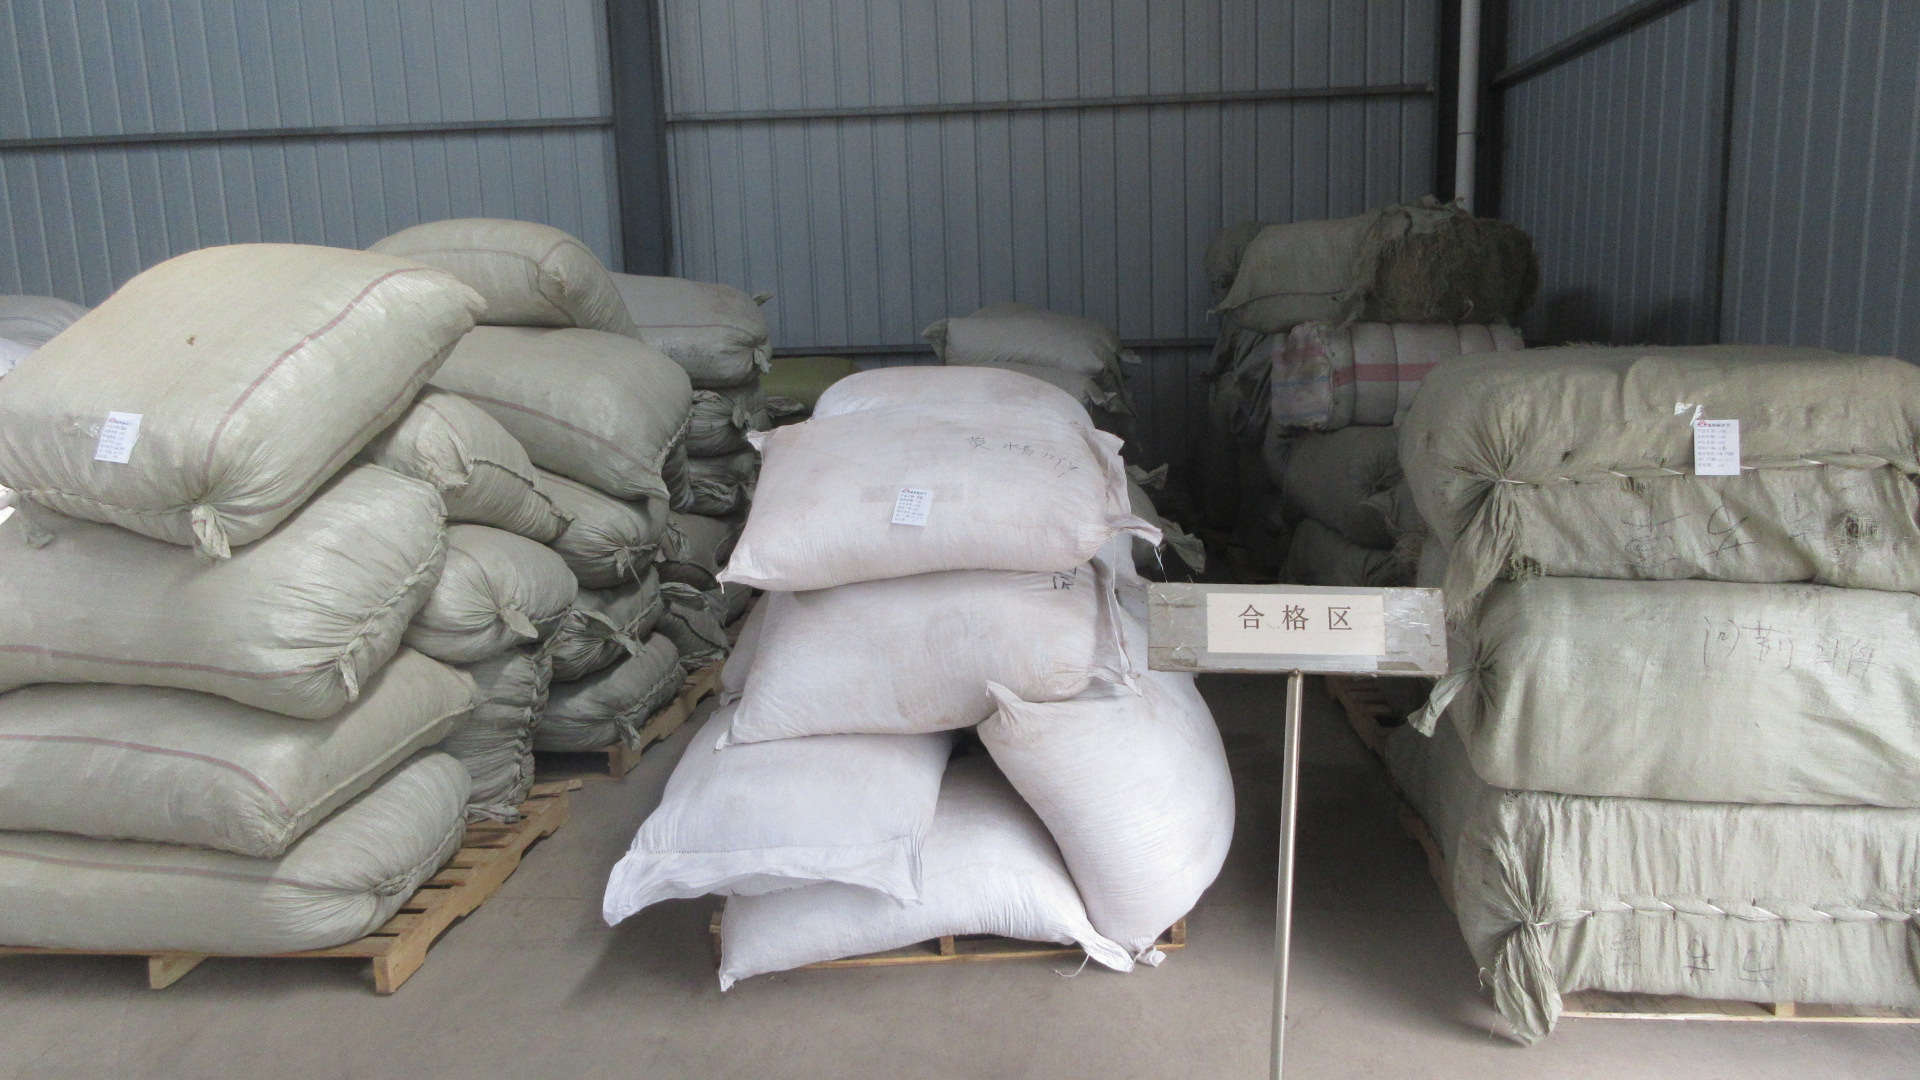
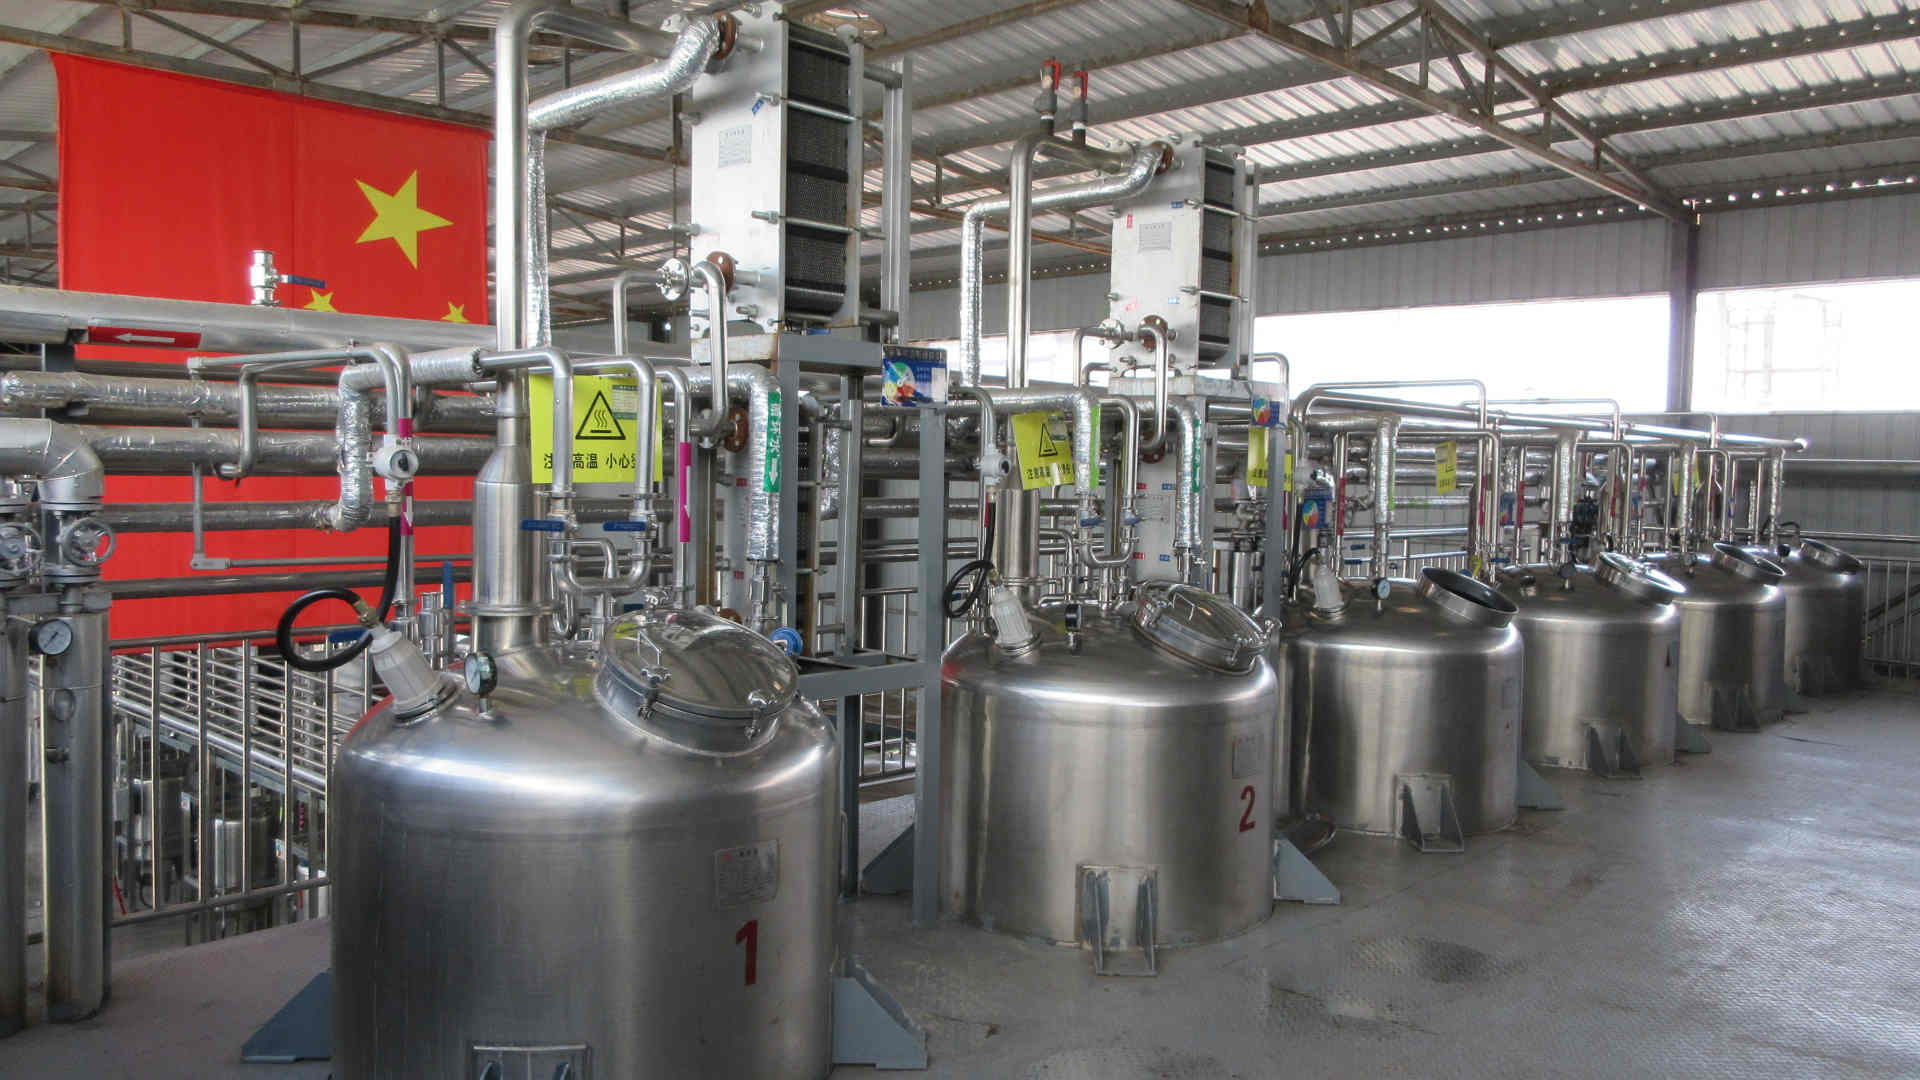
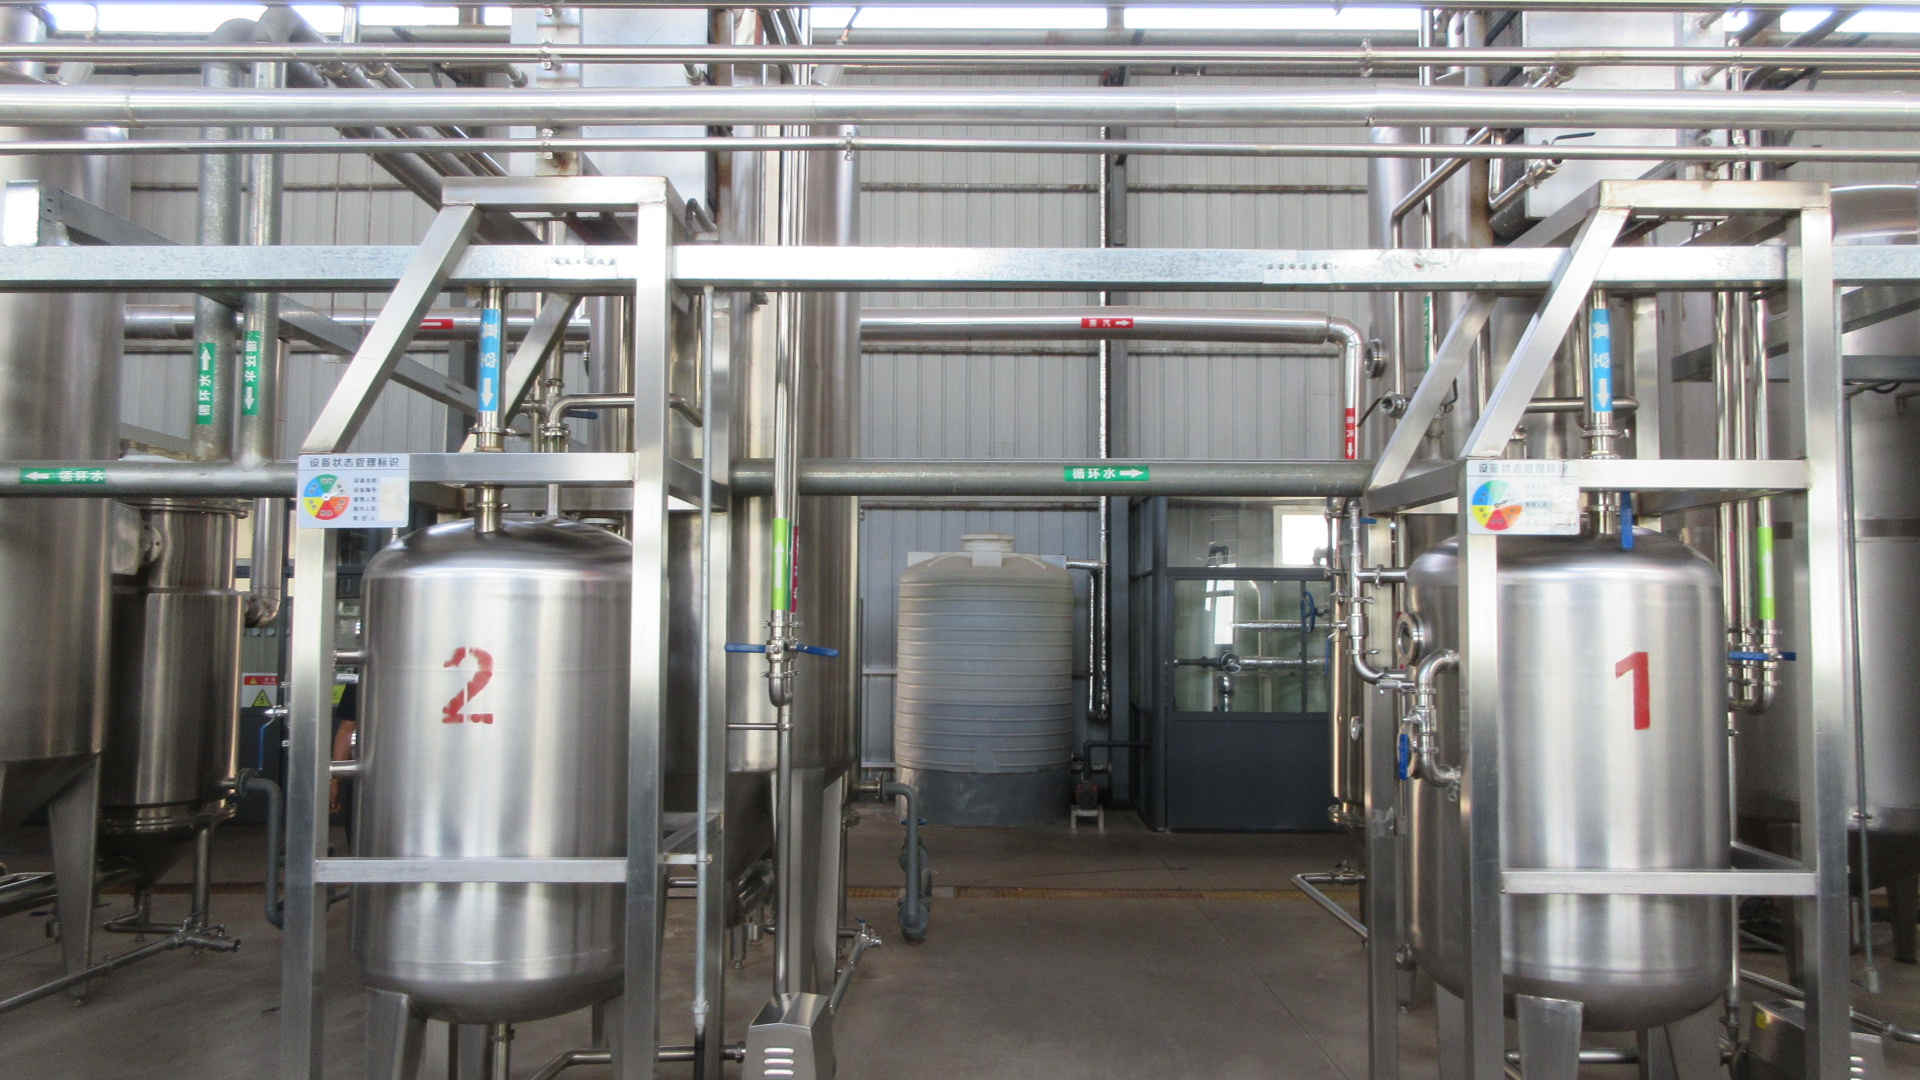
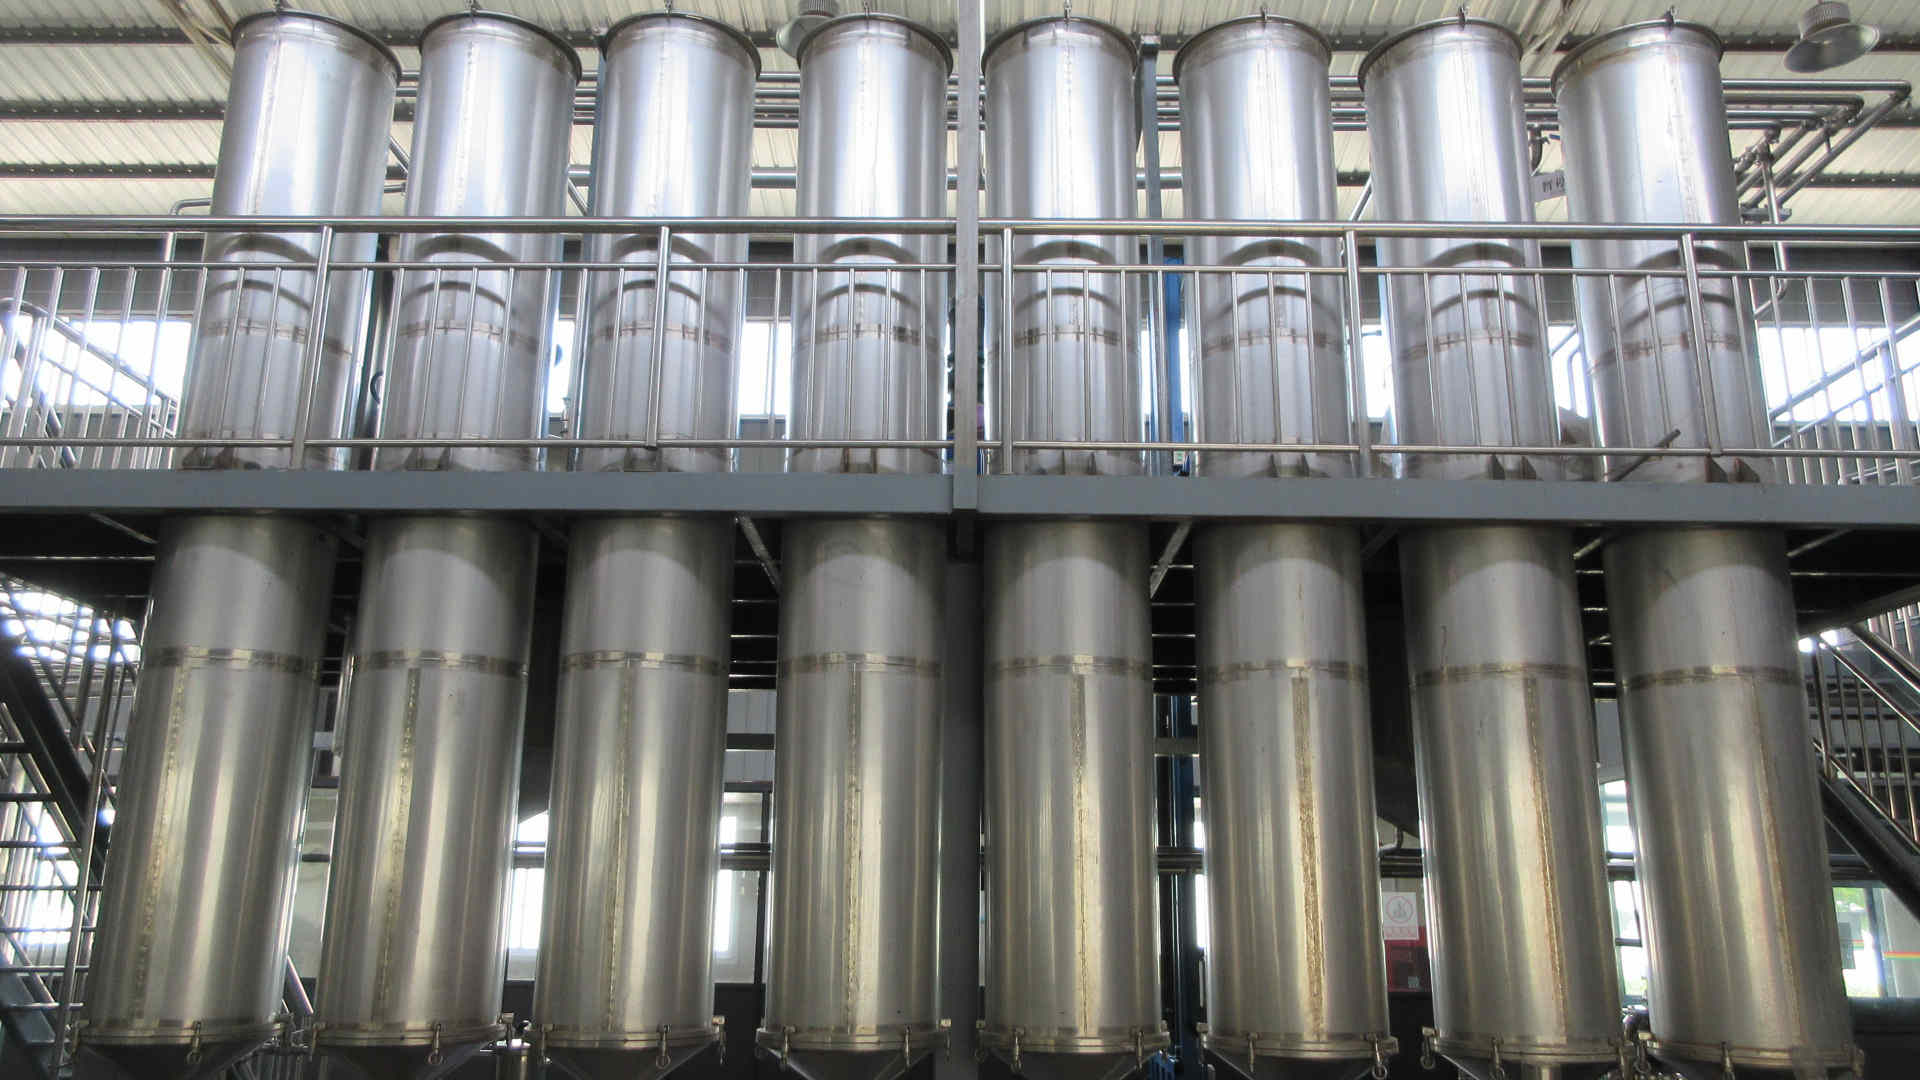
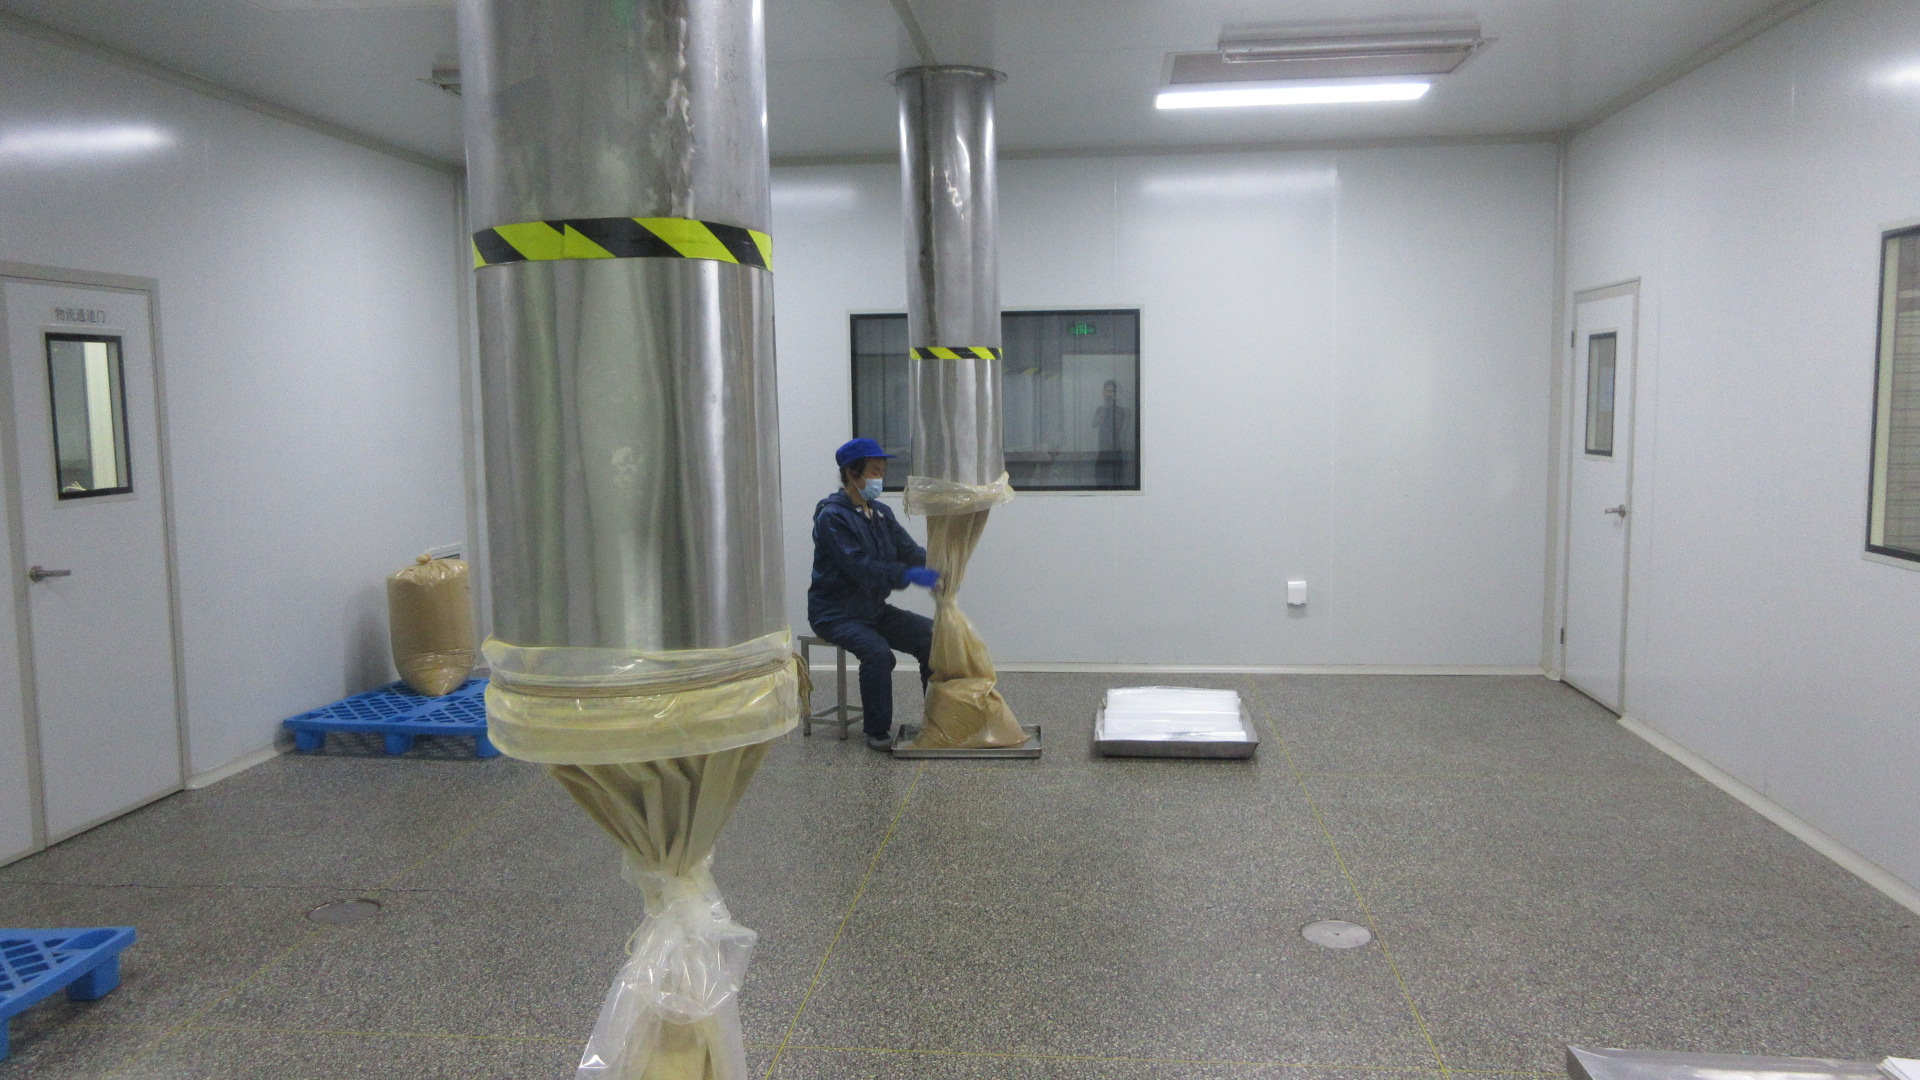
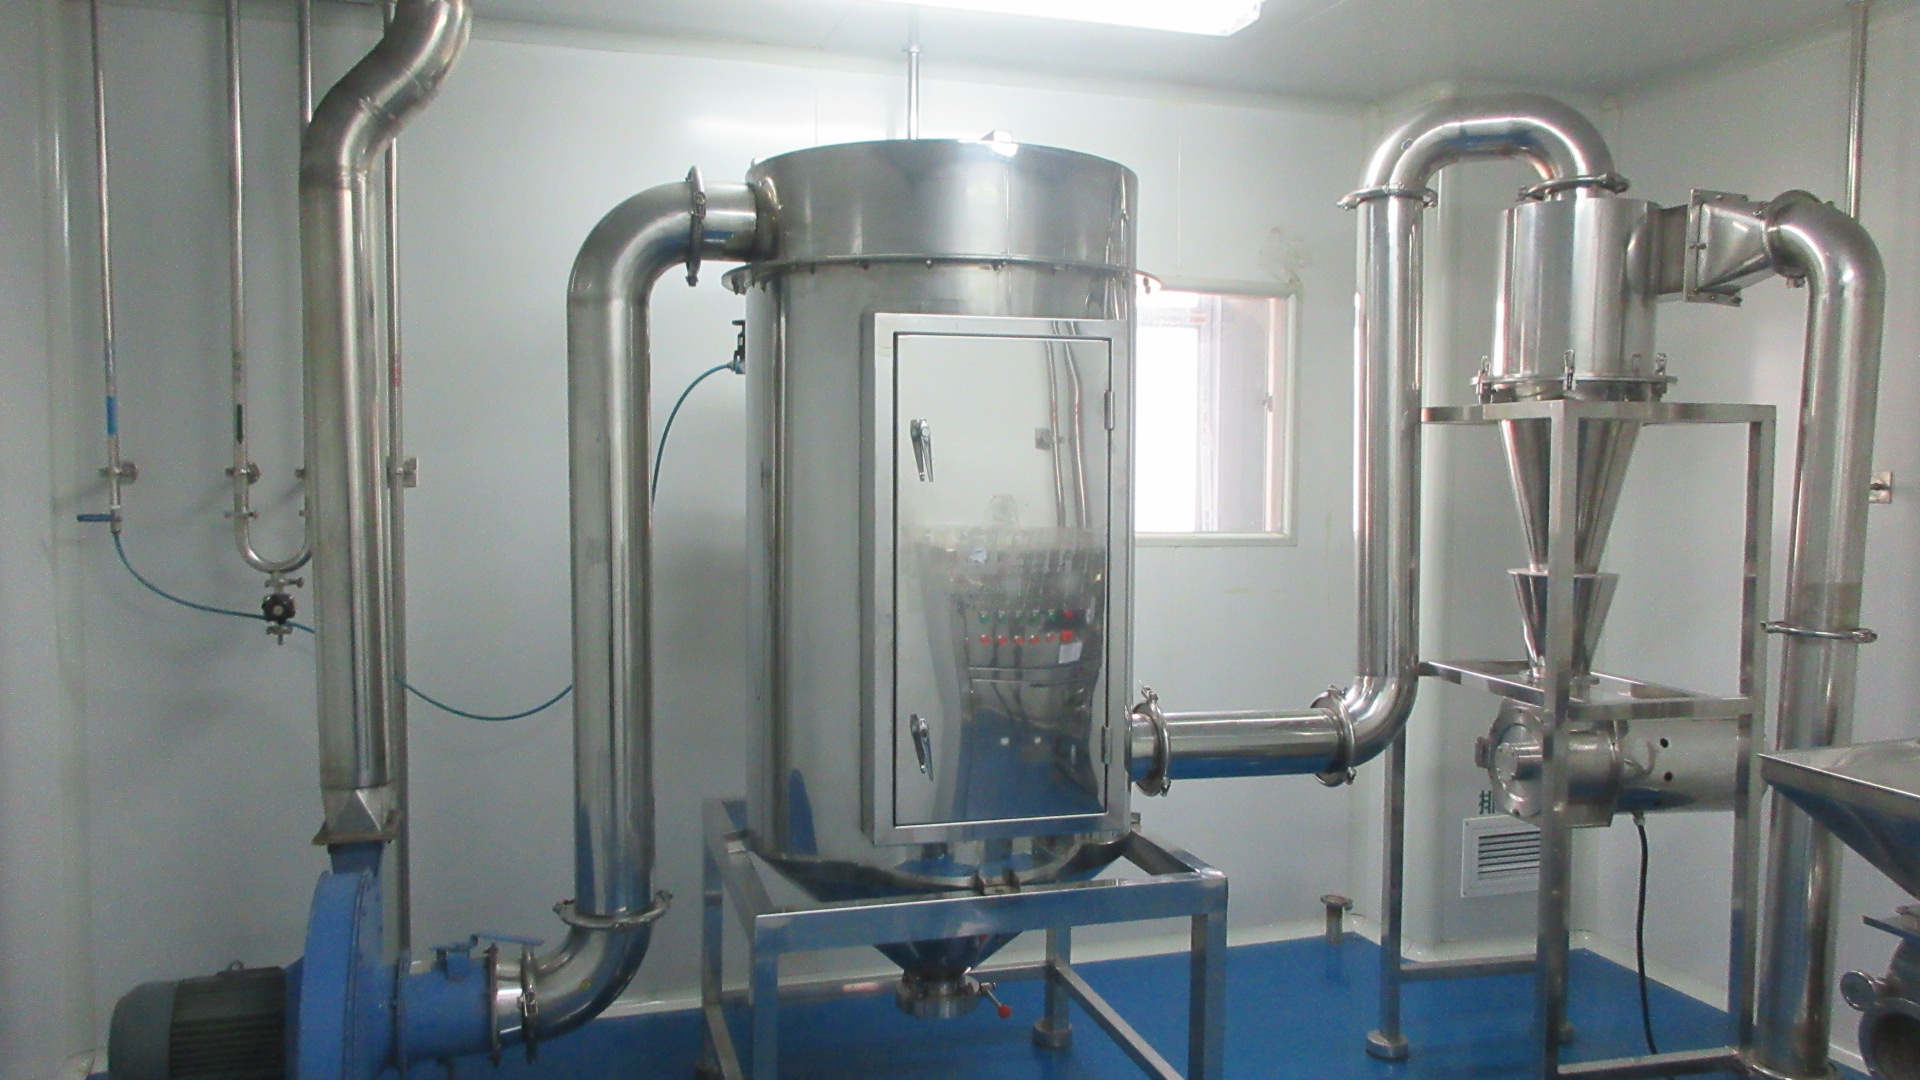
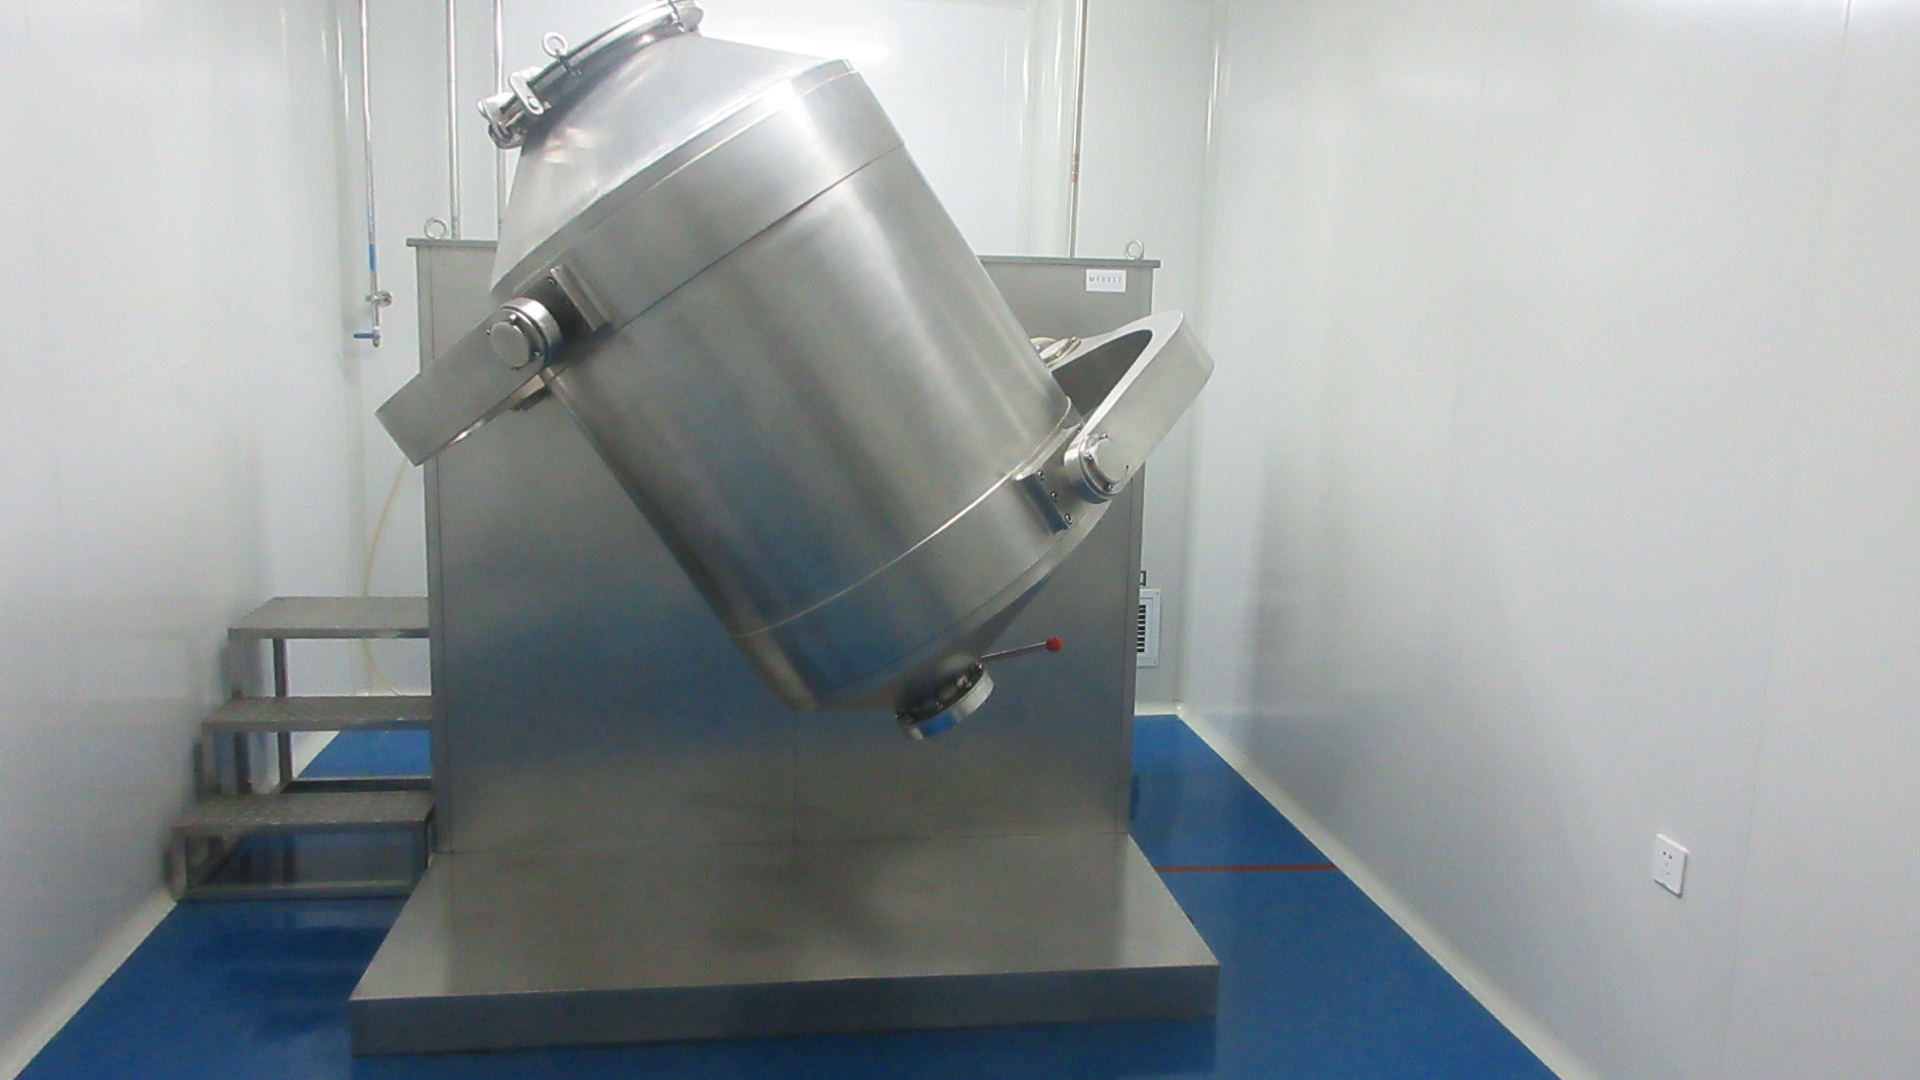
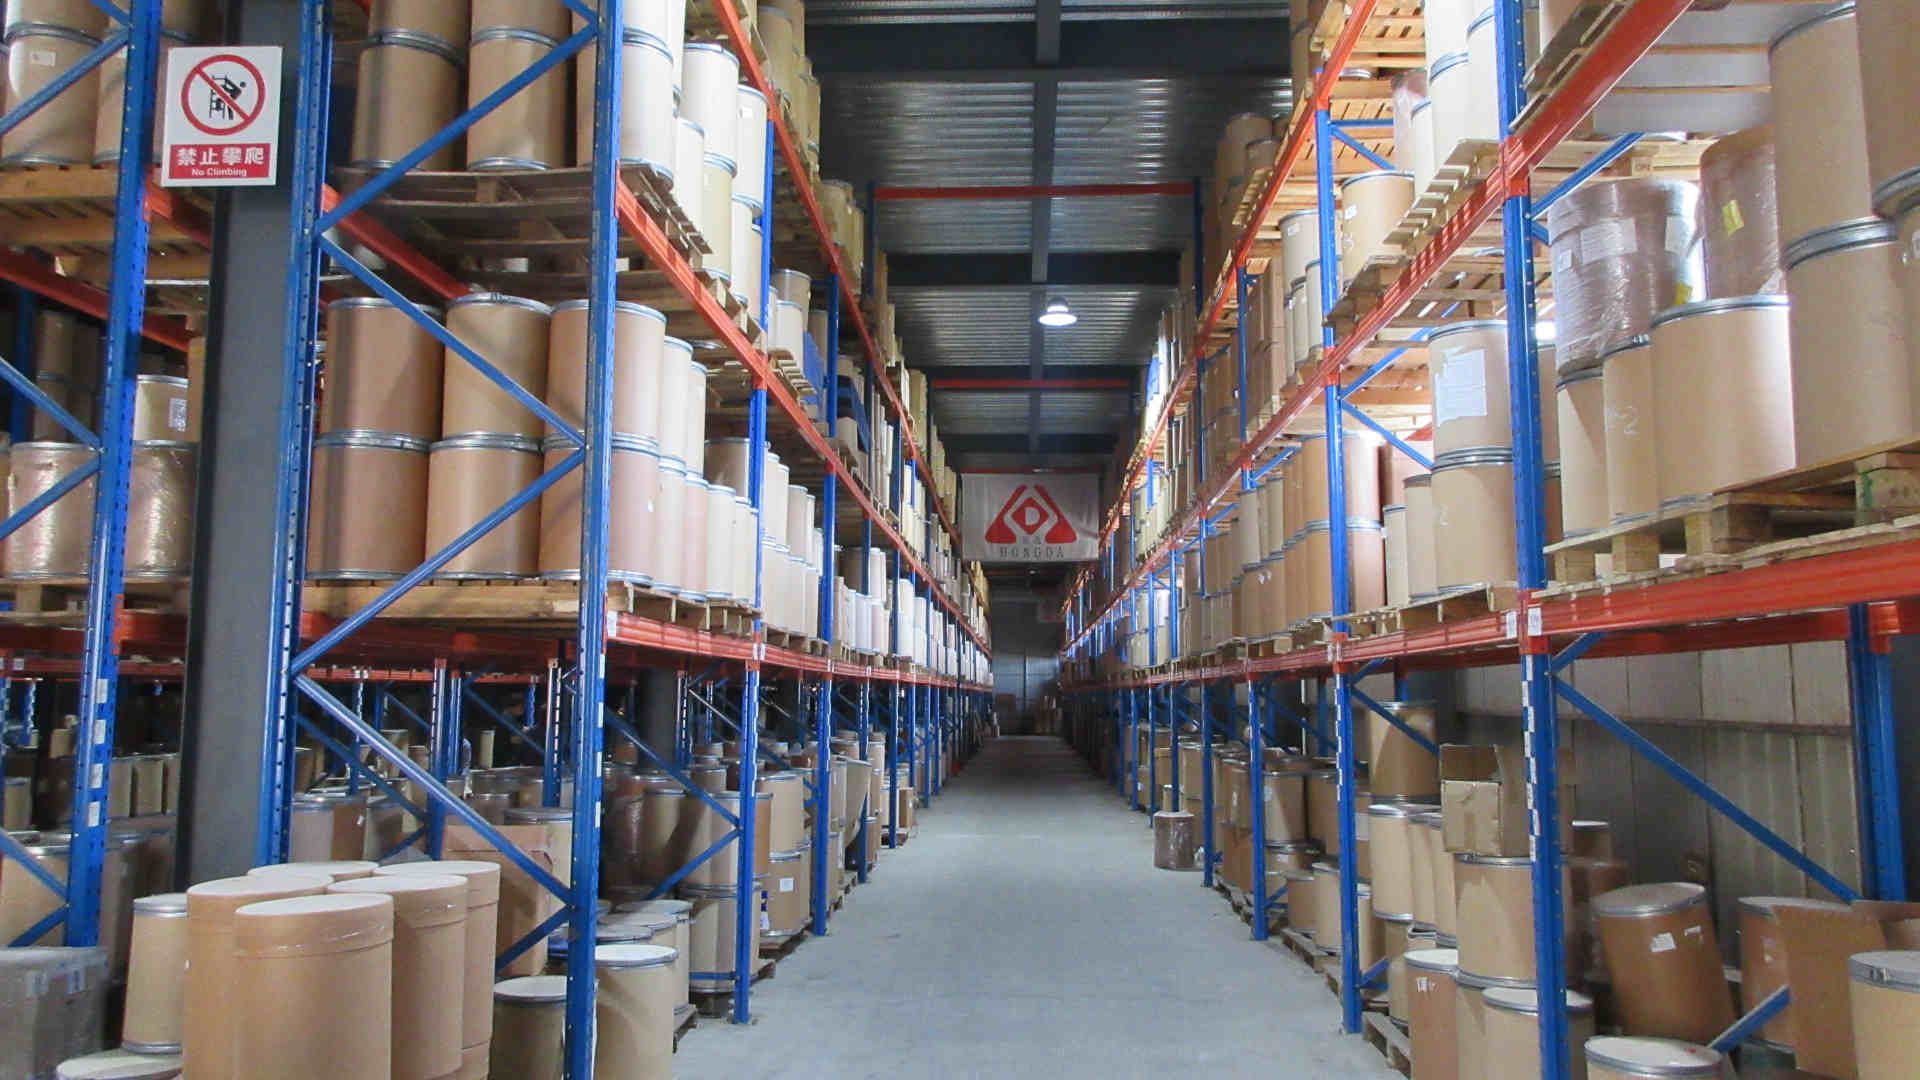
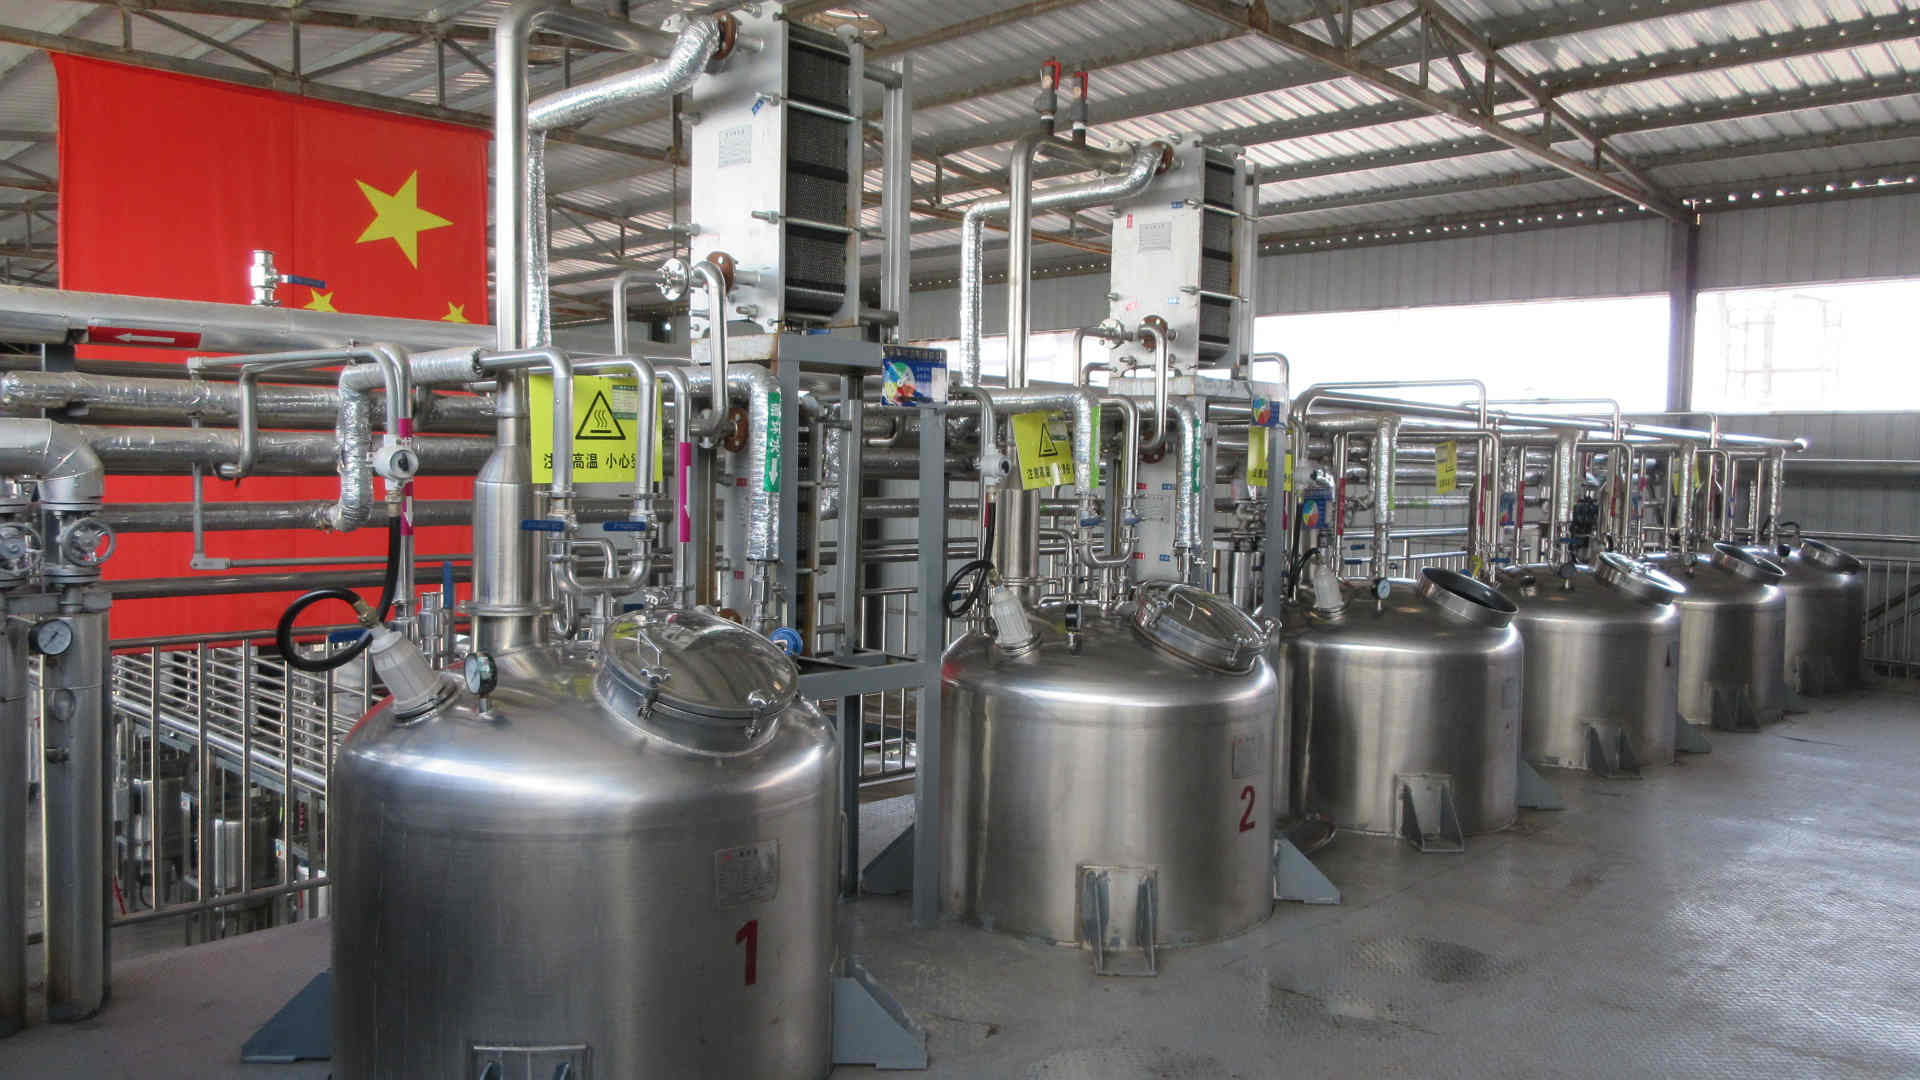
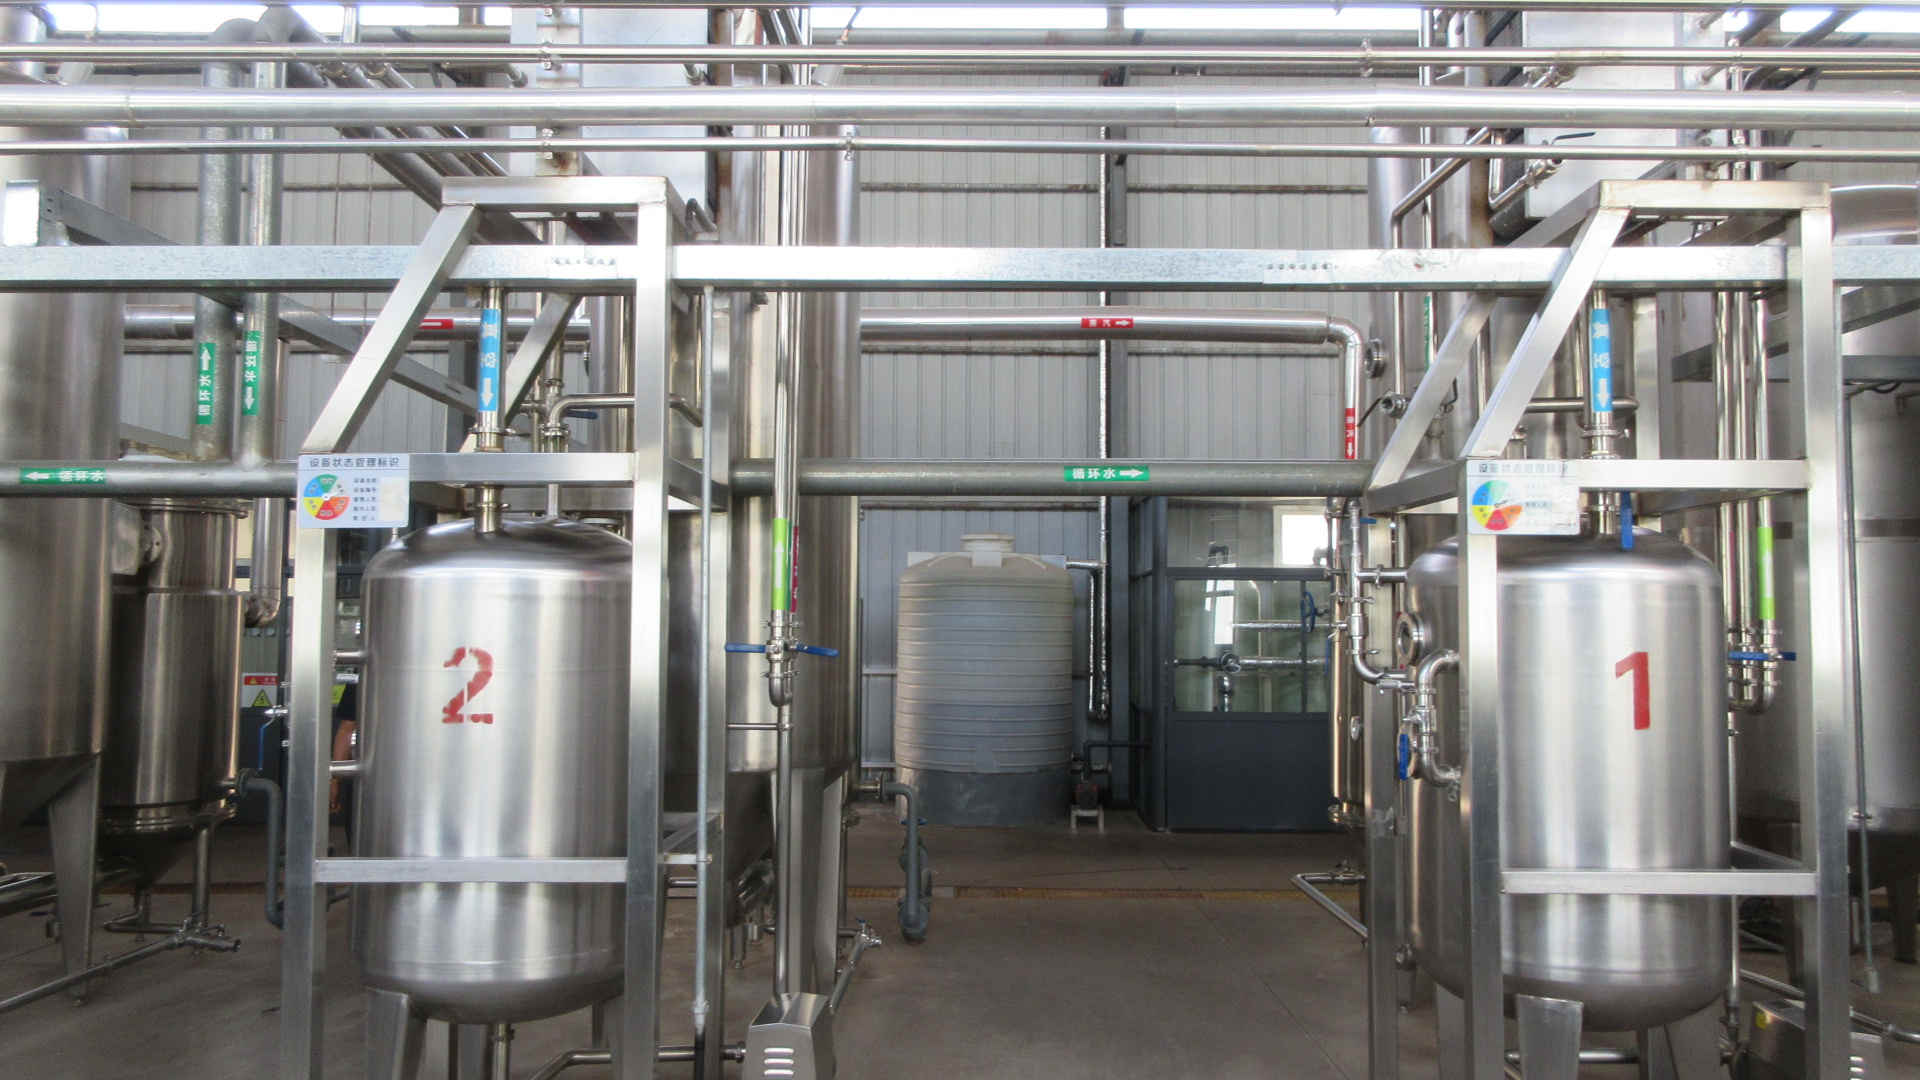
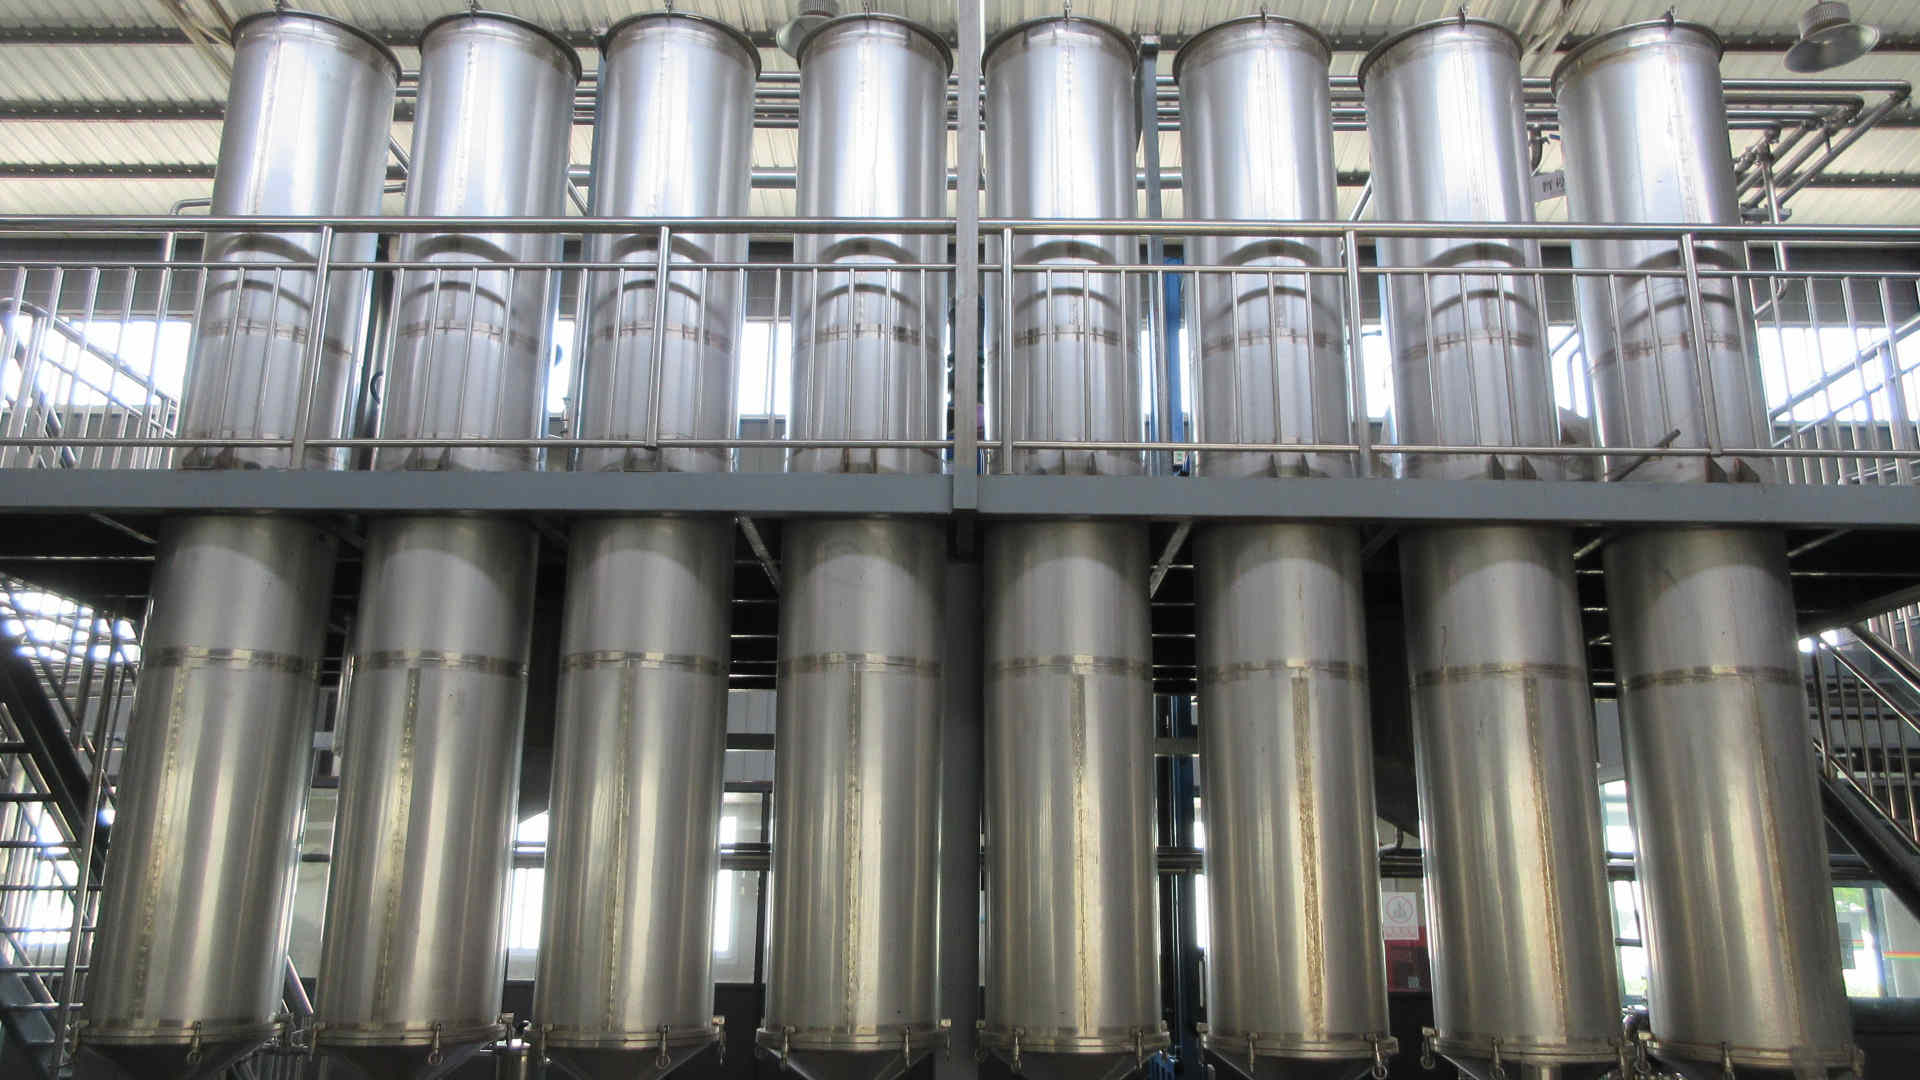
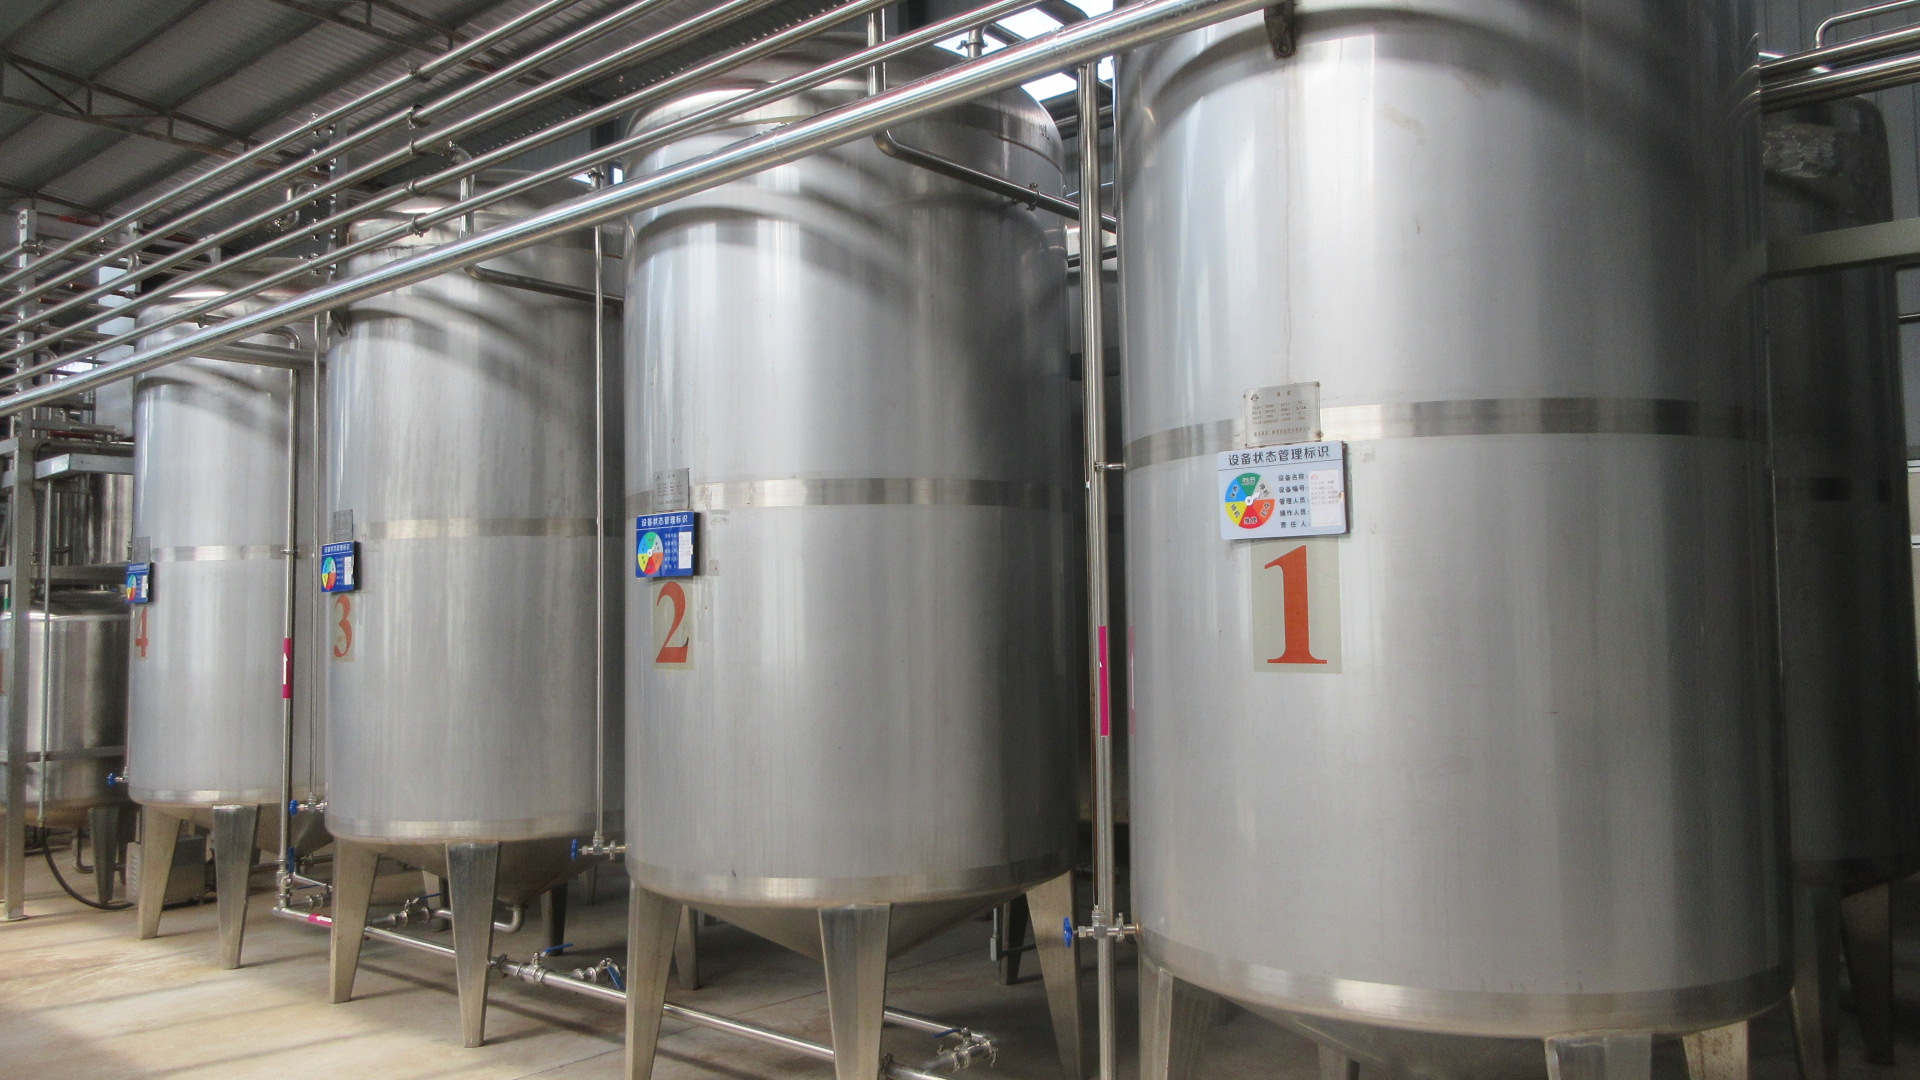
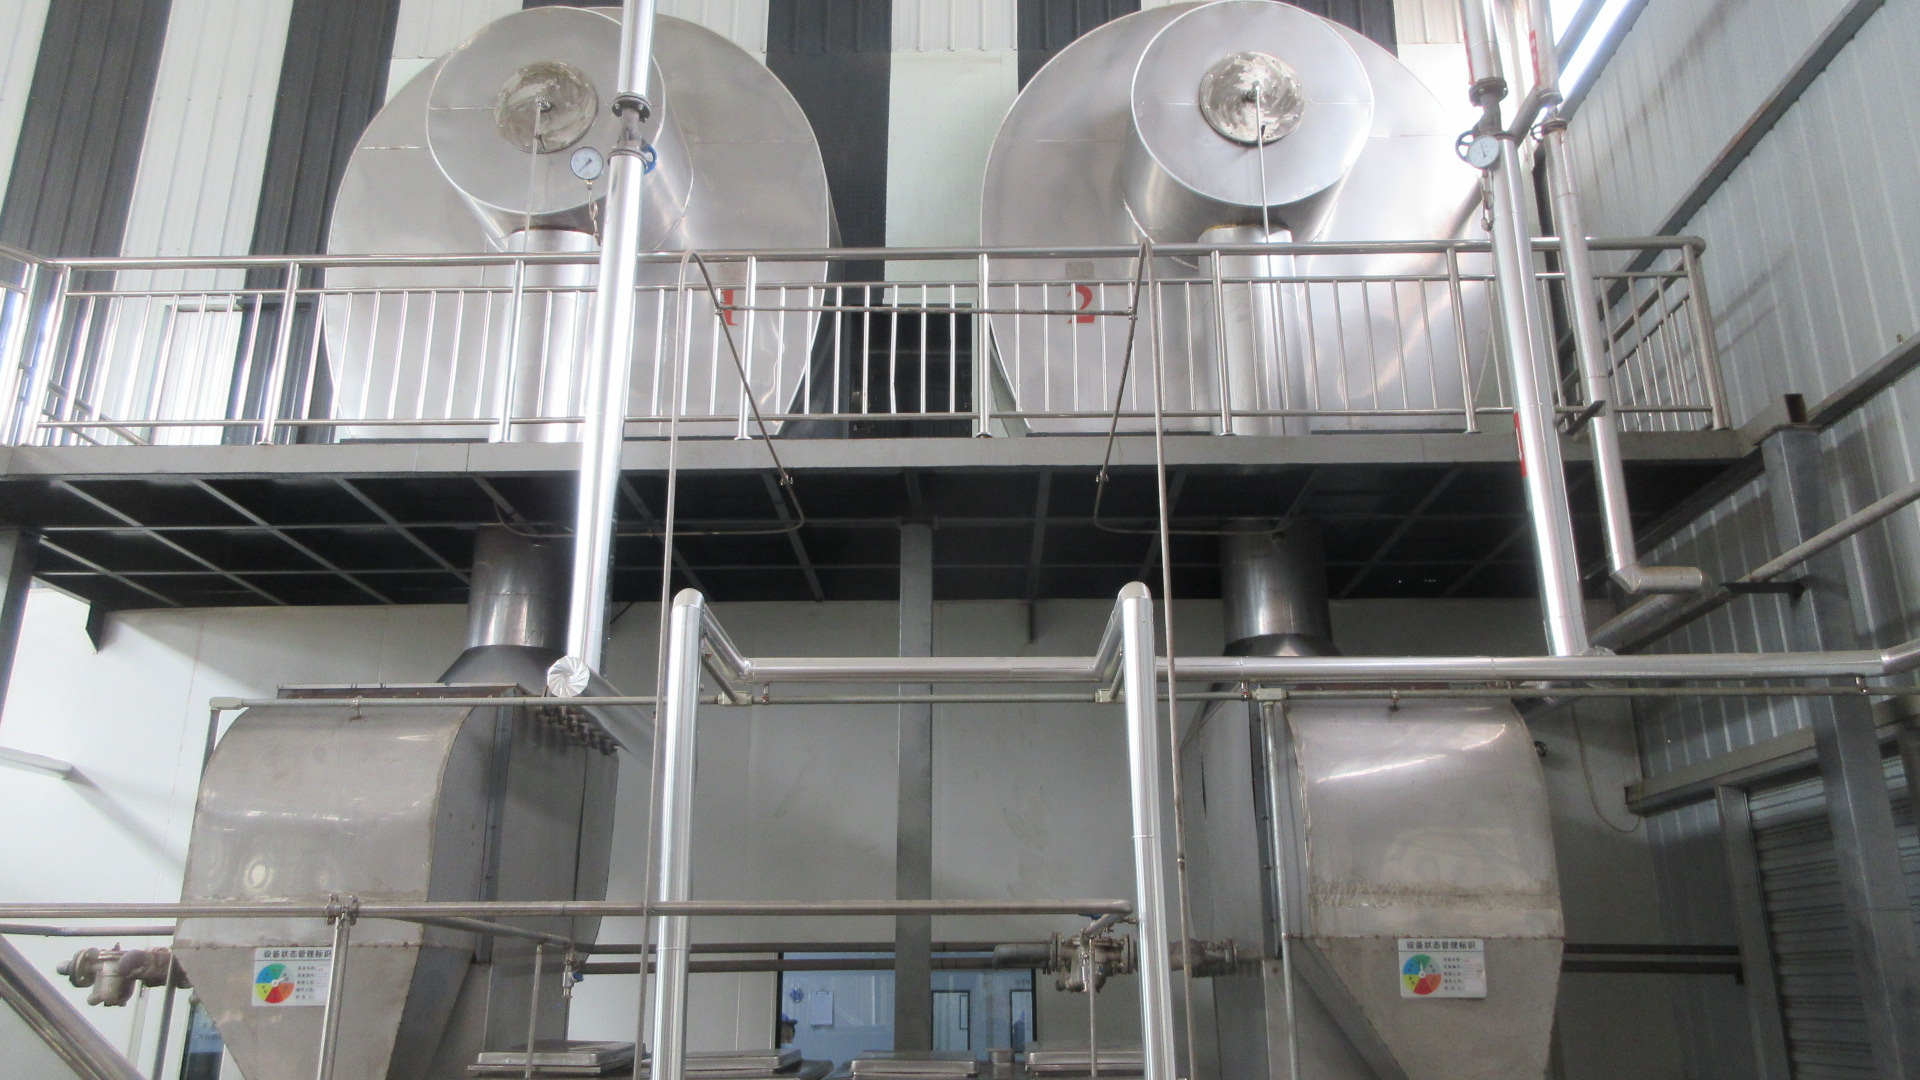
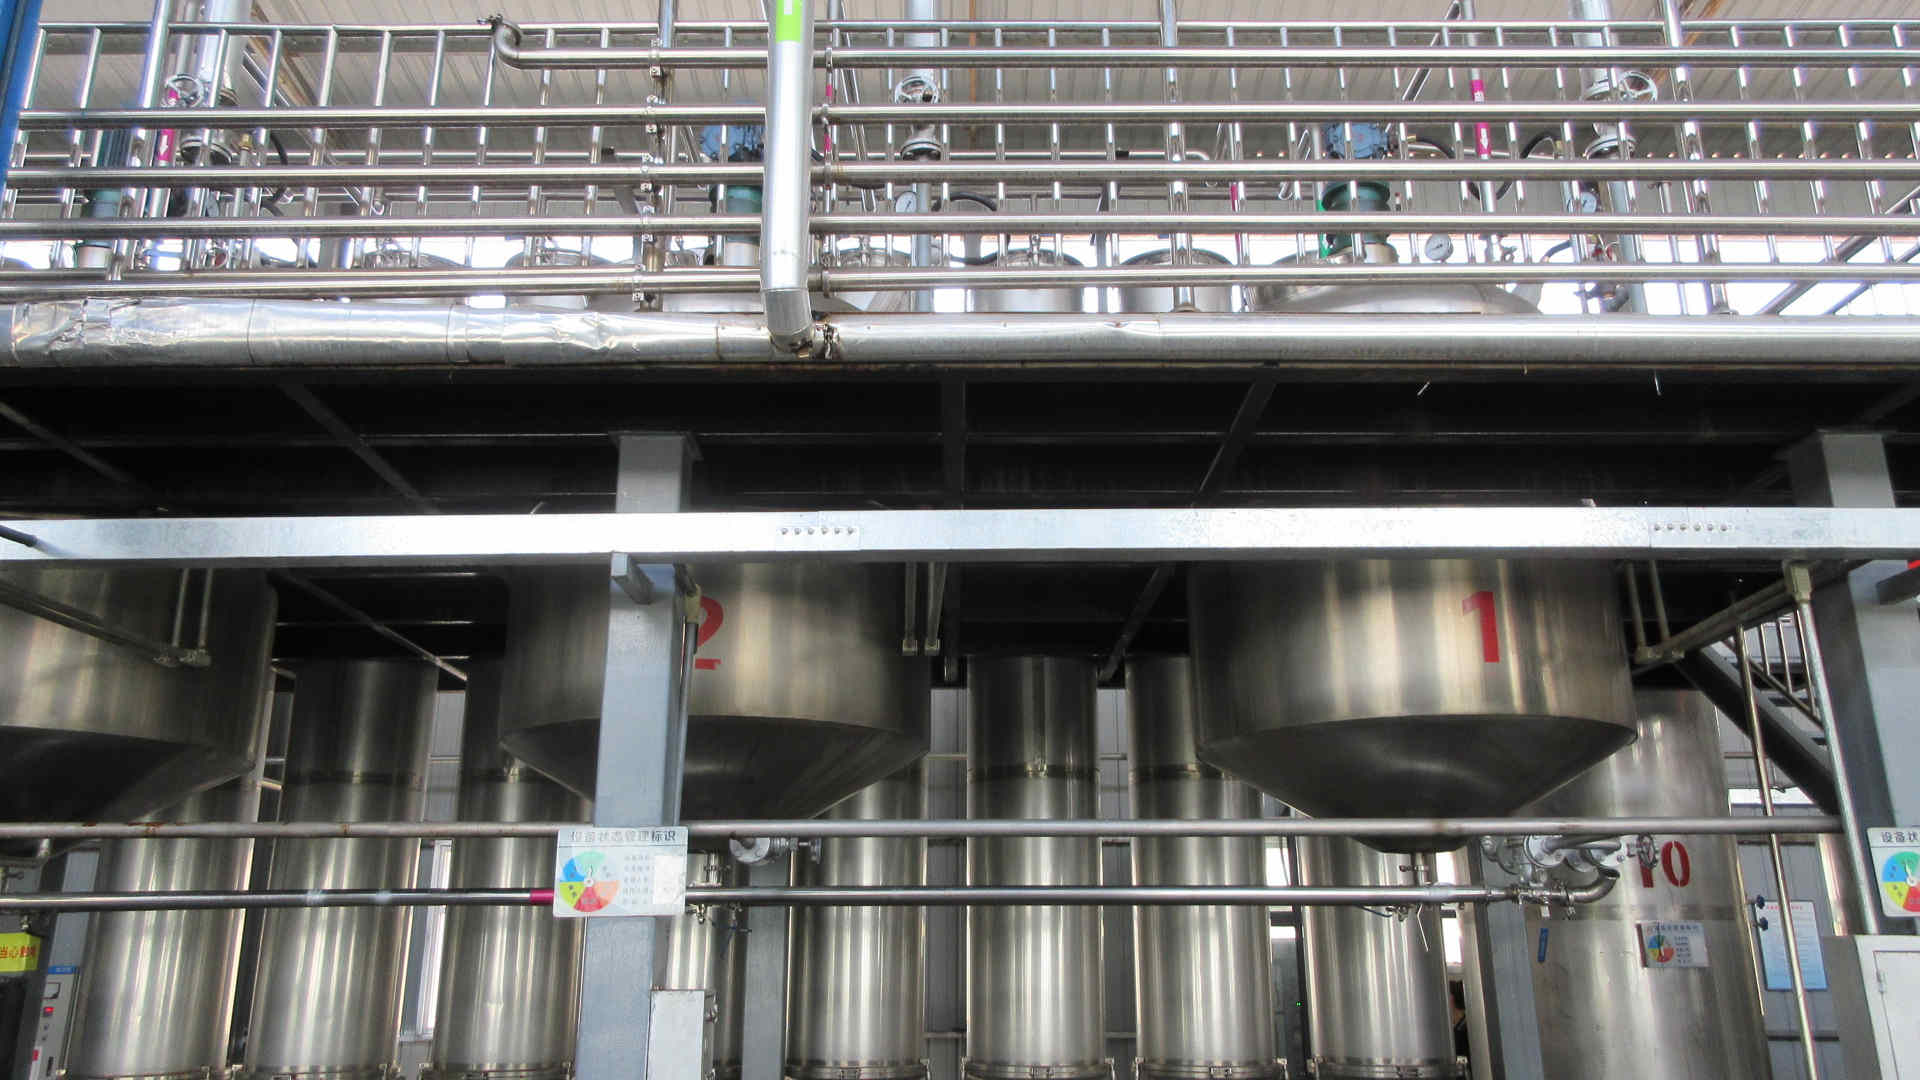
Analyzing the shift from chemical synthesis to clean-label plant derivatives in international markets.
Consumer vigilance and legislative bans by regulatory bodies such as the European Food Safety Authority (EFSA) and the US Food and Drug Administration (FDA) have triggered a global paradigm shift. The phased ban on Titanium Dioxide (E171) and restrictions on synthetic petroleum-derived colorants (e.g., Tartrazine, Allura Red) have compelled food, beverage, and cosmetic R&D divisions to restructure their raw material registries. Global sourcing directors must now identify factories that offer not only naturality but equivalent thermal stability and shelf life.
Our company satisfies this critical gap by providing micro-encapsulated plant colorants that exhibit high stability profile under pasteurization, high-pressure processing (HPP), and long-term shelf storage. With deep extraction capability in Shaanxi, we ensure continuous global supply and low batch-to-batch deviation, satisfying global supply chain safety specifications.
Specialized coloring pigments suited for pharmaceutical coatings, eco-inks, and high-performance masterbatches.
Natural Blue Plant Extract Pigment/Cyanophycin Eco-Friendly Dye
Learn More →
Amulyn High Quality Natural Plant Extract Purple Yam Powder (Ube Powder) For Food Additive Natural Pigments
Learn More →
Best Reputation Sorghum Red Pigment Pure Natural Pigment Sorghum Seed Plant Extract
Learn More →
Bulk Gardenia Green Supplier Natural Plant Pigment Powder for Food and Beverage Coloring Applications
Learn More →Pioneering processing paths that enhance yield, bio-availability, and matrix stability of organic color pigments.
Utilizing pressurized carbon dioxide at precise critical temperatures to extract lipophilic color complexes without thermal damage. This ensures full retention of native botanical integrity without residual toxic solvents.
Standardizing color values through molecular weight cut-off filtration membranes and industrial column chromatography. This system concentrates active coloring agents (such as phycocyanobilin or betanin) while removing odor-active and bitter compounds.
Applying natural protective carrier polysaccharides (e.g., gum arabic, organic maltodextrin) to coat color particles during atomized spray drying. This technology provides excellent oxygen, light, and heat resistance, allowing natural colors to thrive in diverse manufacturing environments.
Explore our diverse industrial, food-grade, and cosmetic-grade coloring solutions engineered to international standards.
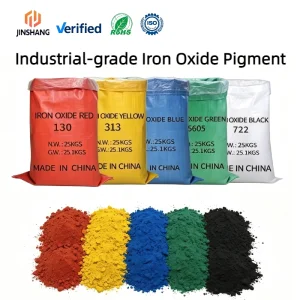
Red 130 Yellow 313 Black 722 Synthetic Iron Oxide Pigment Inorganic Colorant For Asphalt Ceramic Tiles Construction Wholesale
Learn More →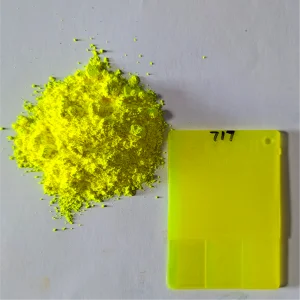
Superior Dispersion Non-fading Day Glow Pigment For Specialized Polyolefin Masterbatch And Universal Resin Coloration
Learn More →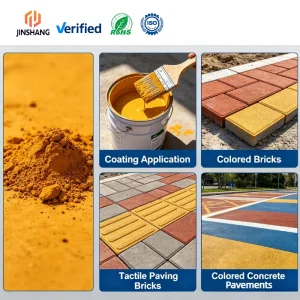
Vibrant Color ROHS Verified Weather Resistant Synthetic Iron Oxide Yellow Powder Pigment Leather Pigments Coating Pigment
Learn More →
Natural Plant Pigment Colour Gardenia Jasminoides Ellis Extract E30-E100 Gardenia Blue Powder
Learn More →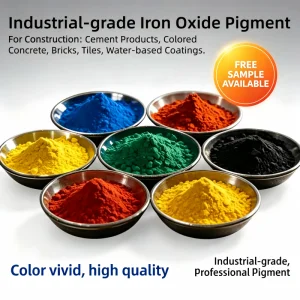
Iron Oxide Pigment Factory Direct - High Purity 325 Mesh Synthetic Pigment For Concrete Bricks Paving Stone And Cement Colorant
Learn More →
Brazilwood Red Pigment Natural Medieval Plant Pigments Oil Painting Tempera Watercolor
Learn More →
Colors Pigment Nail Powder Fluorescent Powder Color Nail Pigments Glitter Neon Pigment Eyeshadow Powder RTS-127
Learn More →
Synthetic Mica Powder Heavy Metal Free High Whiteness Ultra Fine Flake Cosmetic Coatings Pearlescent Pigment Fluorphlogopite
Learn More →Key inquiries regarding stability, standardization, compliance, and formulation integration.
Phycocyanin is inherently sensitive to high temperatures. To mitigate thermal degradation during pasteurization, we offer micro-encapsulated formulations utilizing sodium alginate or maltodextrin carriers. This protects the chromophore structure up to 80°C for short cycles. Additionally, buffer systems adjusting pH levels between 5.5 and 6.0 significantly improve color retention.
Yes, our raw materials undergo comprehensive testing. Our production facility is certified under ISO 9001, HACCP, GMP, Kosher, and Halal standards. We provide batch-specific Certificates of Analysis (COA) detailing heavy metal assays, microbiological count limits, and pesticide residue profiling to meet rigorous international food safety criteria.
While direct replacement requires adjusting the loading levels due to color strength variances, our specialized pigments (such as our Superior Dispersion Non-fading Day Glow Pigments and modified chlorophyll powders) are engineered to withstand extrusion temperatures up to 220°C, making them highly compatible with standard polyolefin masterbatch configurations.
We maintain strict agricultural control over our raw materials source fields. Before entering extraction tanks, botanical inputs undergo testing for heavy metals via Inductively Coupled Plasma Mass Spectrometry (ICP-MS) and multi-residue gas chromatography. We enforce limits stricter than European Pharmacopoeia tolerances, keeping lead and arsenic below 0.5 ppm.
Under dry, cool storage conditions, shielded from direct sunlight and moisture, our dry-form plant powders maintain stability for 24 months. For liquid forms, we recommend keeping them sealed in aseptic containers under refrigeration (4°C) to prevent natural biodegradation or atmospheric oxidation.
Yes, we specialize in high-mesh dry pulverization. We can process botanical powders to an ultra-fine particle size distribution ranging from 120 mesh to 325 mesh (sub-45 microns). This is ideal for applications demanding smooth skin adhesion, such as compact powders, eyeshadows, and premium organic cosmetic creams.
 Mirae Biology