Premium grade bioactive compounds, specialized antioxidants, botanical extracts, and custom formulations engineered for global B2B procurement.
In an era defined by preventive healthcare, functional cosmetics, sustainable agriculture, and bio-based industrial chemistry, the global market for vitamins, minerals, botanical extracts, and synthetic active precursors is undergoing a fundamental structural transformation. Modern enterprise procurement teams, pharmaceutical formulators, and global brands no longer demand mere commodity chemical supply; they require fully traceable, high-purity, batch-consistent, and environmentally compliant raw materials backed by rigorous scientific documentation and international regulatory support.
As a leading vitamins and minerals factory and exporter, Shaanxi Mirae Biology Co., Ltd. stands at the forefront of this industrial transition. By combining Shaanxi's unique geographical access to rich botanical reserves with cutting-edge enzymatic hydrolysis, supercritical molecular extraction, and advanced spray-drying technologies, we empower B2B buyers across North America, Europe, Asia-Pacific, and the Middle East to engineer high-performance finished products.
Unlike conventional bulk ingredient brokers, primary manufacturers offering advanced technical integration deliver significant efficiency gains across the supply chain:
Enterprise Manufacturing Capabilities & Global Supply Reach
Shaanxi Mirae Biology Co., Ltd. is a professional manufacturer and global supplier specializing in the research, development, production, and distribution of high-quality plant extracts, nutritional ingredients, cosmetic raw materials, peptides, and specialty chemicals.
Located in Shaanxi Province, China, a region renowned for its rich botanical resources and advanced biotechnology industry, we combine premium natural ingredients with modern extraction technology to provide innovative and reliable solutions for customers worldwide.
With a strong commitment to quality, innovation, and customer satisfaction, we serve clients across the pharmaceutical, nutraceutical, cosmetic, food, and research industries. Our experienced technical team and strict quality control system ensure that every product meets international standards for purity, safety, and consistency.
Today, our products are exported to customers in North America, Europe, Southeast Asia, the Middle East, and many other international markets, earning a reputation for dependable quality and professional service.
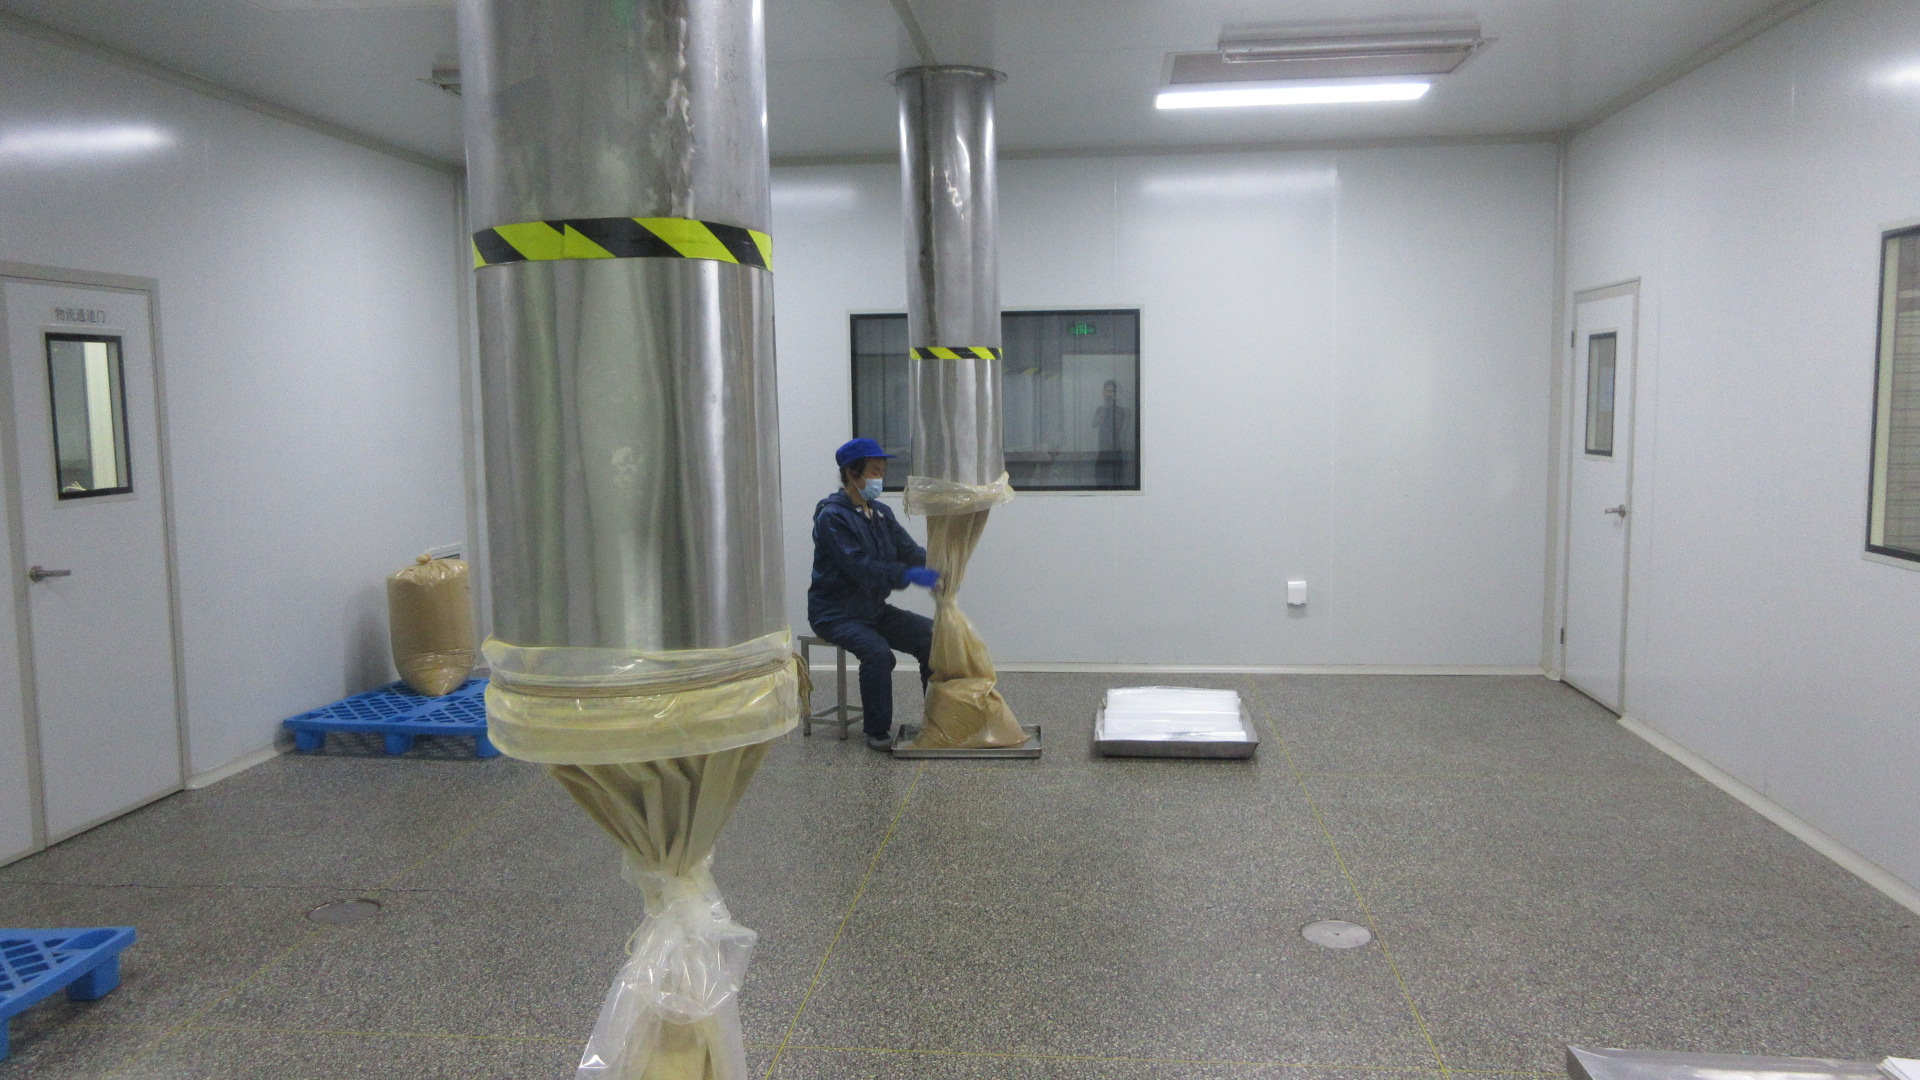
Professional manufacturer with years of industry experience, operating dedicated pilot and commercial-scale production units built to cGMP standards.
Complete testing procedures utilizing HPLC, GC-MS, AAS, and LC-MS-MS to verify purity, heavy metal limits, residual solvents, and microbiological compliance.
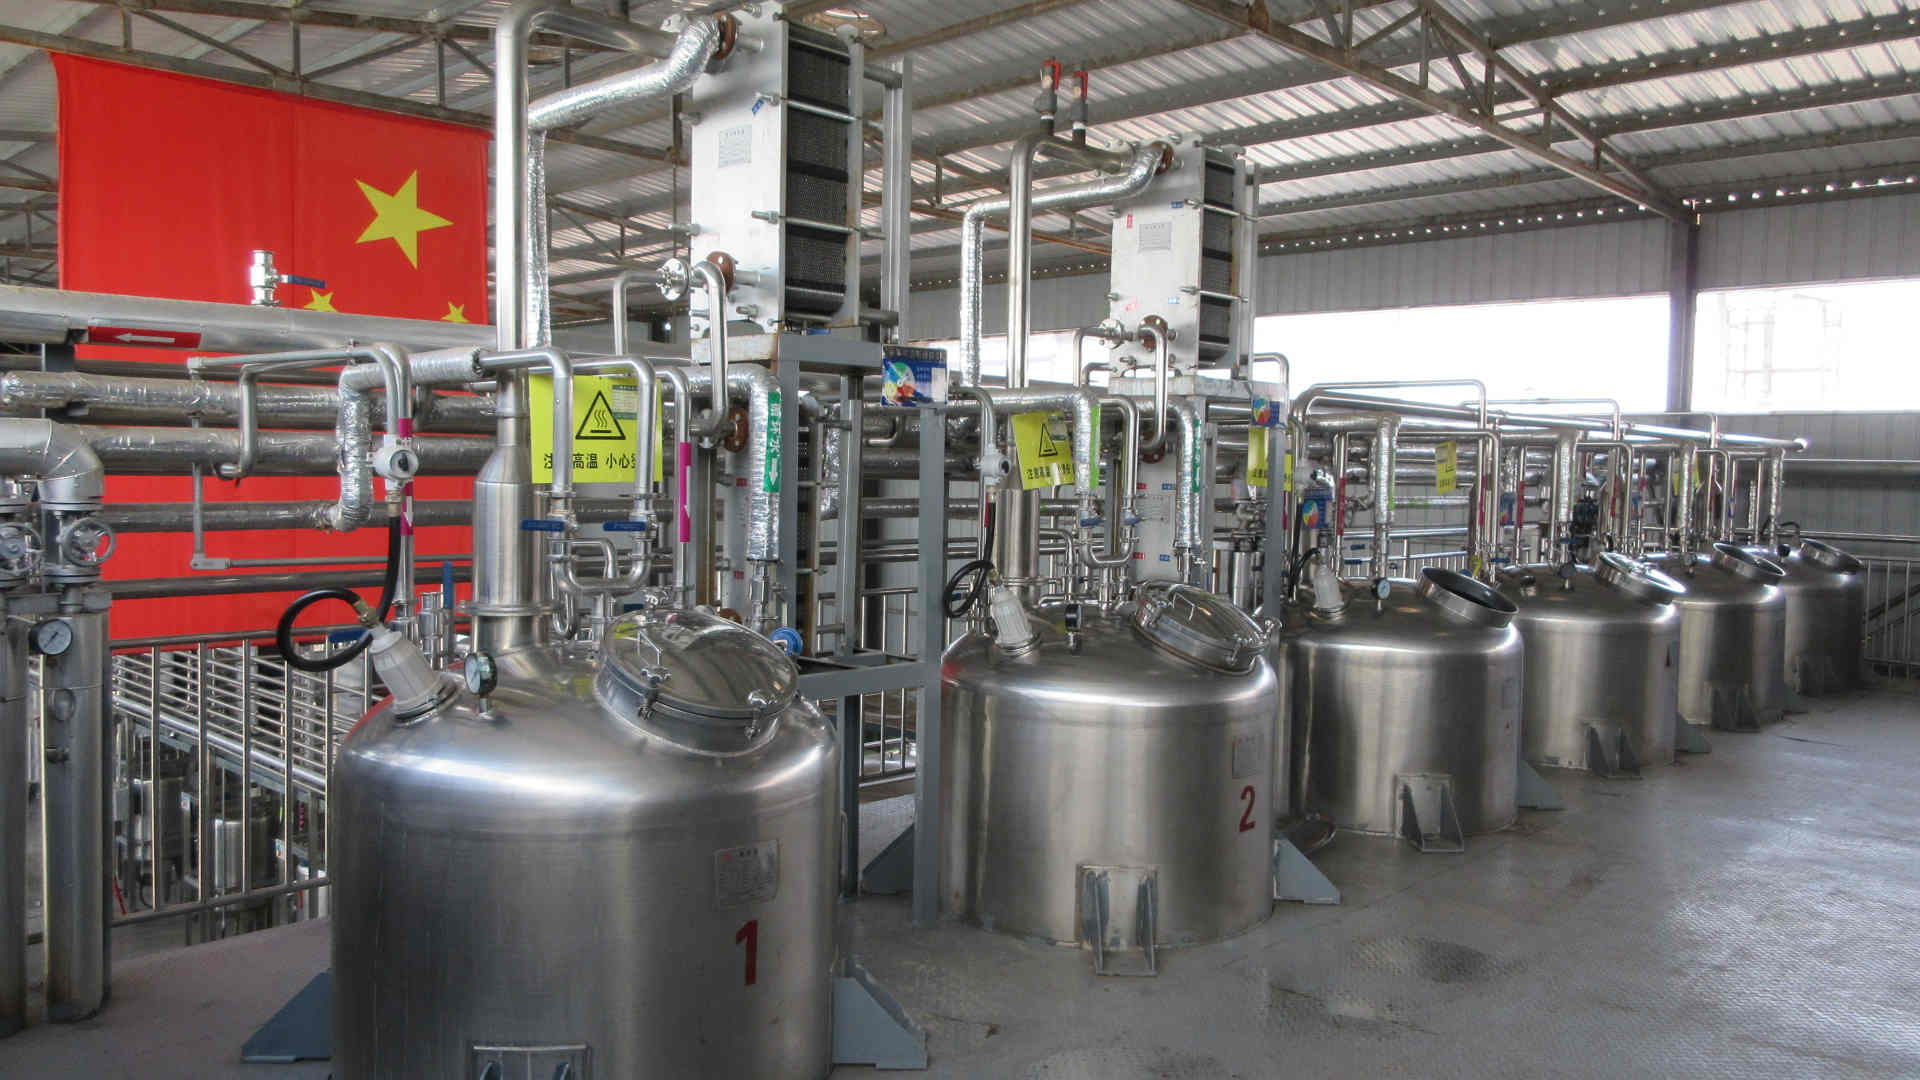
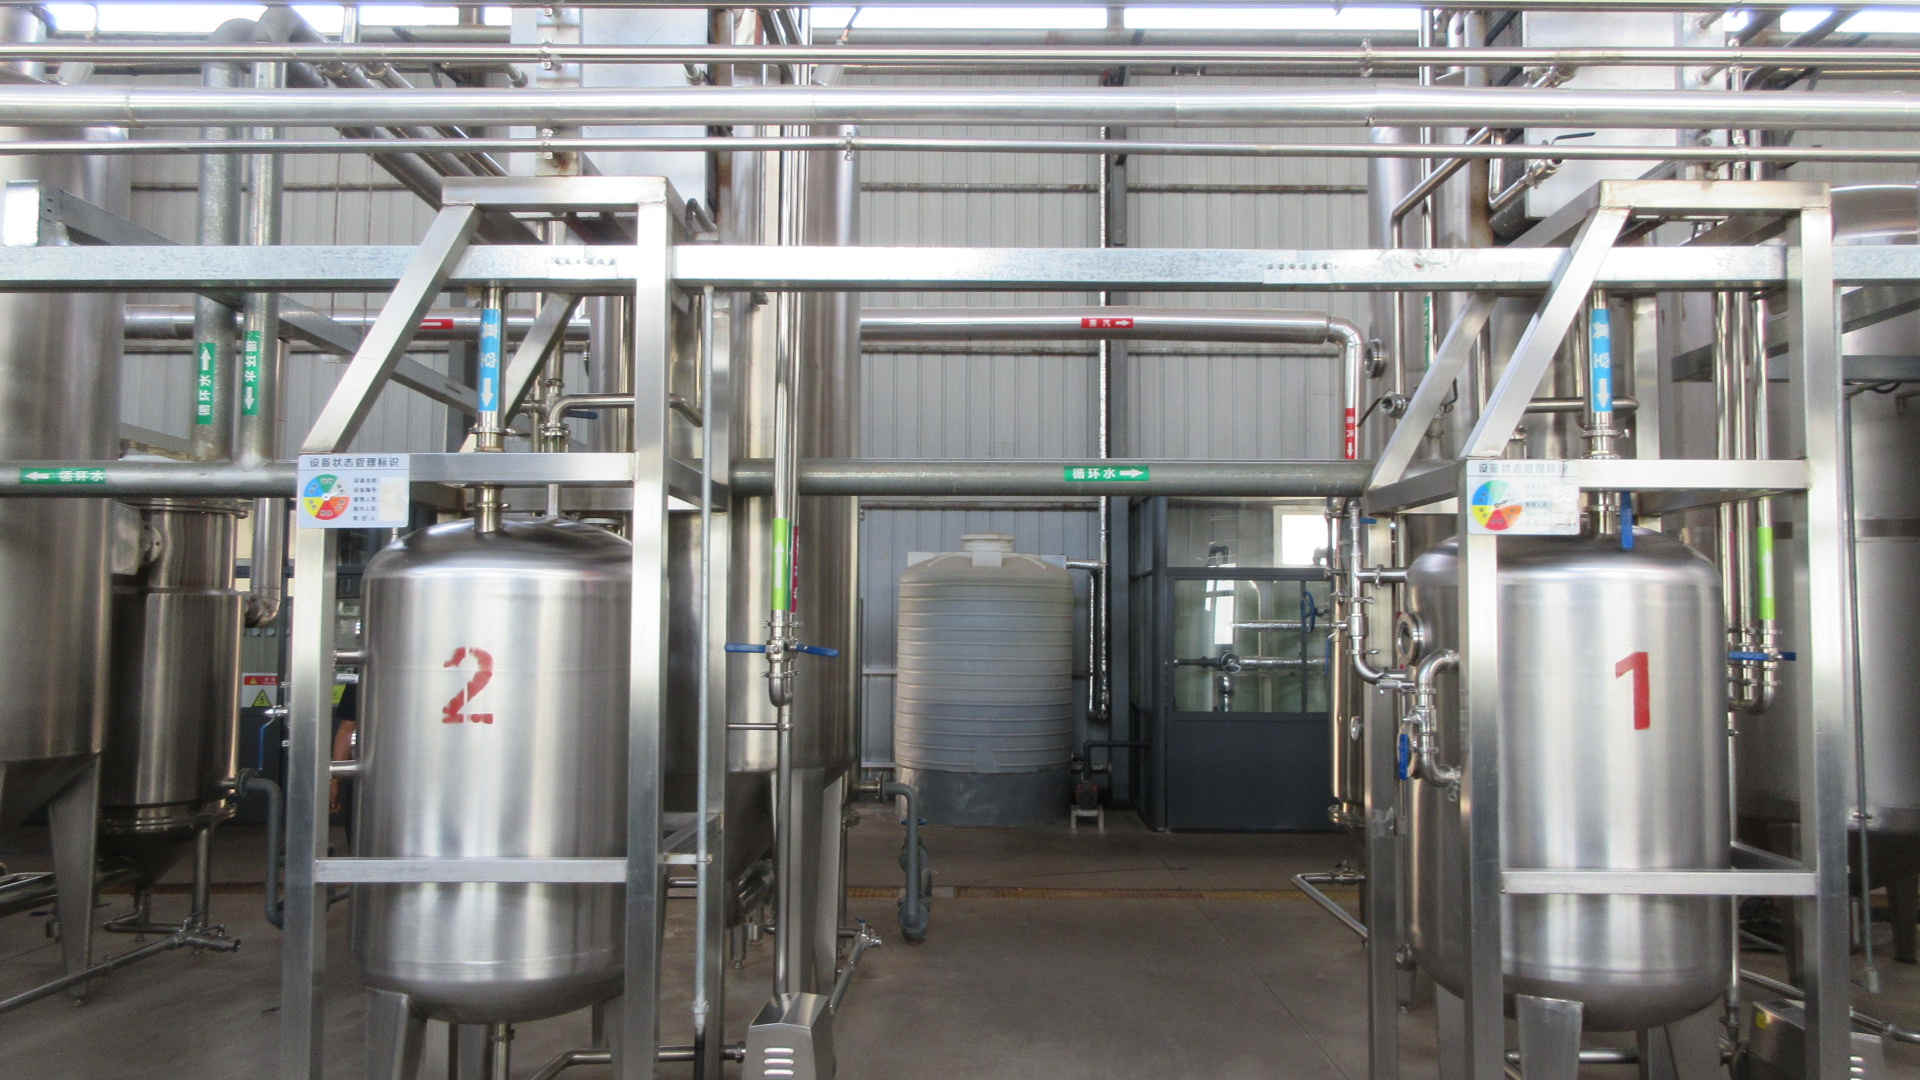
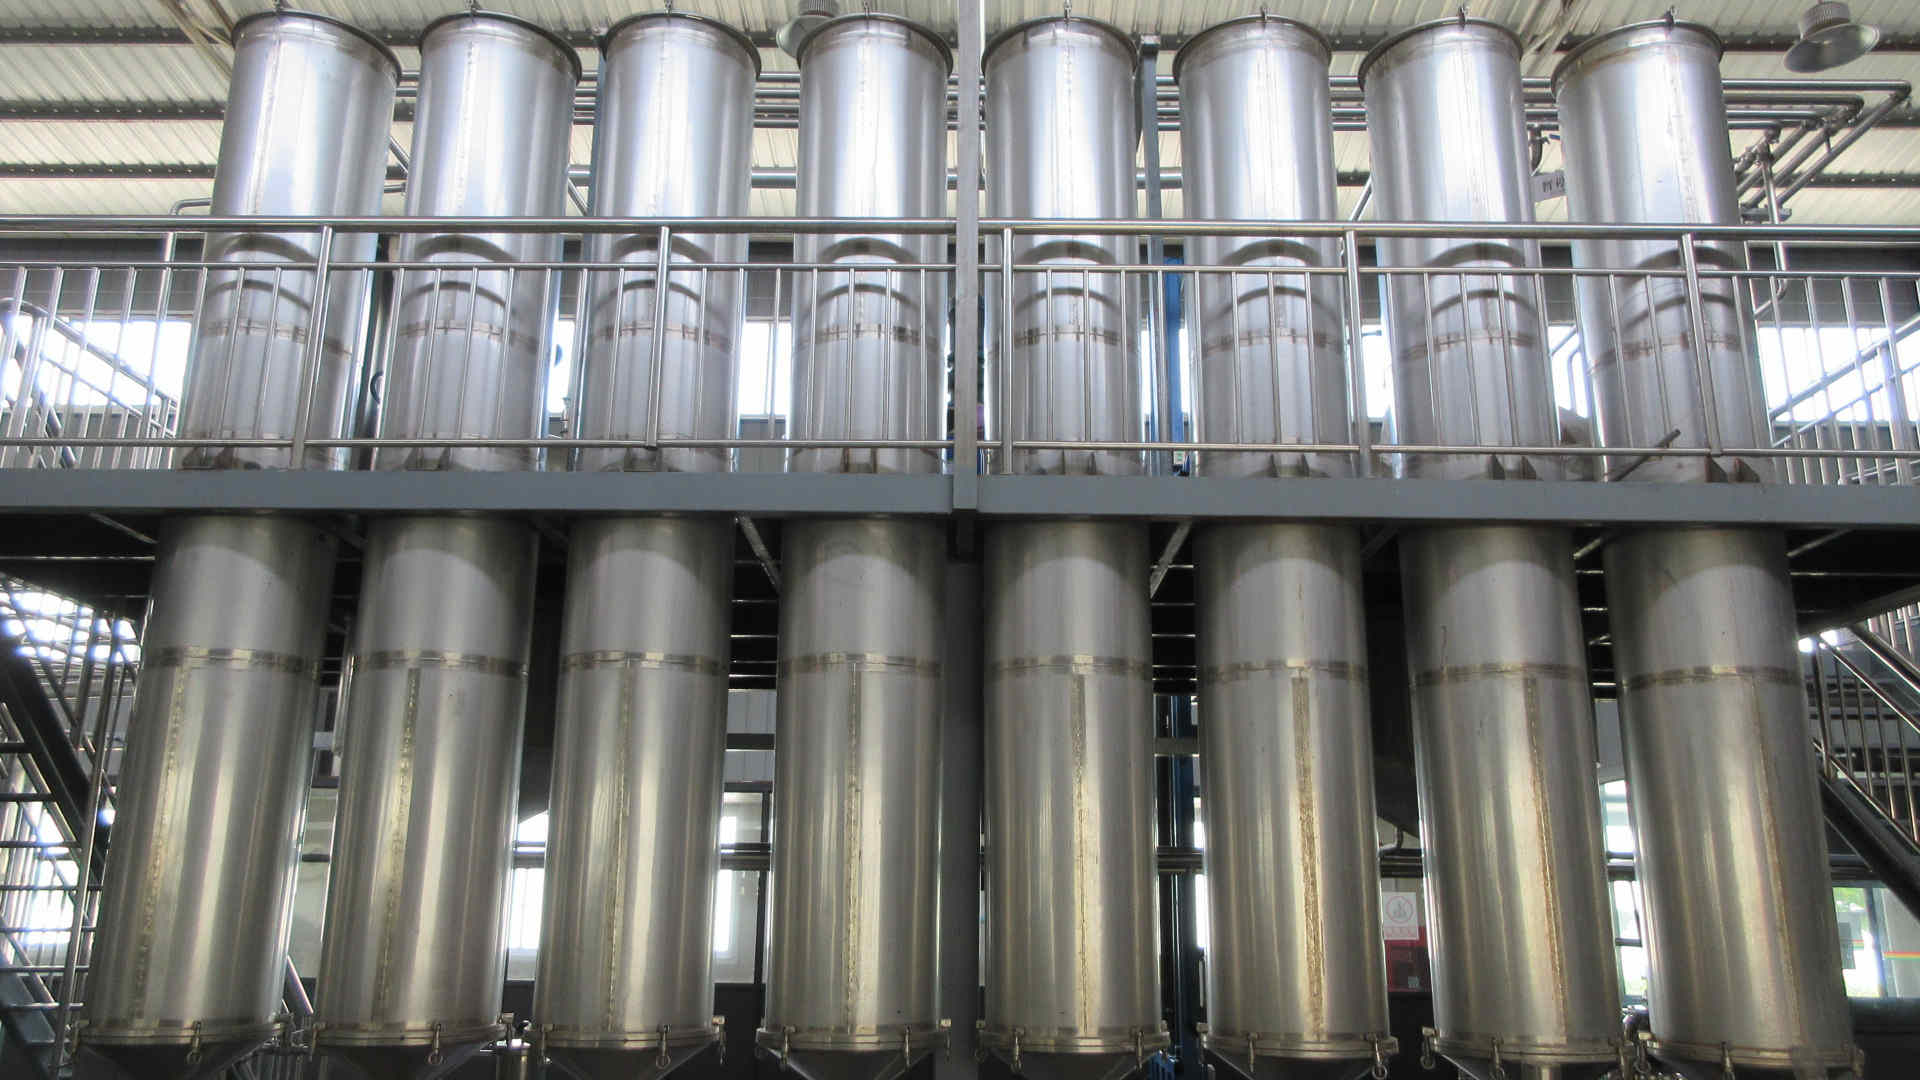
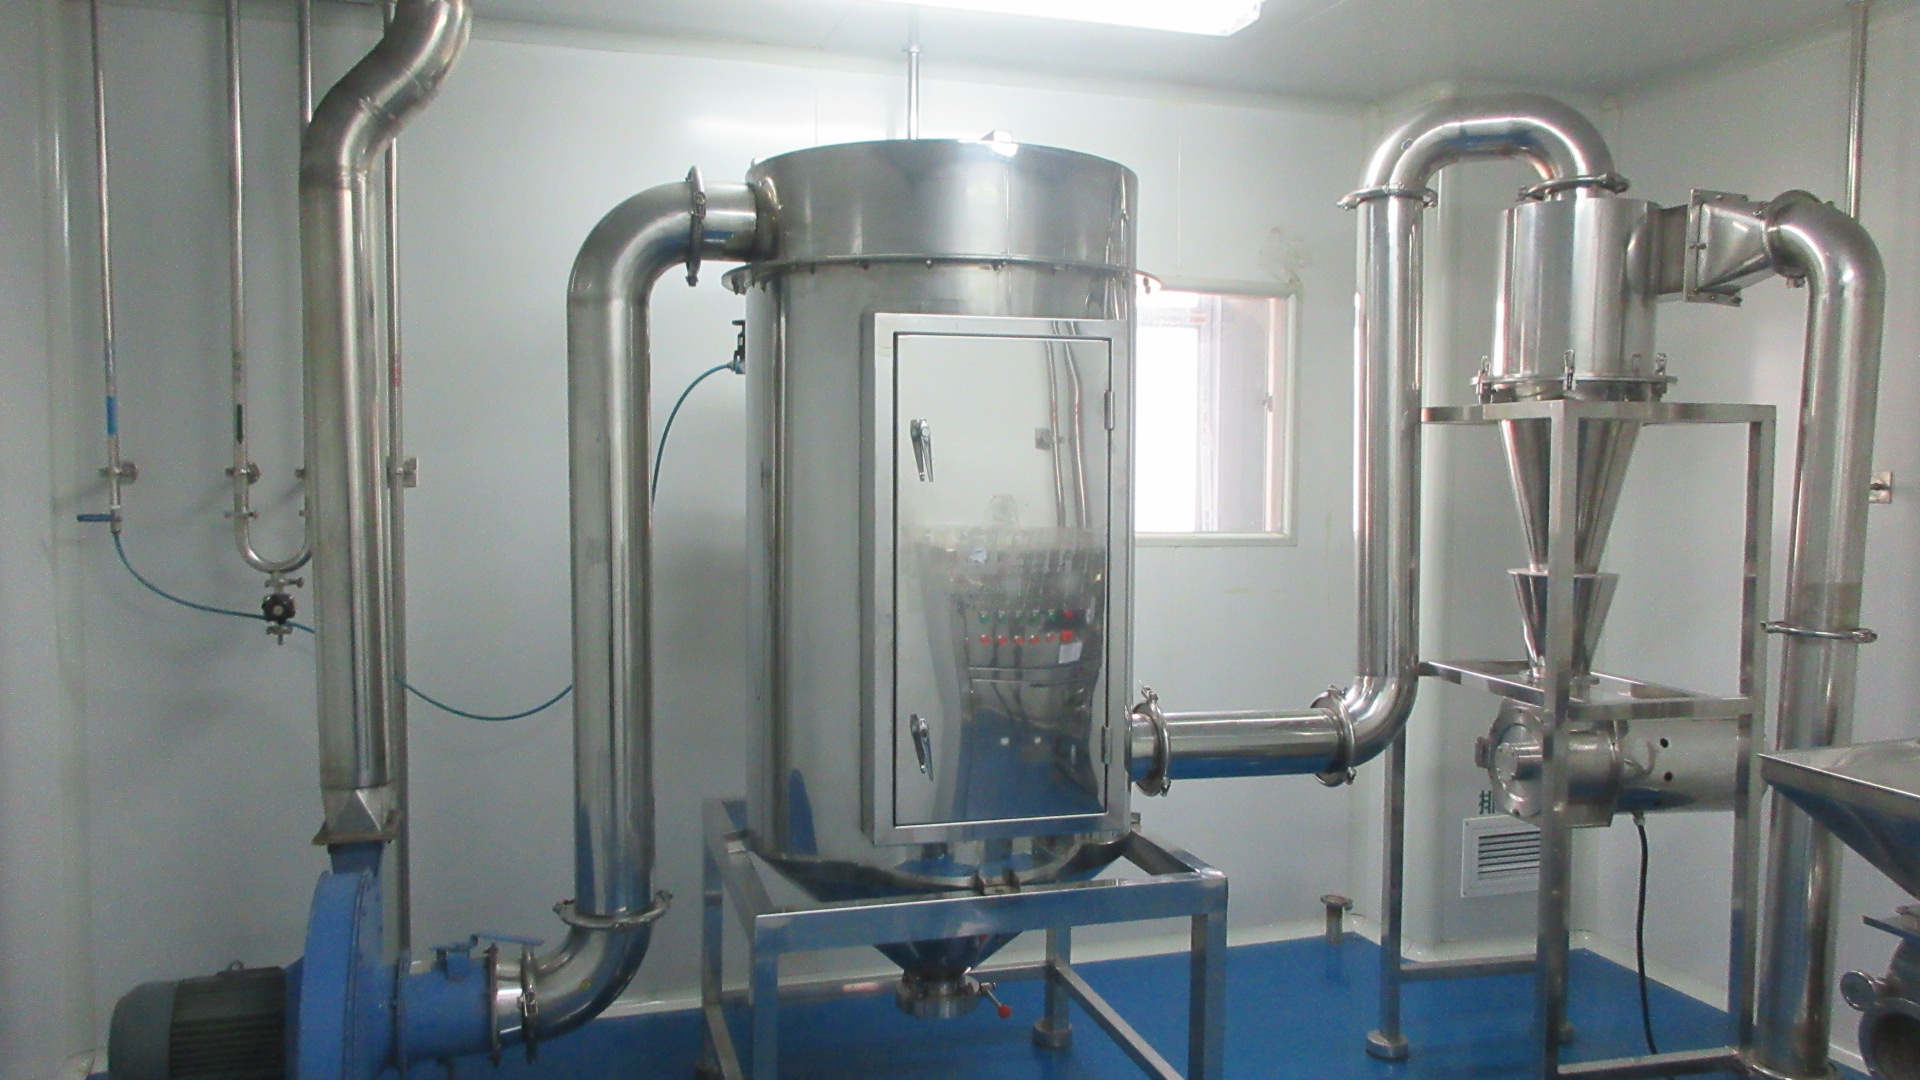
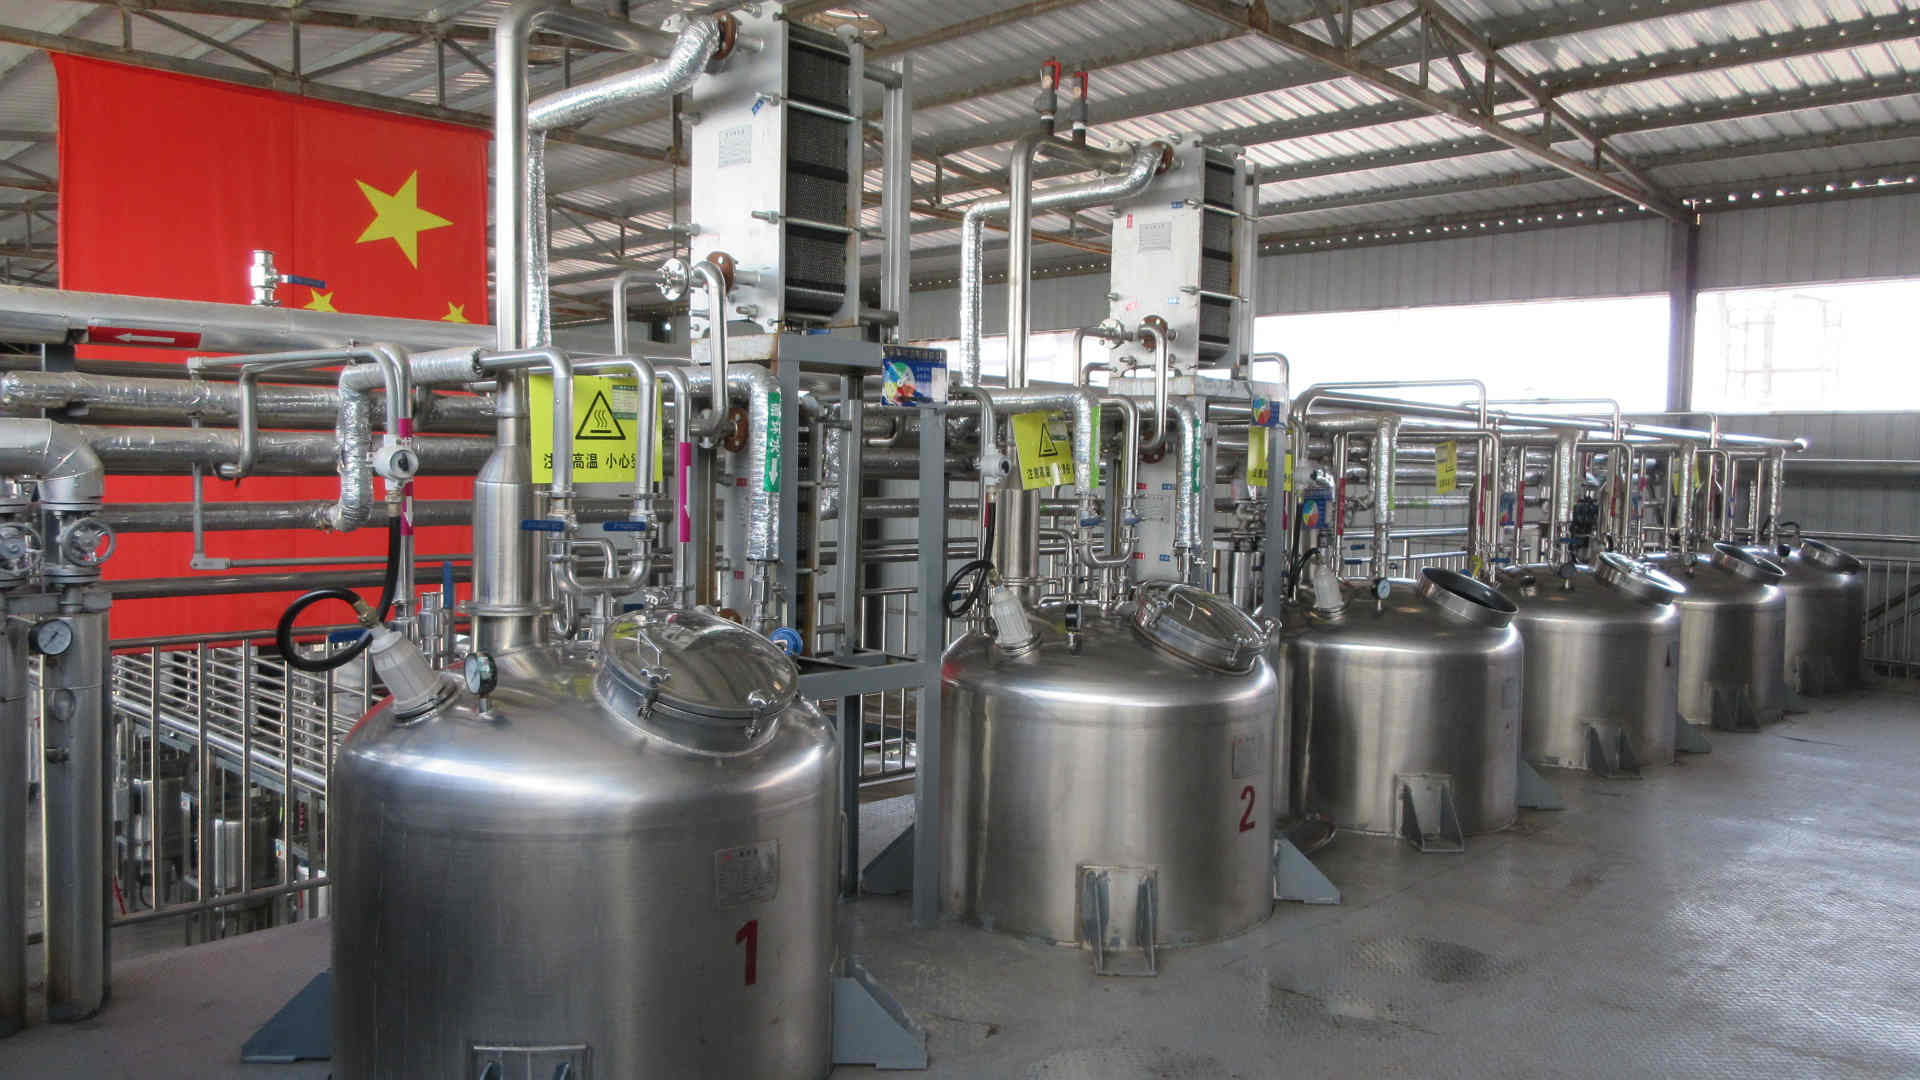
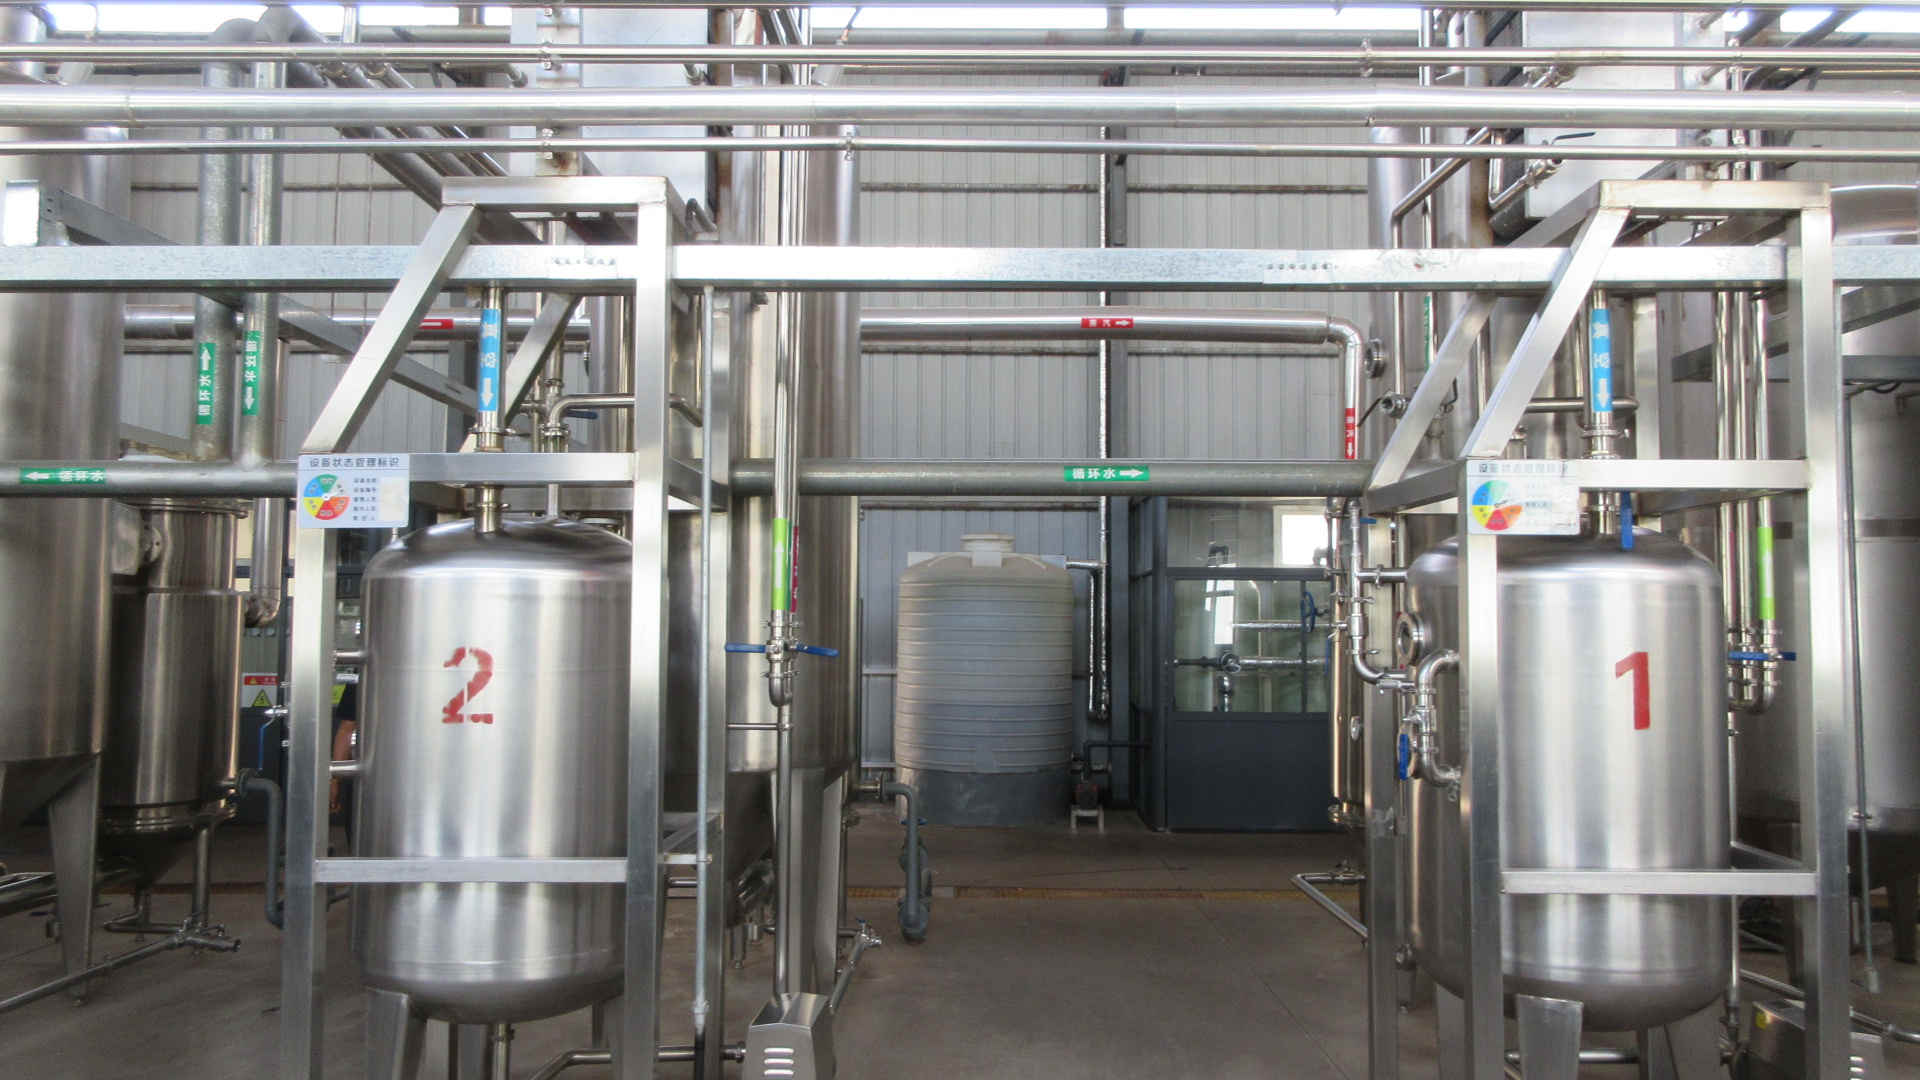
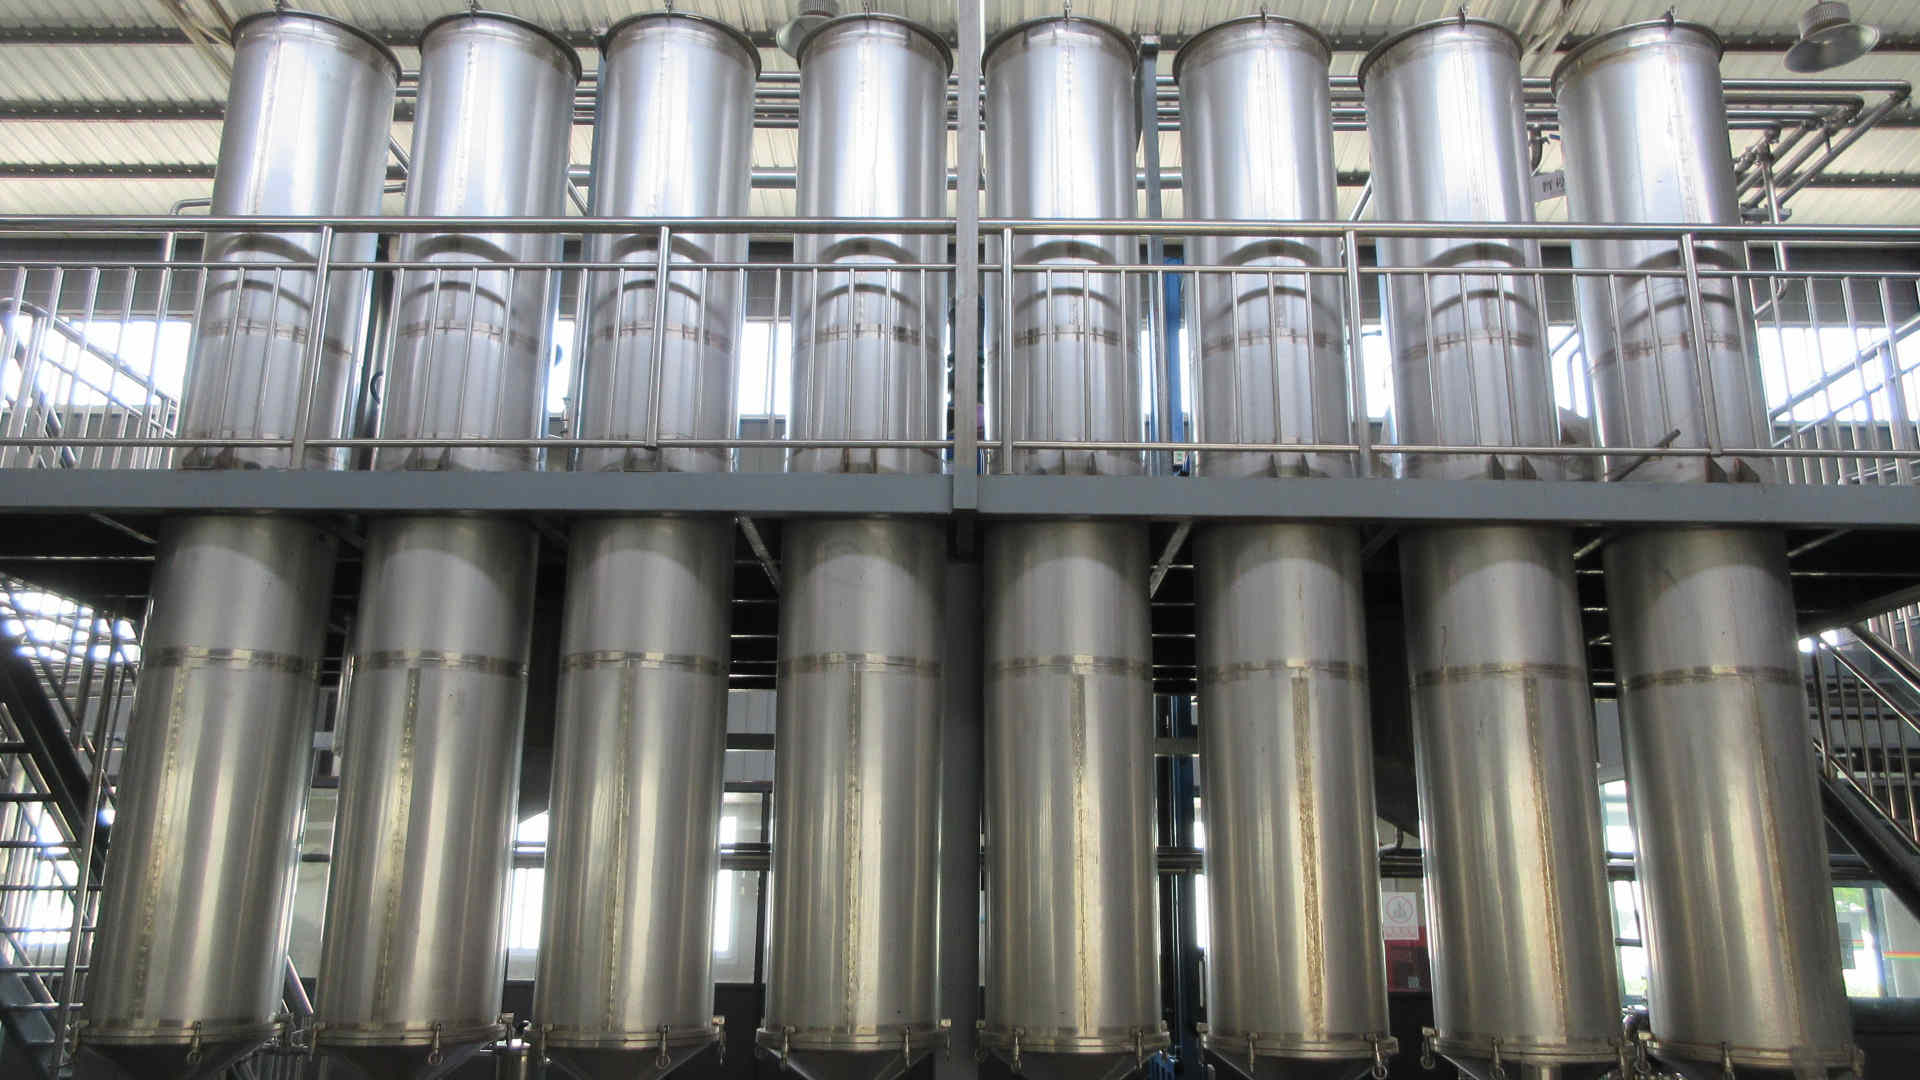
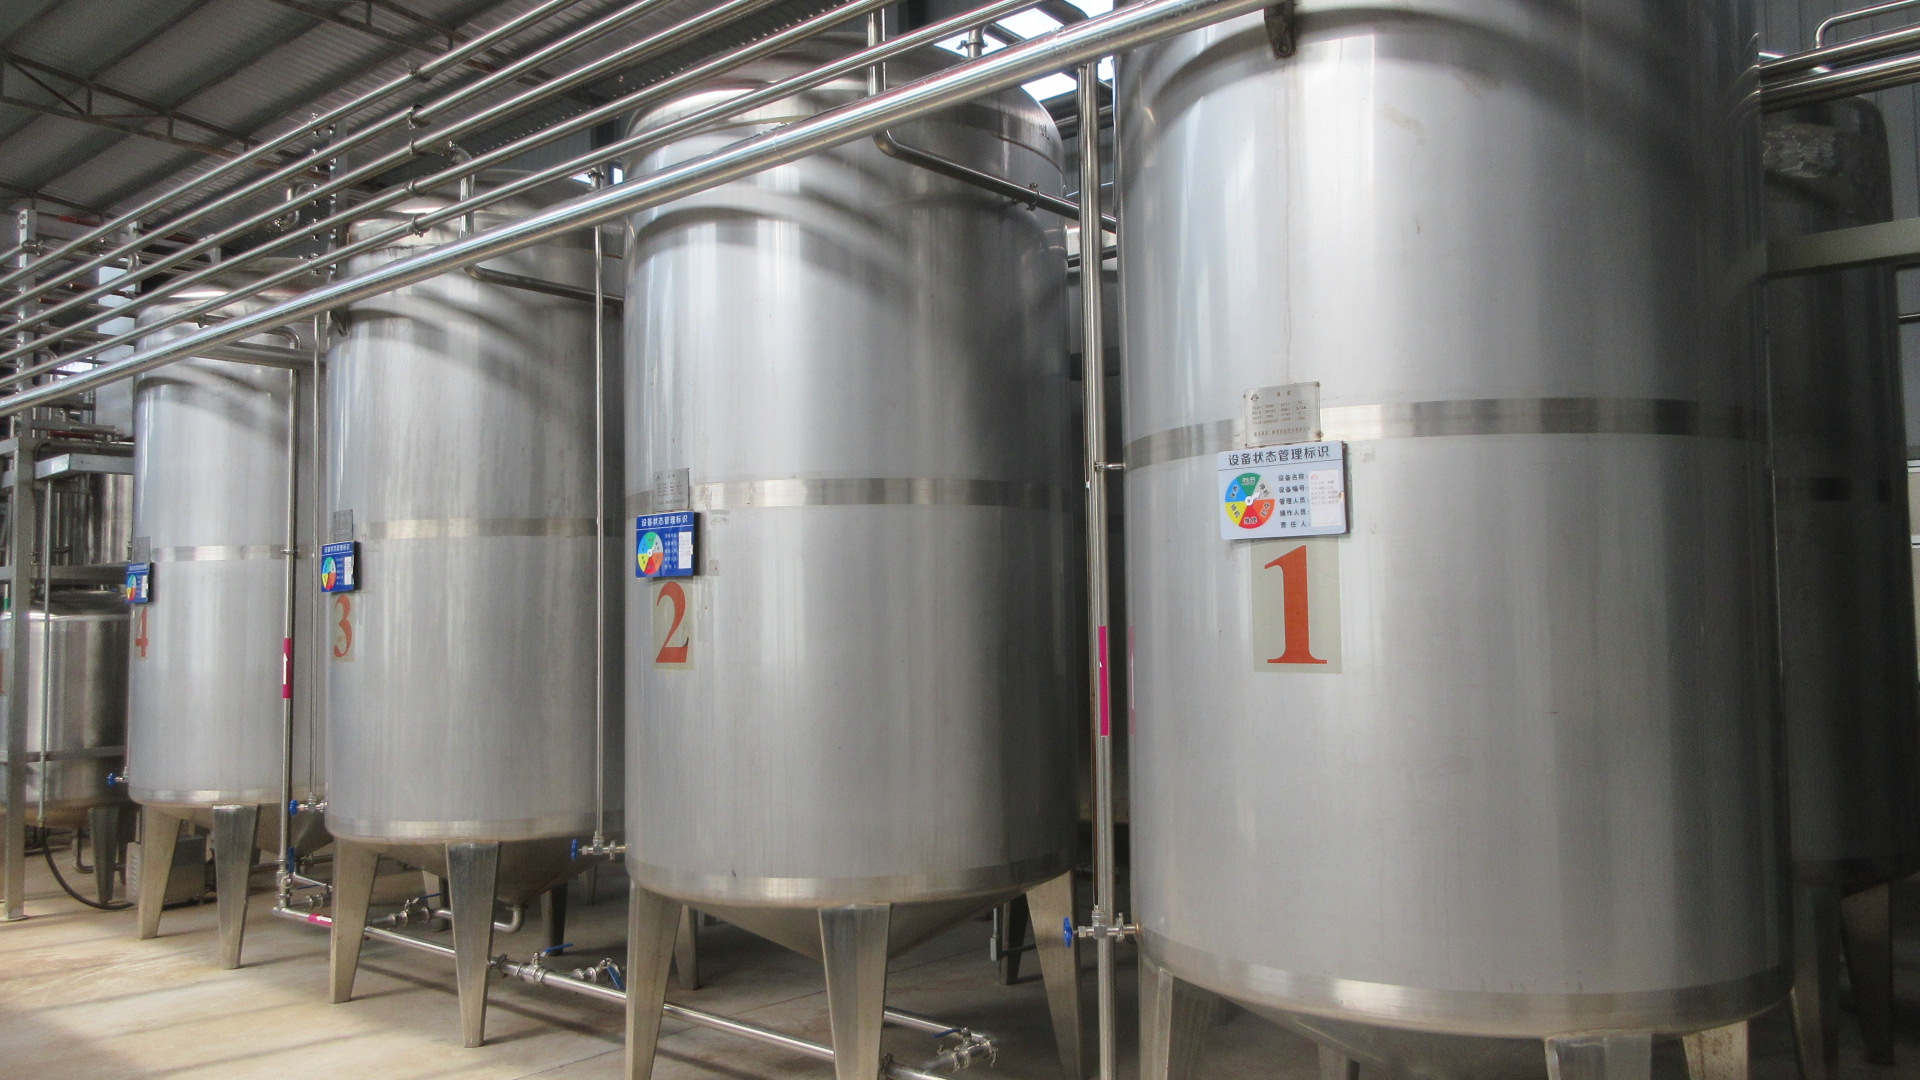
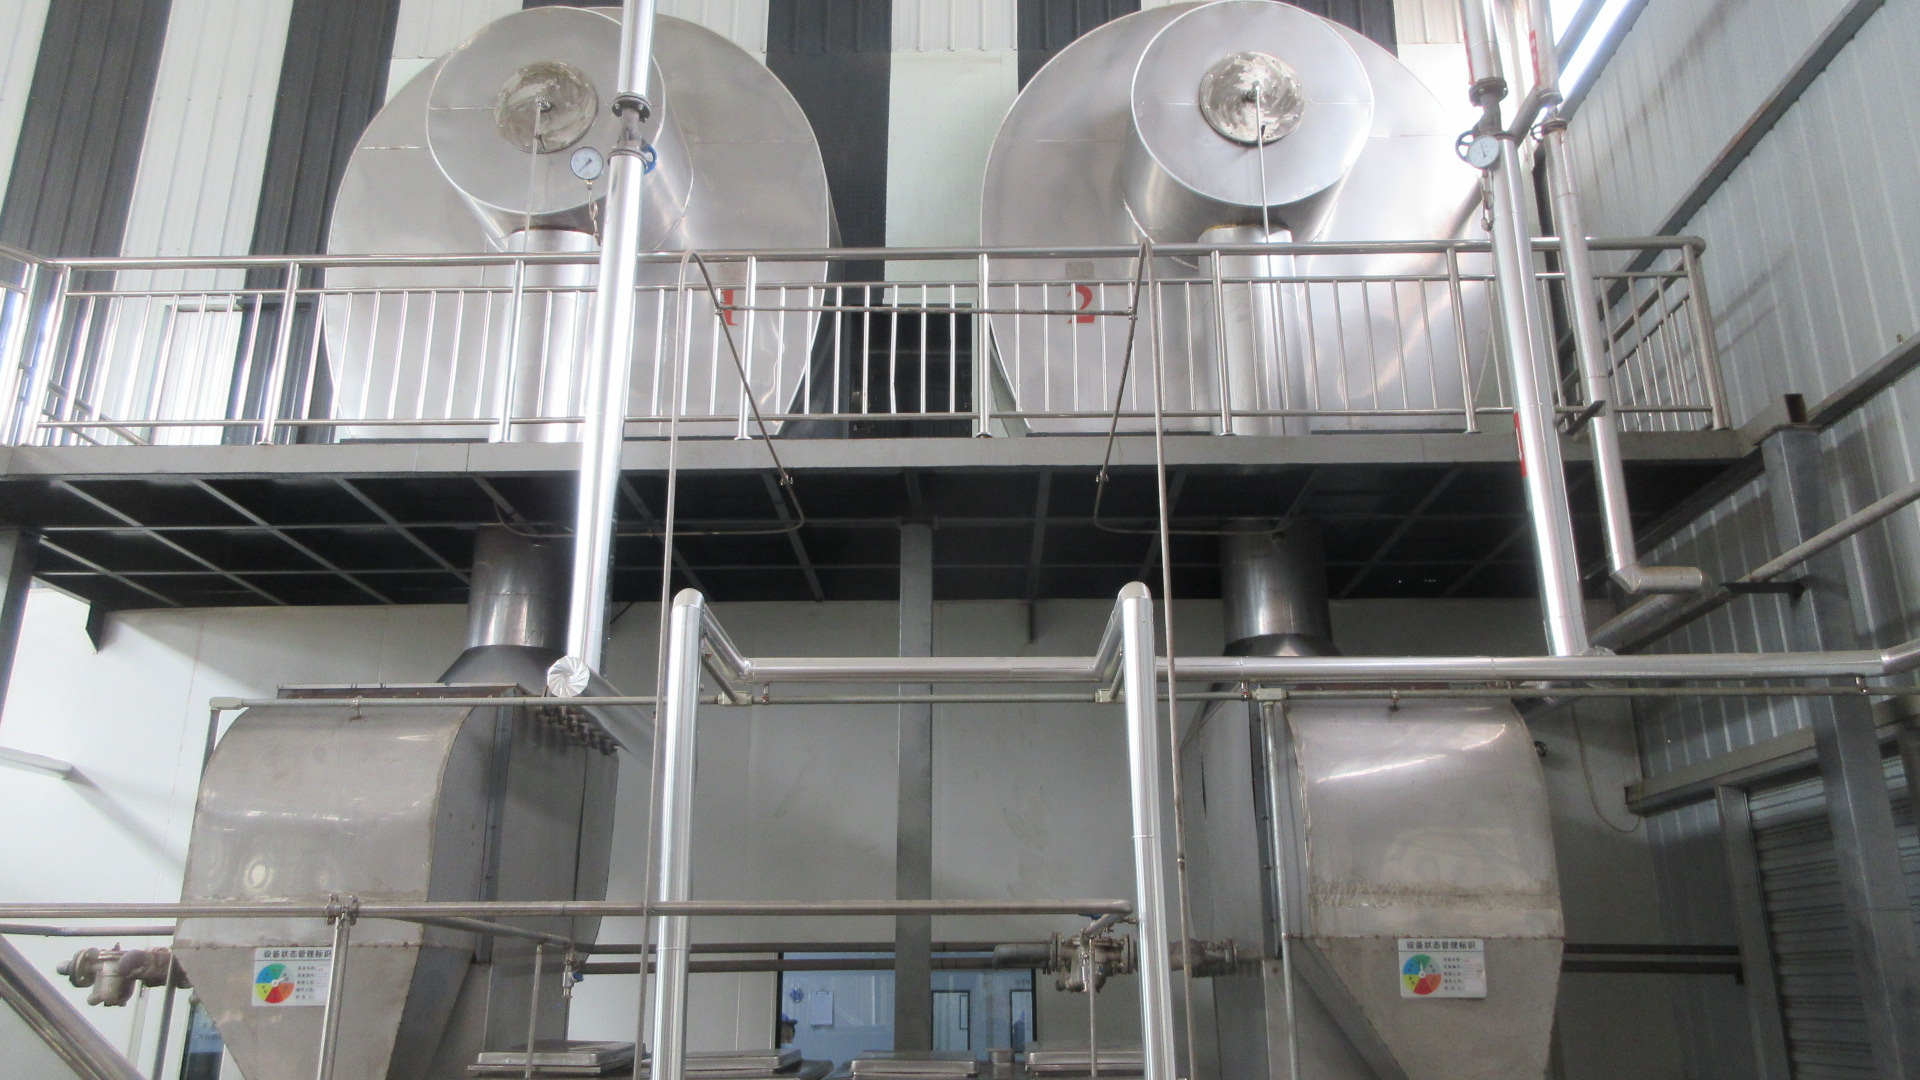
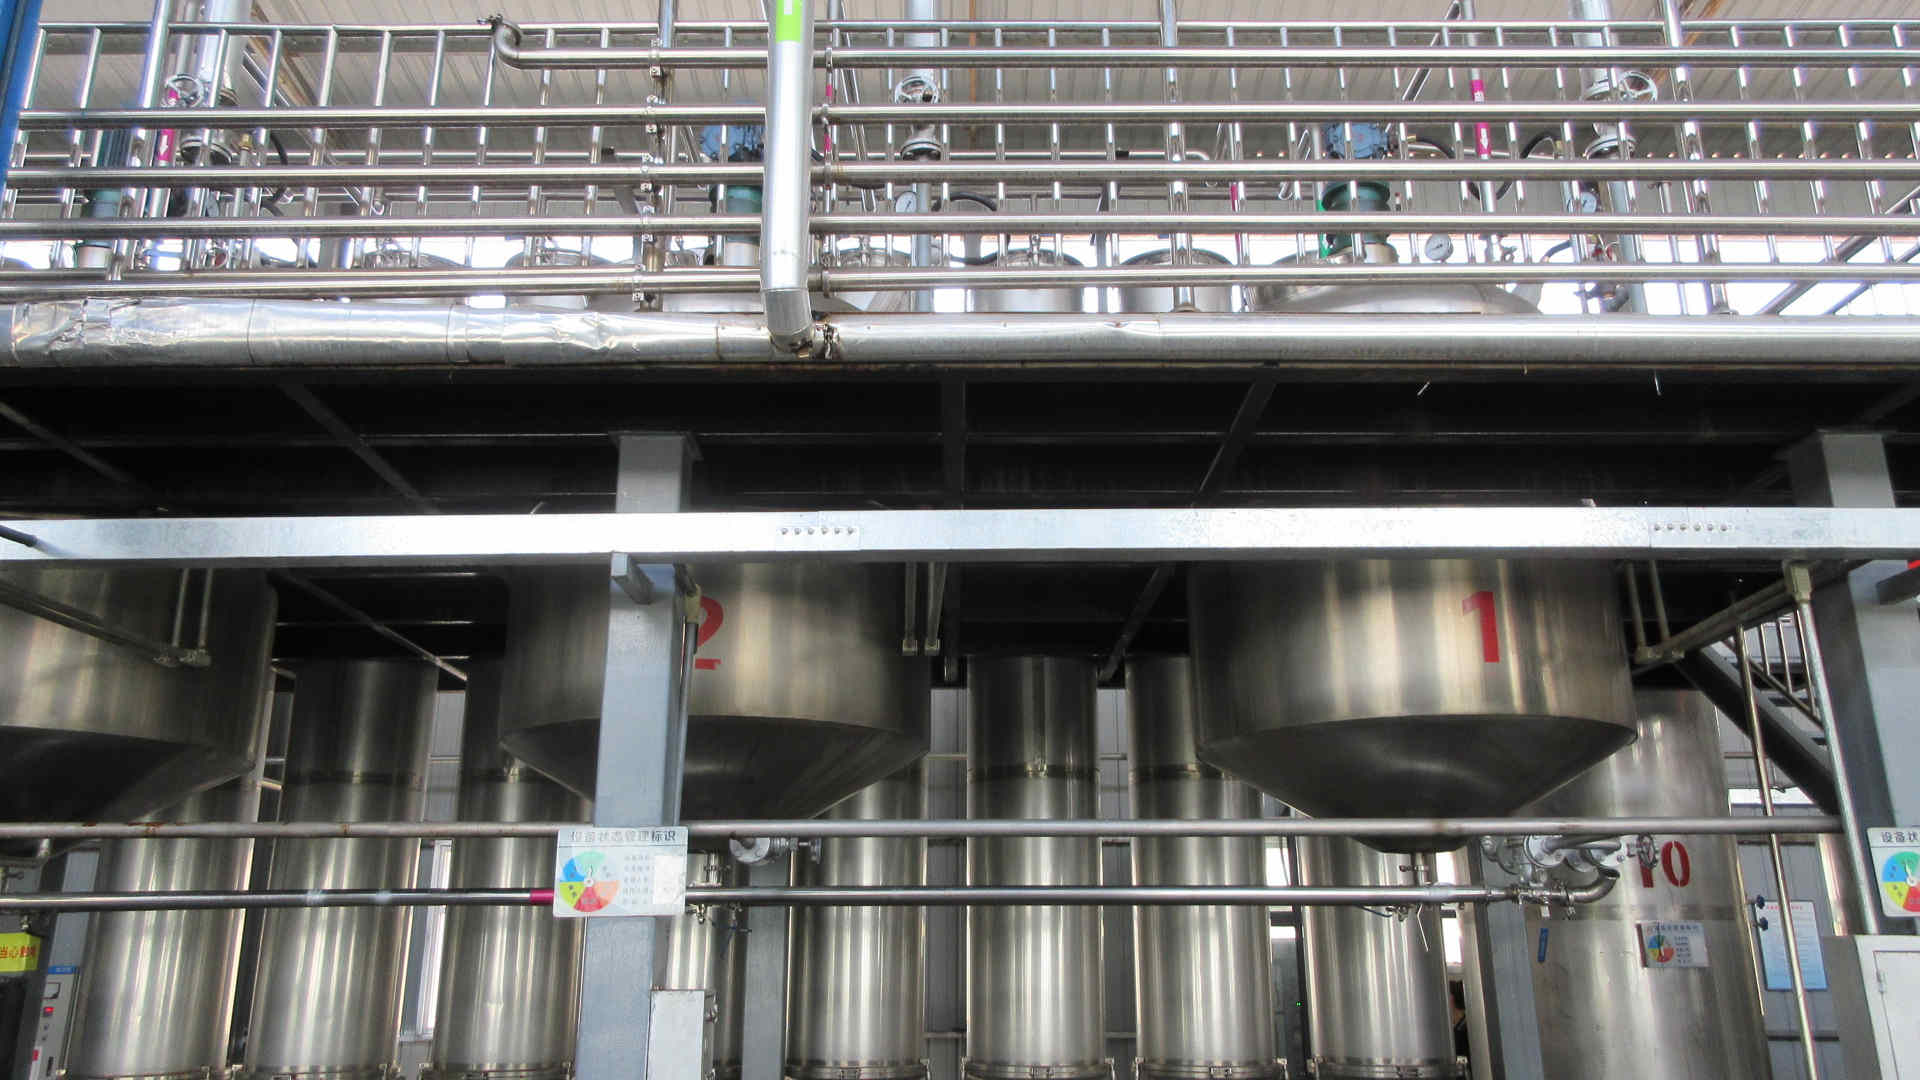
Cutting-edge extraction, low-temperature membrane concentration, chromatographic separation, and spray drying systems designed for high active retention.
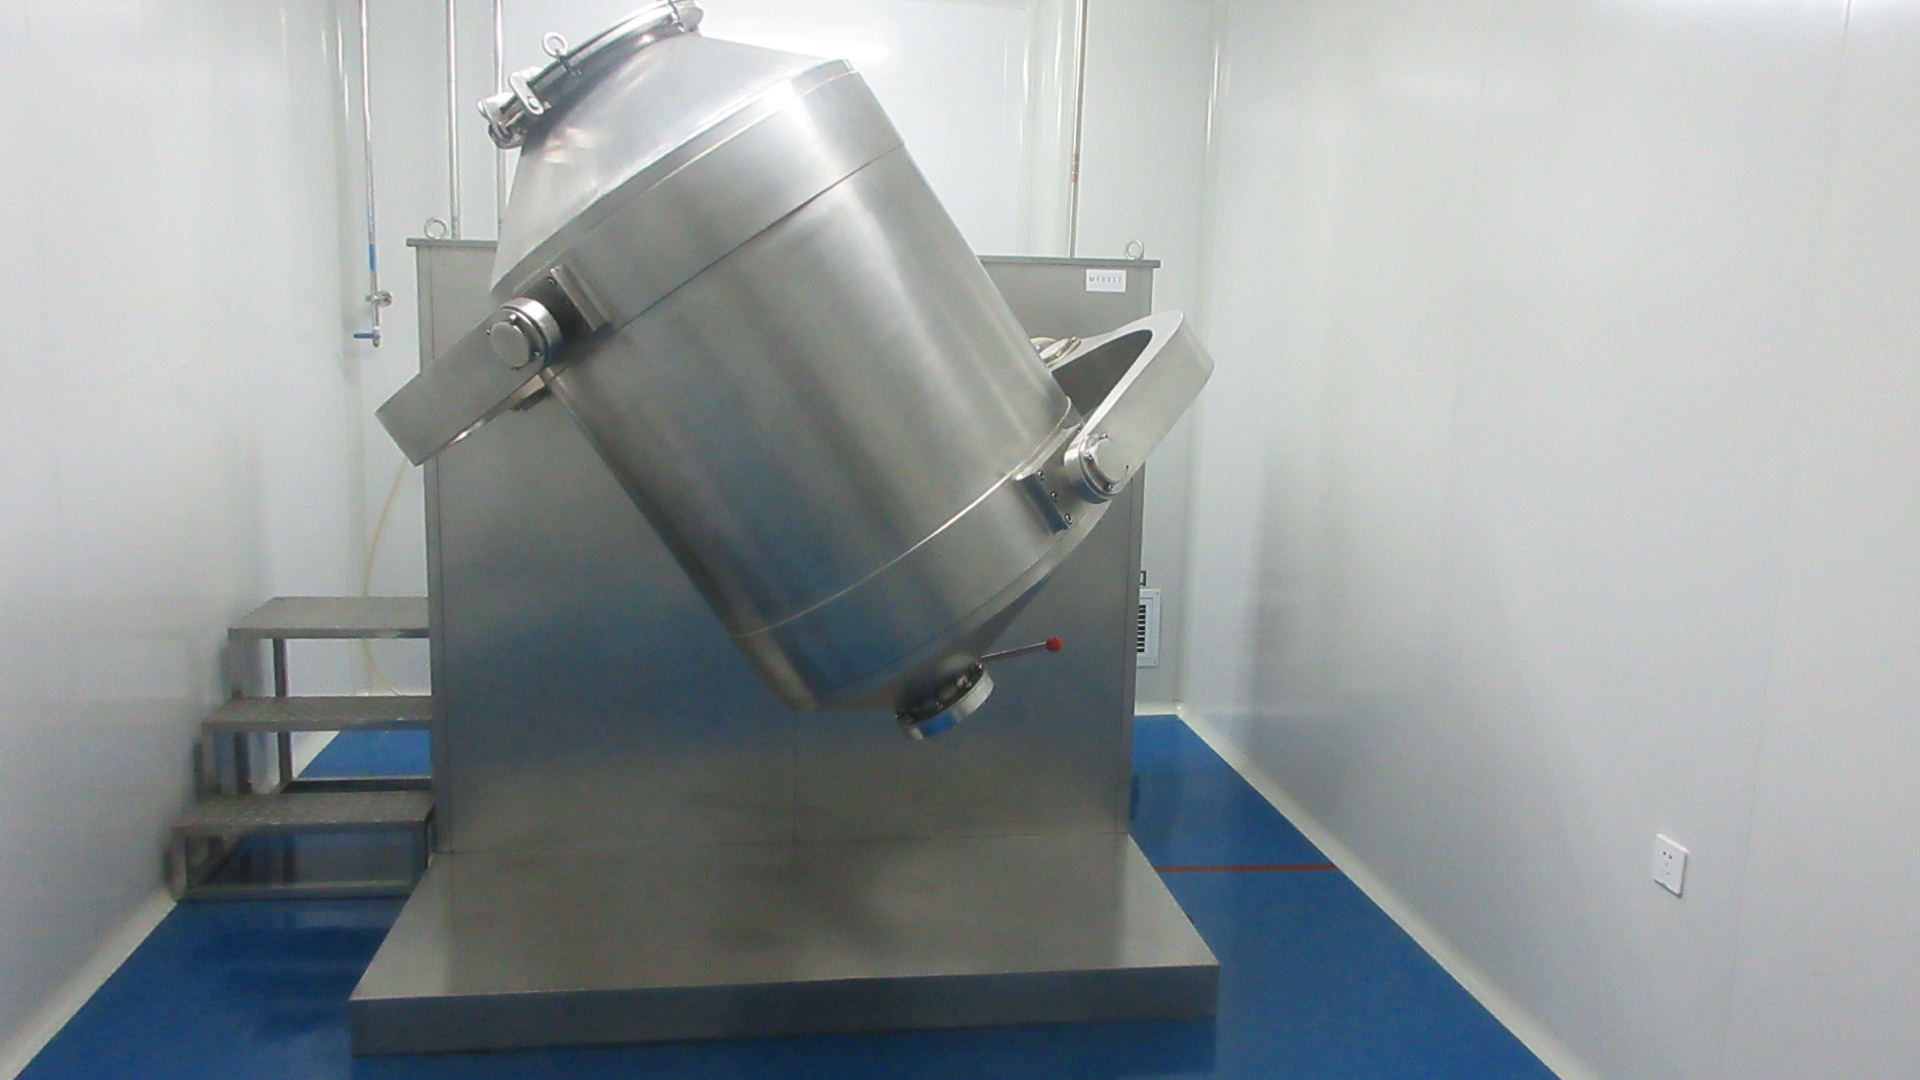
Comprehensive custom formulation, private labeling, particle mesh sizing, premixing, and specialized dosage encapsulation services tailored to market demand.
Direct factory manufacturing enables cost optimization, stable volume capacity, and long-term procurement price hedging for global distributors.
Global logistics integration supporting door-to-door, sea, air, and express shipping with dedicated technical assistance before and after sales.
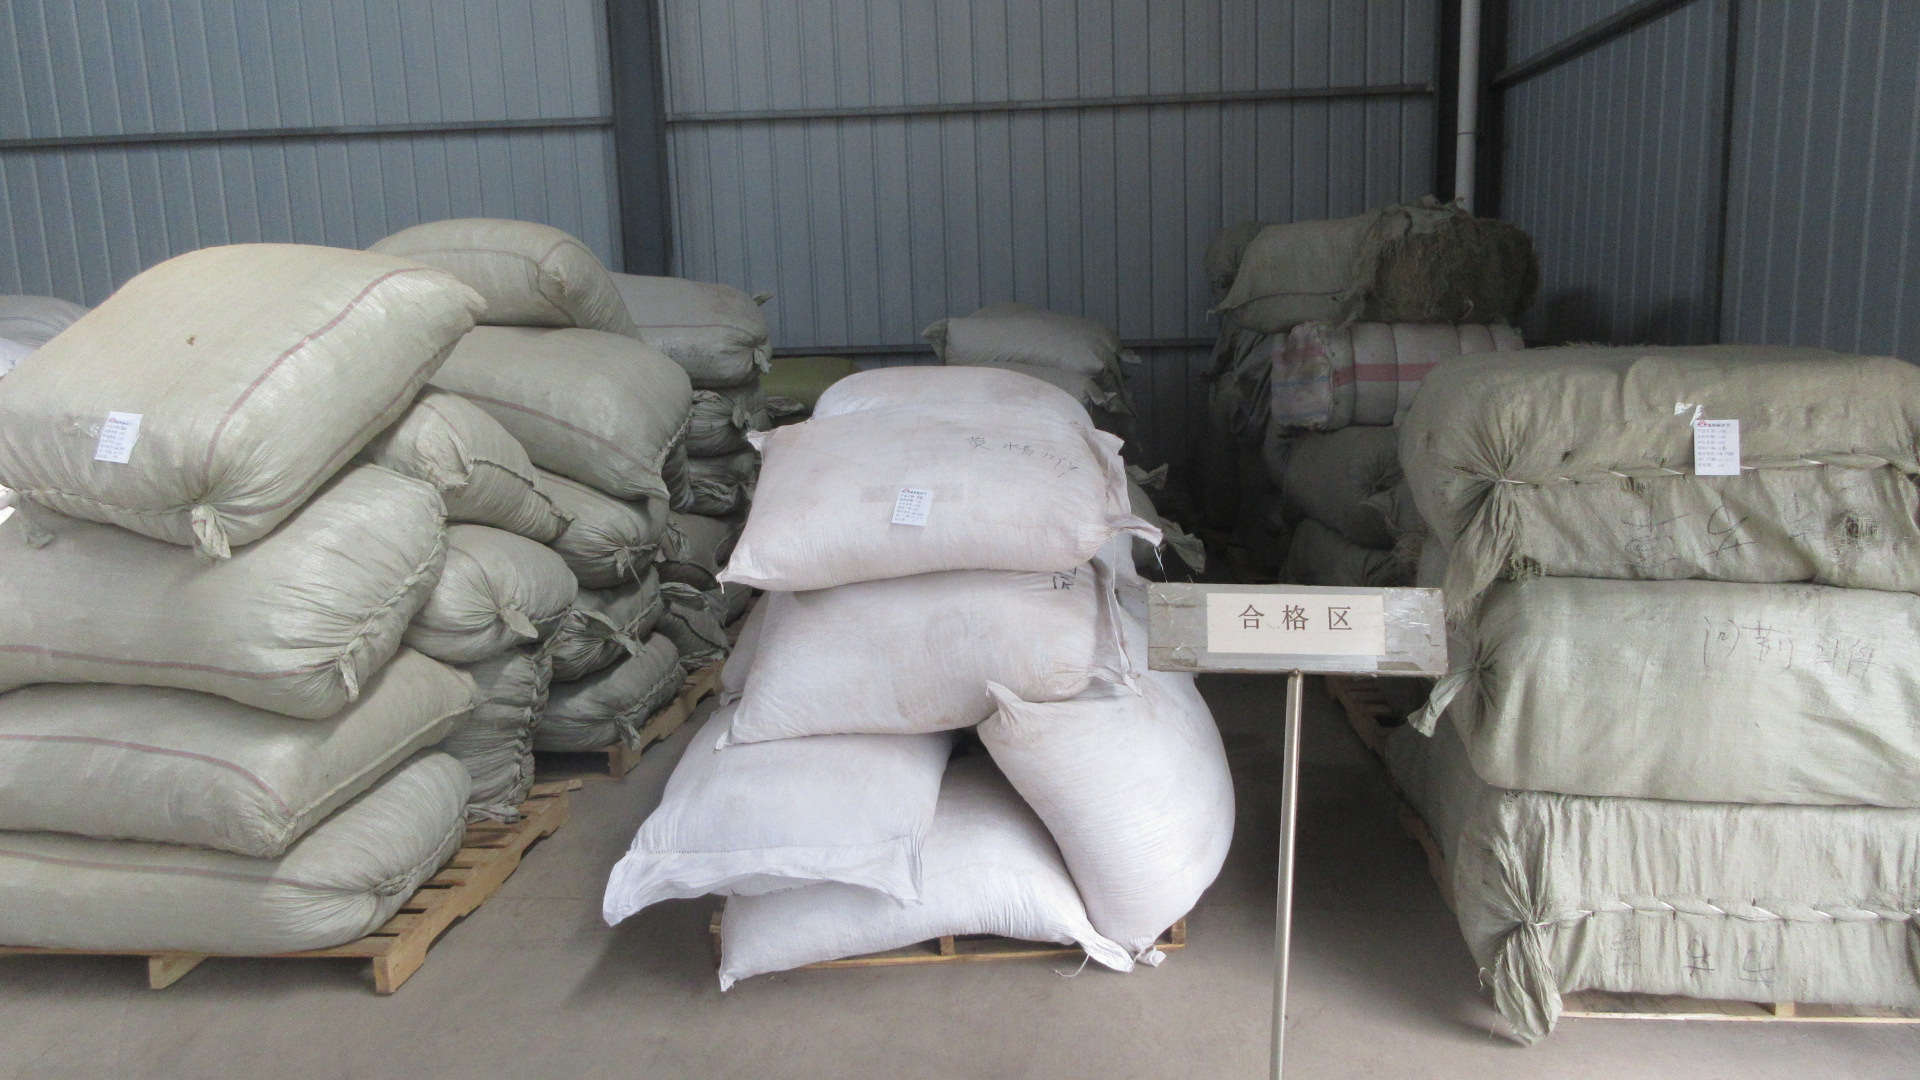
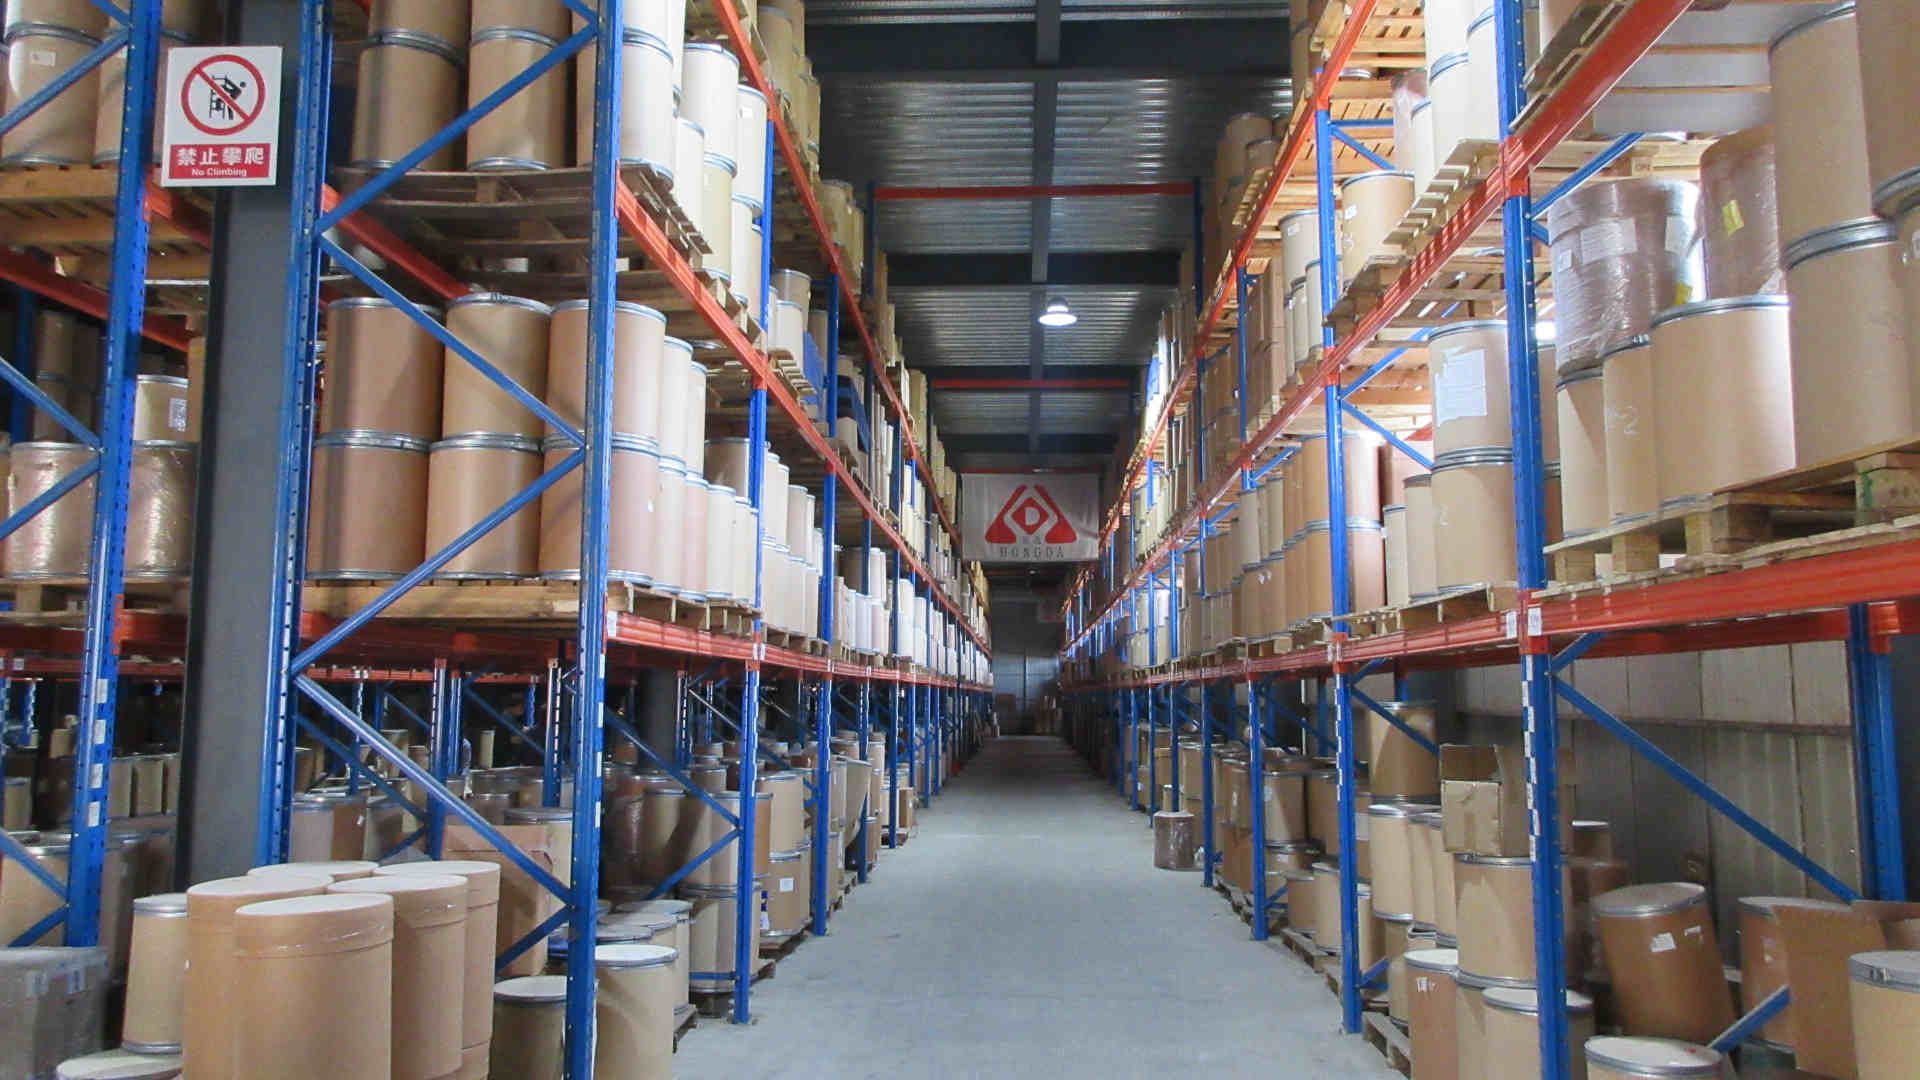
Complete end-to-end processing pipeline from botanical raw material intake to analytical quality control and high-speed packaging.
The industrial consumption of vitamins, specialized minerals, bioactive amino acids, and cosmetic barrier compounds is accelerating exponentially. Modern corporate procurement managers must navigate complex market drivers across distinct commercial sectors:
Global demand is shifting rapidly from standard single-vitamin tablets toward synergistic multi-ingredient matrix systems. Procurement demands focus on prebiotics, targeted amino acids, microencapsulated vitamin complexes, and digestive enzymes. Ingredients like high-solubility L-glutamine, probiotic fiber mixes, and organic amino acid powders enable manufacturers to develop premium stick packs, gummies, and clinical nutrition formulas with high stability and pleasant organoleptic profiles.
The cosmetic market is governed by biomimetic actives. Ingredients such as multi-ceramide complexes (SK-INFLUX V MB), high-purity hexapeptides (Hexapeptide-2), and enzymatic oxido-reductases are critical for anti-aging, lipid barrier repair, and hyperpigmentation suppression. Formulators require raw materials with standardized CAS purity, low endotoxins, and certified sustainable palm kernel derivatization (RSPO / MB standards).
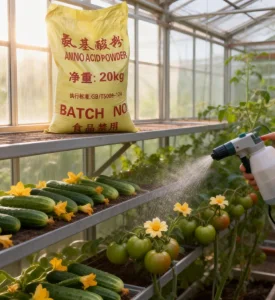
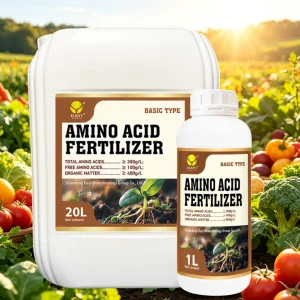
Sustainable agriculture demands zero-residue, highly bio-available plant biostimulants. Plant-derived organic amino acid powders (40% free L-amino acids) produced via controlled enzymatic hydrolysis enhance osmotic stress tolerance, stimulate root rhizosphere activity, and dramatically boost mineral uptake efficiency in broadacre crops, horticulture, and commercial greenhouses.
Food security and chemical stability rely on specialized antioxidant stabilizers. Compounds like Butylated Hydroxyanisole (BHA) and specialized non-corrosive industrial antioxidants (e.g., Benzotriazole BTA) protect organic lipids, synthetic polymers, and machinery fluids against auto-oxidation, extend thermal stability, and prevent catalytic degradation.
As the global biotechnology landscape advances, Shaanxi Mirae Biology Co., Ltd. is committed to pioneering next-generation manufacturing technology routes:
Ensuring seamless international customs clearance, full audit documentation, and localized supply security.
Every shipment is accompanied by detailed Certificate of Analysis (CoA), Heavy Metal Analysis (ICP-MS), Pesticide Residue Screening, HPLC Chromatograms, and MSDS/SDS documentation.
Manufacturing facilities operate under ISO9001:2015, ISO22000, cGMP, and HACCP frameworks, with Kosher and Halal compliance available across primary product lines.
Flexible bulk packaging solutions ranging from 1kg aluminum foil bags for high-value peptides to 25kg fiber drums and 1,000kg tote tanks, supported by temperature-controlled cold chain logistics.
Expert insights covering product specs, minimum order quantities, testing procedures, and global delivery schedules.
Our standard production runs accommodate MOQs starting as low as 1kg for high-purity peptides and cosmetic active compounds (such as D-Serine or Hexapeptide-2), and 100kg to 1,000kg for bulk botanical powders, amino acid biostimulants, and food-grade additives.
We utilize an automated 8-step process pipeline, including high-vacuum falling-film evaporation, precision chromatographic adsorption columns, and automated spray towers. Every production lot undergoes internal HPLC/GC testing plus third-party validation (SGS/Eurofins upon request).
Yes. Our crushing, sieving, and fluid-bed granulation equipment allows us to engineer customized mesh profiles ranging from ultra-fine 200-mesh powders to dust-free granular forms designed for tableting and hard-shell encapsulation.
Absolutly. We prioritize sustainable feedstock sourcing. Our cosmetic barrier ceramides and botanical extract lines comply with RSPO Mass Balance standards, cruelty-free guidelines, and EU Cosmetic Regulation (EC) No 1223/2009 requirements.
Standard catalog items ship within 3–5 business days from our Shaanxi warehouse. Custom OEM/ODM formulation runs typically require 2 to 3 weeks for synthesis, spray drying, quality verification, and export documentation preparation.
Our dedicated R&D team composed of senior bio-engineers offers comprehensive technical guidance regarding active compound stability, pH compatibility, solubilization strategies, and antioxidant protection matrix selection.
Explore our extended line of active pharmaceutical intermediates, specialty food antioxidants, and high-efficiency biostimulants.
 Mirae Biology